For industrial applications involving sodium silicate, the choice of an efficient and reliable material handling solution is critical. The sodium silicate pneumatic conveying system represents a sophisticated approach to transporting this chemical, offering numerous advantages over traditional methods. This analysis delves into the design, functionality, and benefits of such systems, highlighting their role in modern industrial processes.
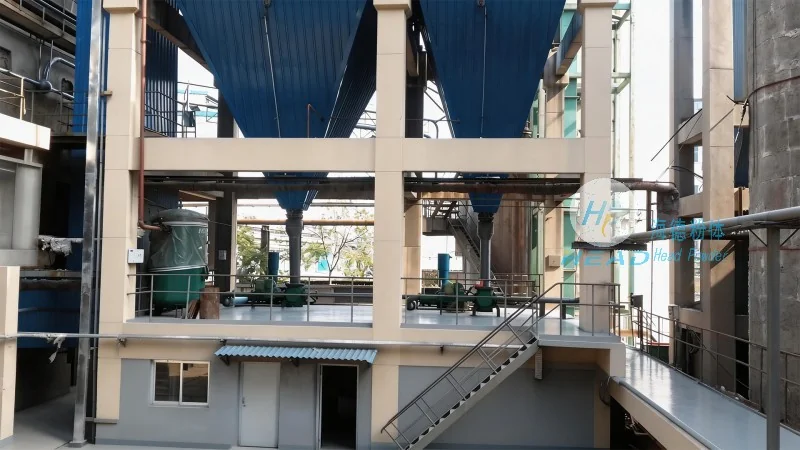
The sodium silicate pneumatic conveying system is a technology designed to transport sodium silicate, a key industrial chemical, through a pressurized air stream. Unlike conventional methods like belt conveyors or bucket elevators, this system uses air to move the material, minimizing physical contact and reducing the risk of contamination or degradation. The system typically consists of a hopper, a rotary airlock, a conveying line, and a receiver, all working in tandem to ensure smooth and continuous material transfer.
Headpowder, a leading manufacturer in the field, specializes in the design and production of advanced pneumatic conveying systems. With a strong presence in China, particularly in Shandong, the company has built a reputation for quality and innovation. Shandong HeadPowder Engineering Co., Ltd. leverages years of experience and technical expertise to develop customized solutions tailored to the specific needs of clients, ensuring optimal performance and reliability. The company’s commitment to excellence is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes.
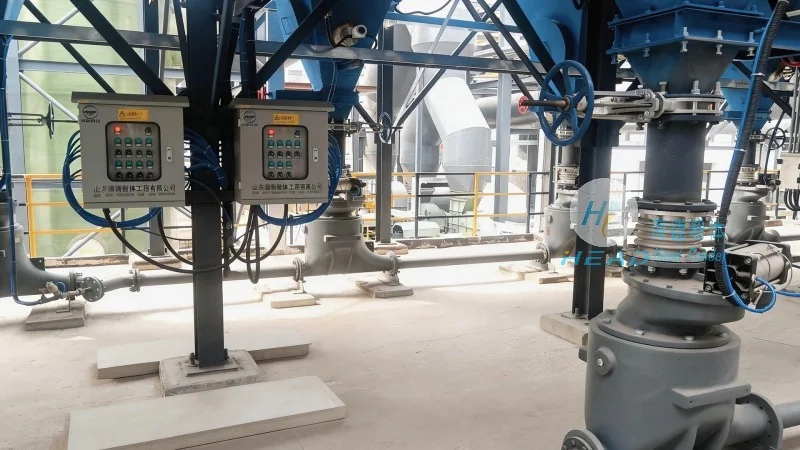
The operation of a sodium silicate pneumatic conveying system begins with the material being fed into a hopper. From there, the material passes through a rotary airlock, which regulates the flow and prevents backflow. Simultaneously, a blower or compressor generates a high-pressure air stream that is introduced into the conveying line. The air stream carries the sodium silicate particles through the line to a receiver, where the material is collected and the air is filtered or recycled. This process is continuous and can be adjusted to handle varying material volumes and flow rates, making it highly adaptable to different production requirements.
The sodium silicate pneumatic conveying system offers several distinct advantages that make it a preferred choice for industrial applications. Firstly, it provides a clean and hygienic method of material handling, which is essential for sodium silicate, a chemical often used in food and pharmaceutical industries. The system minimizes dust generation and contamination, ensuring that the material remains in its original state. Secondly, it is highly efficient, with the ability to transport materials over long distances with minimal energy consumption compared to other methods. Additionally, the system is flexible, allowing for easy integration into existing production lines and the ability to handle different particle sizes and moisture contents. The safety features, such as pressure relief valves and explosion-proof designs, further enhance its reliability and operational safety.
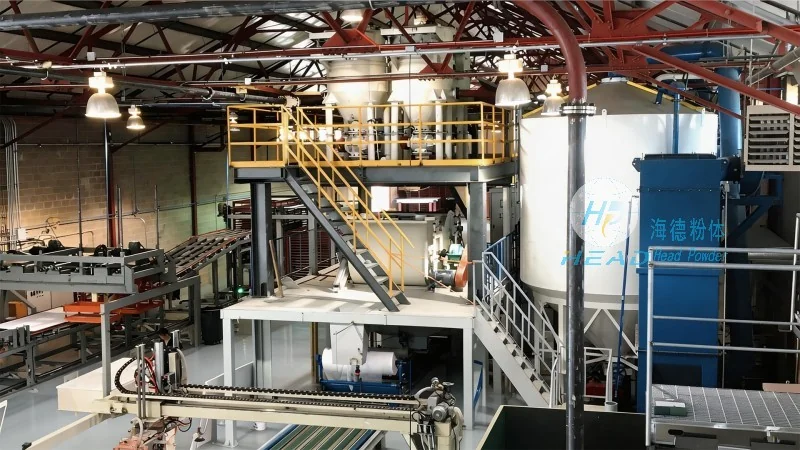
Sodium silicate pneumatic conveying systems are widely used in various industrial sectors where sodium silicate is a key component. In the glass manufacturing industry, the system is used to transport raw materials to the production line, ensuring a steady supply of sodium silicate for glass formulation. In the construction industry, it is employed to deliver sodium silicate for use in cement and concrete additives, improving the durability and properties of building materials. The chemical industry also utilizes this system for the handling of sodium silicate in the production of detergents, adhesives, and other chemical products. In each of these applications, the system’s ability to handle bulk materials efficiently and safely contributes to improved productivity and operational efficiency.
In conclusion, the sodium silicate pneumatic conveying system is a highly effective and reliable solution for the transportation of sodium silicate in industrial settings. By leveraging advanced pneumatic technology, the system offers numerous benefits, including improved cleanliness, energy efficiency, and operational flexibility. The expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd. ensures that these systems are designed and manufactured to meet the highest standards of performance and safety. As industries continue to seek more efficient and sustainable material handling solutions, the sodium silicate pneumatic conveying system remains a top choice, providing a robust and adaptable approach to managing sodium silicate in various applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top