Organic fertilizer pneumatic conveying systems represent a critical technology in the modern agricultural and fertilizer processing industries. These systems are designed to efficiently transport organic materials, such as compost, manure, and other natural fertilizers, from storage or production areas to processing facilities or distribution points. The technology leverages air pressure to move bulk materials, offering a flexible and often more cost-effective alternative to traditional mechanical conveying methods.
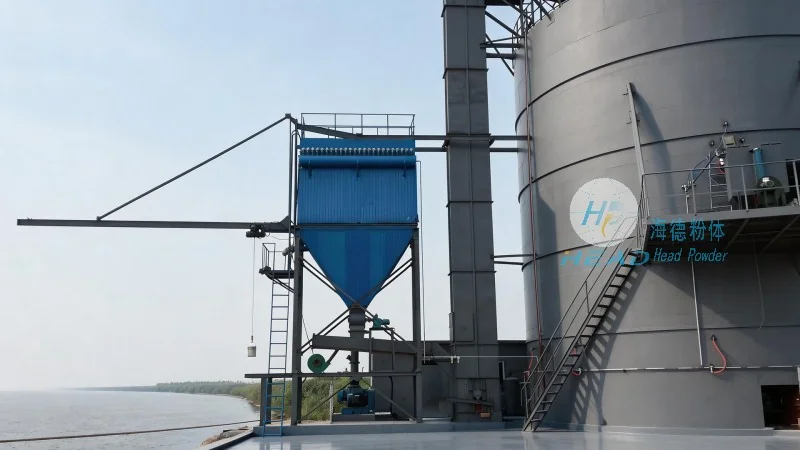
At the core of any pneumatic conveying system for organic fertilizer are several key components. The system typically includes a hopper or storage bin to hold the organic material, a blower or air compressor to generate the necessary air pressure, a pipeline network to transport the material, and a receiver or discharge point where the fertilizer is deposited. Additionally, components like filters, cyclones, and control valves are often integrated to ensure efficient operation and material handling. The design of these components must consider the unique properties of organic fertilizers, such as their moisture content, particle size, and potential for dust generation.
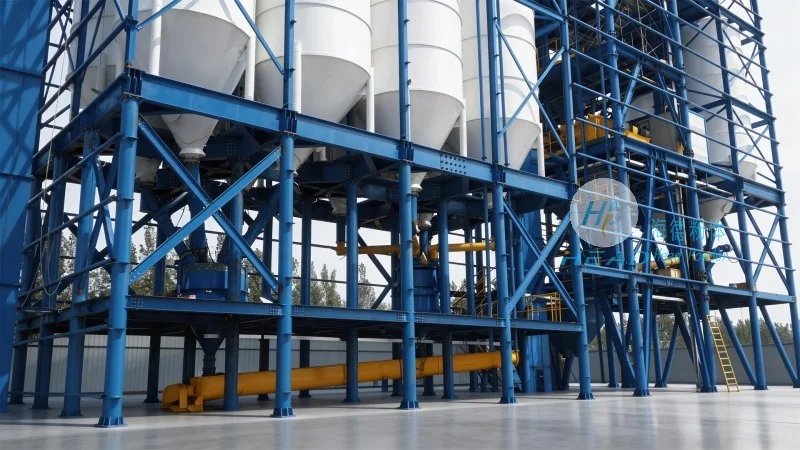
One of the primary advantages of pneumatic conveying systems for organic fertilizer is their ability to handle bulk materials with minimal human intervention. Unlike traditional methods that may require manual loading or mechanical conveyors that can be prone to blockages, pneumatic systems can operate continuously, reducing labor costs and increasing productivity. Furthermore, these systems offer greater flexibility in terms of layout and routing, allowing for the integration of multiple storage and processing points within a facility. The technology also minimizes material degradation, as the enclosed system prevents exposure to air and moisture, preserving the quality of the organic fertilizer.
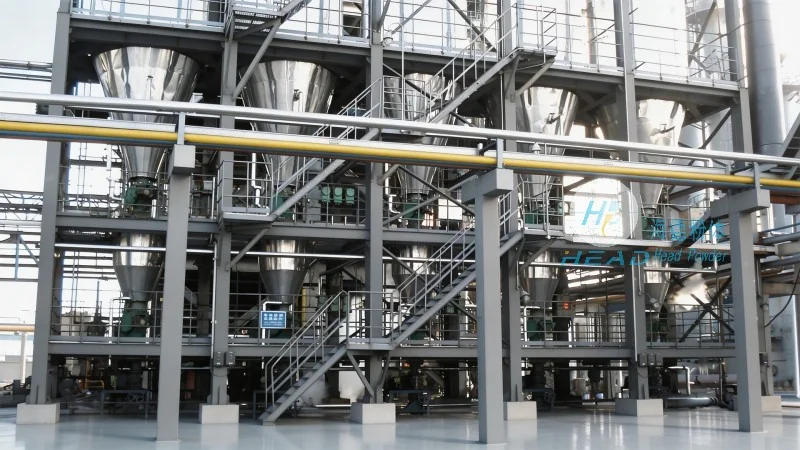
Pneumatic conveying systems are widely used in various applications within the organic fertilizer industry. They are commonly employed in composting facilities, where raw materials are transported from storage to composting reactors. In addition, these systems are utilized in fertilizer blending and packaging operations, where organic materials are mixed with other nutrients before distribution. Operational considerations include the selection of appropriate air velocity and pressure to prevent material degradation or pipeline blockages. Regular maintenance of the blower and filter system is also crucial to ensure consistent performance and to prevent downtime.
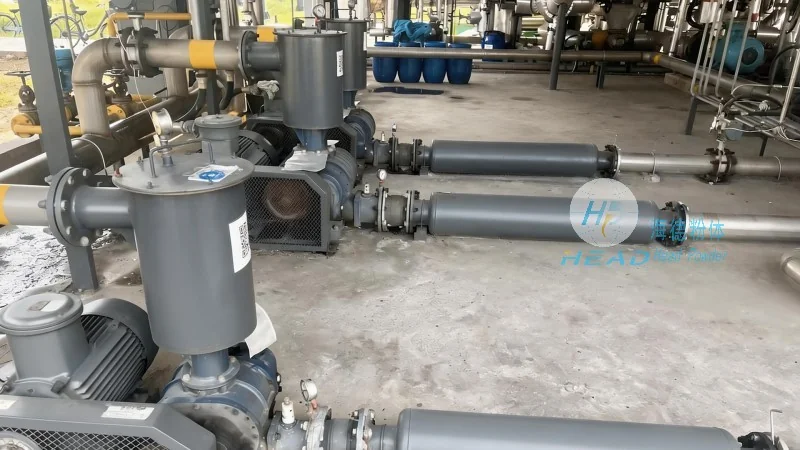
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored to the needs of the organic fertilizer industry. With years of experience and a commitment to innovation, HeadPowder provides customized solutions that enhance efficiency and reliability in fertilizer handling processes. The company’s expertise lies in understanding the unique challenges of organic materials and developing systems that address these challenges effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top