Rare earth ore powder is a critical raw material in various high-tech industries, including electronics, renewable energy, and advanced manufacturing. The efficient and reliable transportation of these fine powders is essential for industrial processes, as it directly impacts production efficiency, product quality, and operational safety. Pneumatic conveying systems have emerged as a preferred method for handling rare earth ore powders due to their ability to transport materials in a closed system, minimizing dust exposure and environmental contamination. This article provides an overview of the structure and operational principles of rare earth ore powder pneumatic conveying systems, highlighting key components and their functions.
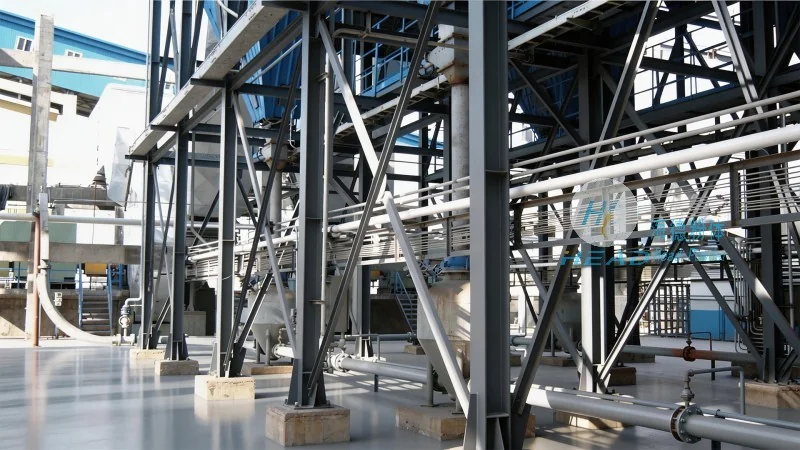
A typical pneumatic conveying system for rare earth ore powders consists of several interconnected components designed to facilitate the transport of fine powders from a source to a destination. The main components include the material hopper, feeder, conveying line, and receiver. Each component plays a crucial role in ensuring the smooth and efficient operation of the system.
The material hopper is the initial storage container where the rare earth ore powder is held before being fed into the system. It is typically designed with a sloped bottom to facilitate the flow of powder into the feeder. The hopper is equipped with a dust collection system to prevent dust accumulation and maintain a clean working environment. The feeder, often a rotary valve or a screw feeder, regulates the flow rate of the powder into the conveying line. This component ensures a consistent and controlled feed of the material, preventing overloading or underfeeding that could lead to system inefficiencies.
The conveying line is the core of the pneumatic system, responsible for transporting the powder through the air. It can be either a positive pressure system, where air is blown into the line to push the powder, or a negative pressure system, where air is drawn out to pull the powder. For rare earth ore powders, which are often abrasive and can cause wear on the system components, the conveying line is typically made of materials such as stainless steel or high-grade plastic to ensure durability and longevity. The line is also equipped with pressure regulators and filters to maintain optimal pressure and air quality.
The receiver is the final destination where the rare earth ore powder is deposited after being conveyed. It is designed to collect the powder and prevent spillage or contamination. The receiver may include a dust collection system to capture any residual powder particles, ensuring a clean and safe environment. In some cases, the receiver is connected to a storage silo or a processing unit, allowing for further use of the material.
The operational principle of a pneumatic conveying system involves the use of air to move the rare earth ore powder through the conveying line. In a positive pressure system, a blower or compressor generates high-pressure air that is introduced into the material hopper. The air then lifts the powder particles and carries them through the conveying line to the receiver. The air velocity in the line must be sufficient to overcome the gravitational force and the friction between the powder particles and the line walls. The velocity is typically maintained at a level that prevents particle settling or clogging in the line.
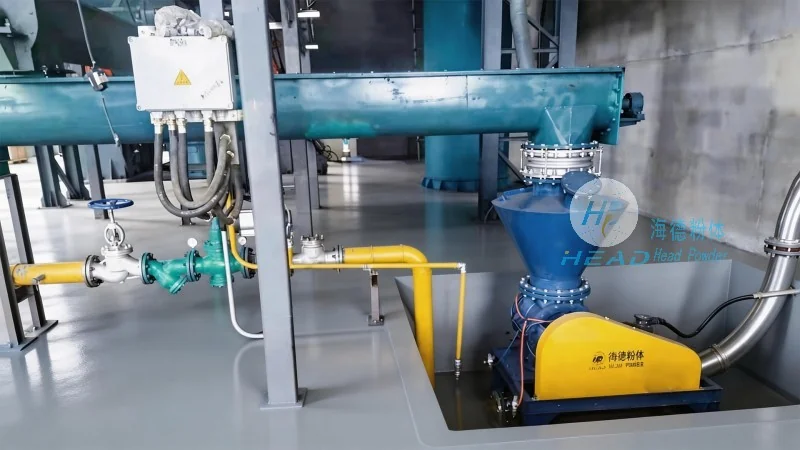
In a negative pressure system, a vacuum pump or fan creates a low-pressure environment at the receiver end of the line. This creates a pressure differential that draws the powder from the hopper into the line and towards the receiver. The air flow in this system is controlled to ensure that the powder particles are not drawn out of the line prematurely, which could lead to dust emissions and safety hazards.
The choice between positive and negative pressure systems depends on various factors, including the distance of the conveying line, the type of powder, and the required flow rate. For rare earth ore powders, which are often fine and can be easily suspended in air, both systems can be effective. However, positive pressure systems are generally preferred for longer conveying distances or when dealing with abrasive powders, as they provide better control over the air flow and pressure.
Pneumatic conveying systems offer several advantages when handling rare earth ore powders. One of the primary benefits is the ability to transport the material in a closed system, which minimizes dust exposure and reduces the risk of environmental contamination. This is particularly important for rare earth powders, which can be hazardous if inhaled or if they come into contact with skin. The closed system also helps to maintain the purity of the powder, preventing contamination from external sources.
Another advantage is the flexibility of the system. Pneumatic conveying systems can be easily modified or expanded to accommodate changes in production needs or to transport materials to different locations. The system can be integrated with other processing equipment, such as grinding or mixing units, to create a seamless production line. This integration improves overall operational efficiency and reduces downtime.
The system also provides better control over the flow rate and pressure, which is crucial for maintaining the quality of the rare earth ore powder. By regulating the air flow and pressure, operators can ensure that the powder is transported at the optimal velocity, preventing particle damage or degradation. This is especially important for rare earth powders, which are often sensitive to mechanical stress and can lose their properties if not handled carefully.
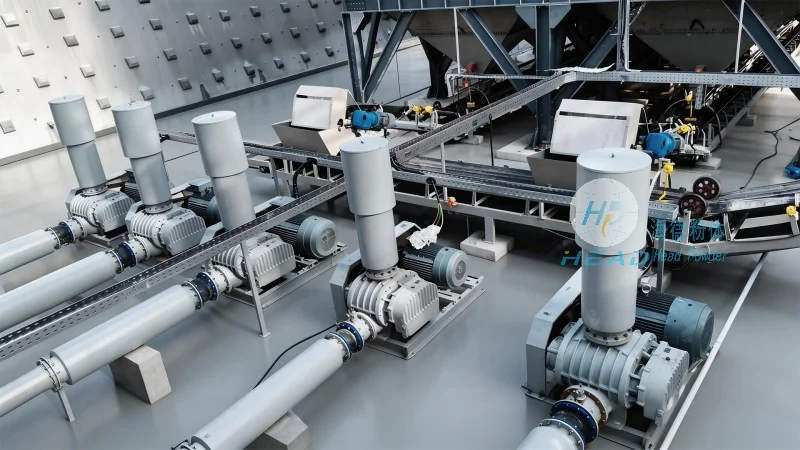
Pneumatic conveying systems are widely used in the processing of rare earth ore powders in various industries. In the electronics industry, rare earth powders are used in the production of magnets, which are essential components in electric vehicles, wind turbines, and consumer electronics. The pneumatic conveying system ensures that these fine powders are transported safely and efficiently to the manufacturing facilities, where they are used in the production of high-quality magnets.
In the renewable energy sector, rare earth powders are used in the production of solar panels and batteries. The pneumatic conveying system helps to transport these powders to the production lines, where they are processed into thin films or electrodes. This ensures that the powders are handled with minimal contamination, maintaining the high efficiency of the solar panels and batteries.
In advanced manufacturing, rare earth powders are used in the production of precision components and coatings. The pneumatic conveying system allows for the precise and controlled transport of these powders to the processing units, ensuring that the final products meet the required specifications. This is particularly important in industries such as aerospace and automotive, where precision and quality are critical.
Pneumatic conveying systems are an essential technology for the efficient and safe handling of rare earth ore powders. The structure and operational principles of these systems are designed to meet the specific needs of the rare earth processing industry, ensuring high-quality material transport and minimal environmental impact. As a leading provider of engineering solutions for material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the unique requirements of rare earth ore powders. With a focus on innovation and quality, the company ensures that its systems are reliable, durable, and cost-effective, helping clients to improve their production efficiency and maintain a competitive edge in the market.
HeadPowder, the professional team behind Shandong HeadPowder Engineering Co., Ltd., brings years of expertise in material handling and engineering to every project. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses in the rare earth processing industry. With its headquarters in Shandong, China, HeadPowder continues to lead the way in developing advanced pneumatic conveying solutions that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top