HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying equipment designed for efficient transport of magnesium oxide powder. This article explores the fundamental principles behind such systems and highlights key working scene characteristics that make them ideal for various industrial applications.
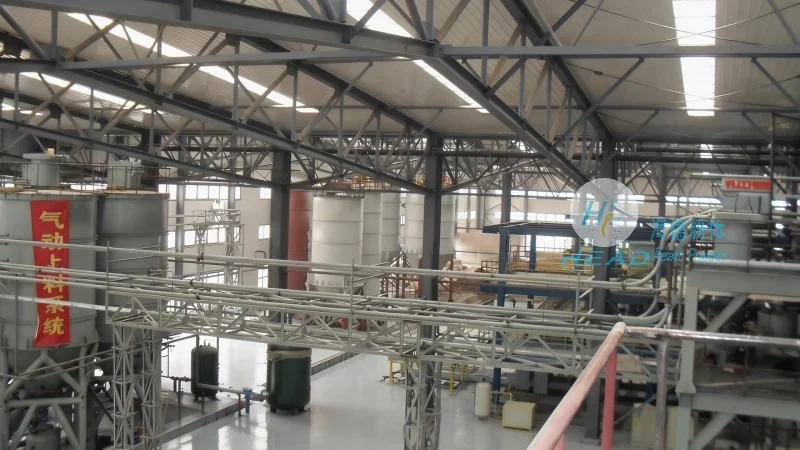
The pneumatic conveying system operates on the principle of transporting bulk materials like magnesium oxide powder through a pipeline using a gas stream, typically air or other gases. This method eliminates the need for mechanical components such as belts or buckets, offering a more hygienic and efficient solution for handling fine powders. The system typically consists of a hopper for material storage, a conveyor line, and a control system that regulates the flow of air and powder. The process involves feeding magnesium oxide powder into the hopper, where it is then drawn into the pipeline by the moving air stream. This creates a dense phase flow, ensuring minimal particle degradation and consistent transport. The design of the system is optimized to maintain the powder's quality, preventing agglomeration or loss of material during transit.
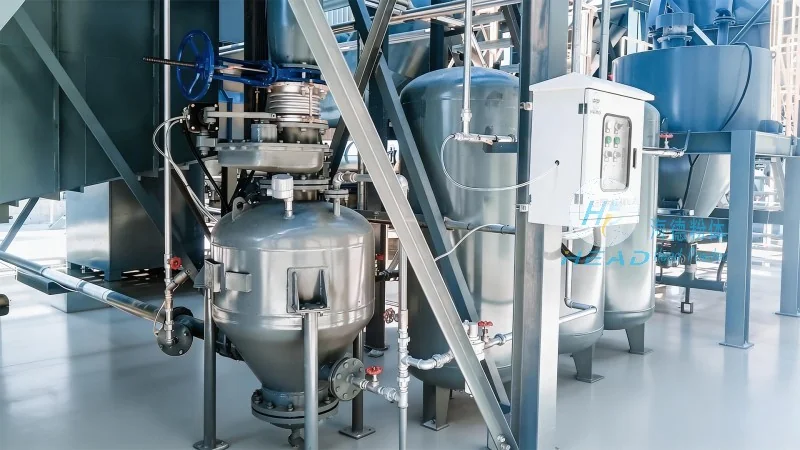
Several key characteristics define the working scenes where magnesium oxide powder pneumatic conveying systems are most effective. Firstly, the systems are highly suitable for applications requiring dust-free and hygienic environments, such as pharmaceutical or food processing industries. The enclosed pipeline design prevents dust emissions, adhering to stringent safety and regulatory standards. Secondly, the flexibility of the system allows for multi-point delivery, enabling the powder to be transported to multiple destinations from a single source. This is particularly beneficial in large-scale production facilities where materials need to be distributed to different processing units or storage areas. Thirdly, the energy efficiency of pneumatic conveying reduces operational costs compared to traditional methods like bucket elevators or belt conveyors. The system's ability to handle varying flow rates and material densities ensures adaptability to different production demands.
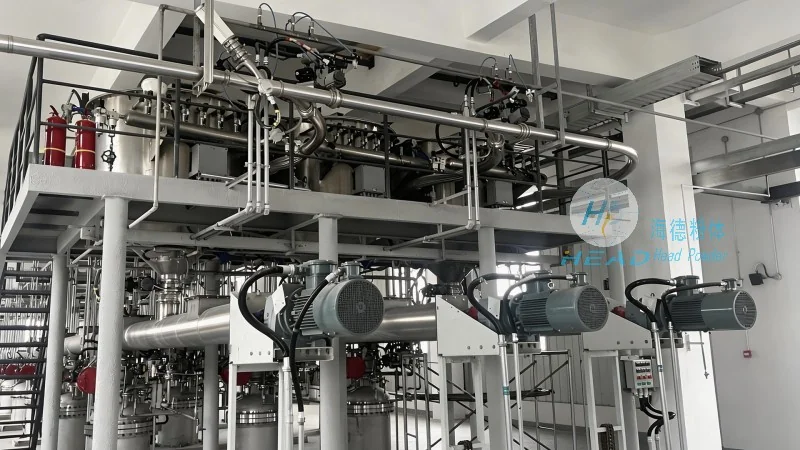
Magnesium oxide powder pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the chemical industry, they are employed for transporting raw materials and finished products, ensuring smooth production workflows. The pharmaceutical sector benefits from the system's ability to maintain product purity and prevent contamination, which is critical for meeting regulatory requirements. Additionally, in the construction materials industry, the system facilitates the transport of magnesium oxide powder for use in cement and other building materials, enhancing production efficiency. The working scene characteristics, such as the ability to handle fine powders without clogging and the maintenance of material integrity, make these systems indispensable in industries where material quality is paramount.
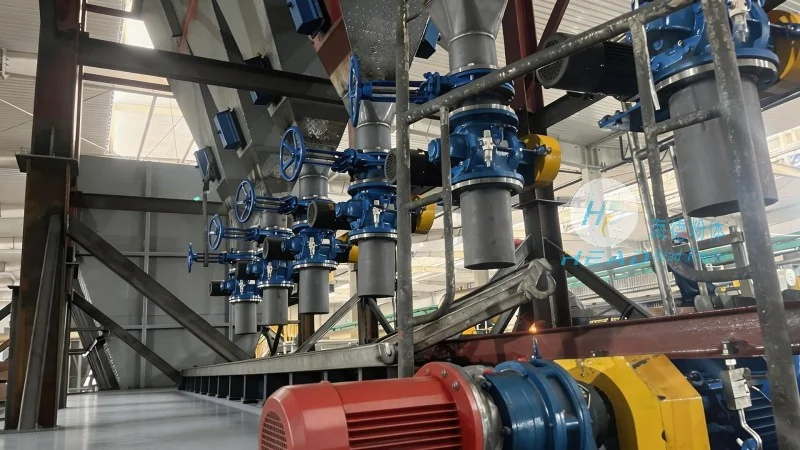
HeadPowder Engineering Co., Ltd., based in Shandong, China, is at the forefront of developing innovative pneumatic conveying solutions tailored to the needs of magnesium oxide powder handling. By leveraging advanced engineering and design principles, the company ensures that its systems meet the highest standards of efficiency, safety, and reliability. The working scene characteristics of these systems, including dust-free operation, multi-point delivery, and energy efficiency, make them a preferred choice for modern industrial applications. As a trusted partner in material handling, HeadPowder continues to advance the technology, providing sustainable and effective solutions for the transport of magnesium oxide powder in diverse industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top