For industrial applications that require the safe and efficient handling of sodium hypochlorite, the pneumatic conveying system offers a reliable solution. This article explores the fundamental principles behind such machinery and highlights the key characteristics of its operational environments, providing insights into how these systems are applied in various industrial settings.
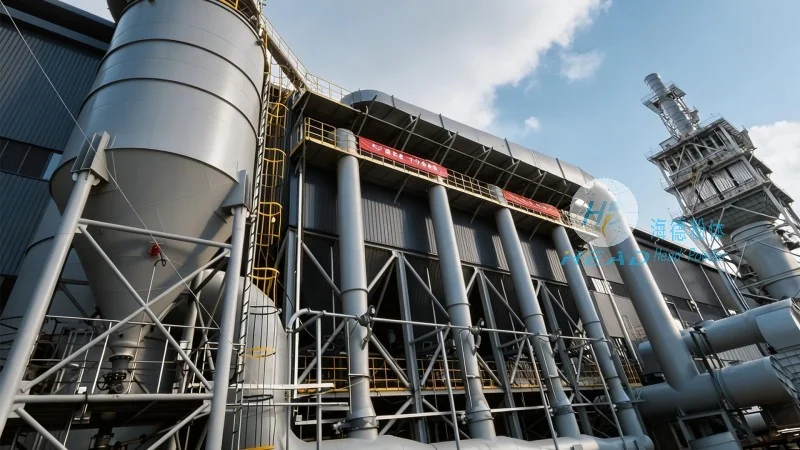
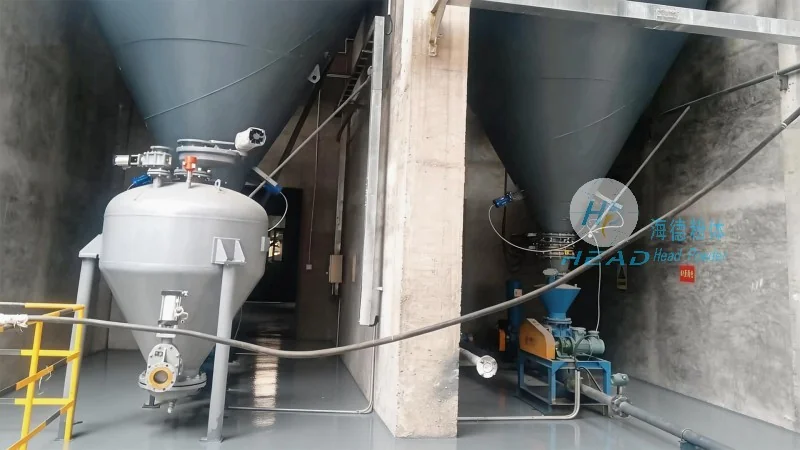
The pneumatic conveying machine for sodium hypochlorite operates on the principle of using air or other gases to transport the liquid or slurry form of the chemical. By creating a pressure differential, the system propels the sodium hypochlorite through a pipeline network, ensuring it moves from the storage or production area to the point of use without the need for mechanical components like pumps or valves that could introduce contamination or damage to the material. This method not only enhances safety by minimizing direct human contact with the chemical but also improves efficiency by automating the transfer process.
The working scene characteristics of sodium hypochlorite pneumatic conveying systems are tailored to meet the demands of specific industrial environments. These systems are commonly employed in water treatment facilities, where they facilitate the distribution of sodium hypochlorite for disinfection purposes. In such settings, the system must maintain strict control over the chemical's concentration and flow rate to ensure consistent water treatment outcomes. Additionally, in industrial cleaning and sanitation operations, the pneumatic conveying machine enables the precise delivery of sodium hypochlorite solutions to cleaning equipment, enhancing the effectiveness of cleaning processes while reducing labor costs.
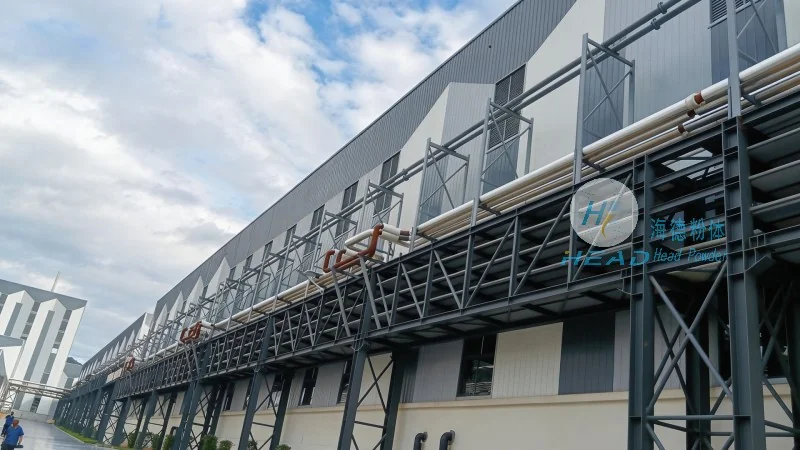
One of the primary advantages of the sodium hypochlorite pneumatic conveying machine is its adaptability to different operational conditions. The system can be configured to handle varying flow rates and pressures, making it suitable for both small-scale and large-scale industrial applications. Furthermore, the enclosed pipeline design minimizes the risk of chemical exposure to the environment and personnel, aligning with environmental regulations and safety standards. This makes the system particularly valuable in industries where compliance with environmental and safety protocols is paramount.
HeadPowder, a leading manufacturer in the field of chemical handling equipment, specializes in the design and production of advanced pneumatic conveying systems for sodium hypochlorite and other hazardous chemicals. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient chemical transfer solutions. HeadPowder's products are engineered to meet the highest industry standards, ensuring durability, safety, and performance in demanding operational environments.
In conclusion, the sodium hypochlorite pneumatic conveying machine represents a sophisticated solution for the safe and efficient handling of this critical chemical. By leveraging the principles of pneumatic transport, these systems enhance operational efficiency, improve safety, and reduce costs in various industrial applications. As industries continue to prioritize sustainability and safety, the adoption of such advanced conveying technologies becomes increasingly important. HeadPowder, with its expertise and commitment to excellence, remains at the forefront of providing tailored solutions that meet the evolving needs of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top