Vacuum pneumatic conveying systems represent a sophisticated method for transporting bulk materials over long distances or within industrial settings. This technology operates by creating a negative pressure environment in a pipeline, which draws material from a source and transports it to a destination. The core principle involves using air as the conveying medium, with the system designed to handle various materials such as powders, granules, and even fine particles. By leveraging negative pressure, these systems offer advantages like reduced material degradation, minimal contamination, and the ability to transport materials in a closed system, ensuring safety and environmental compliance.
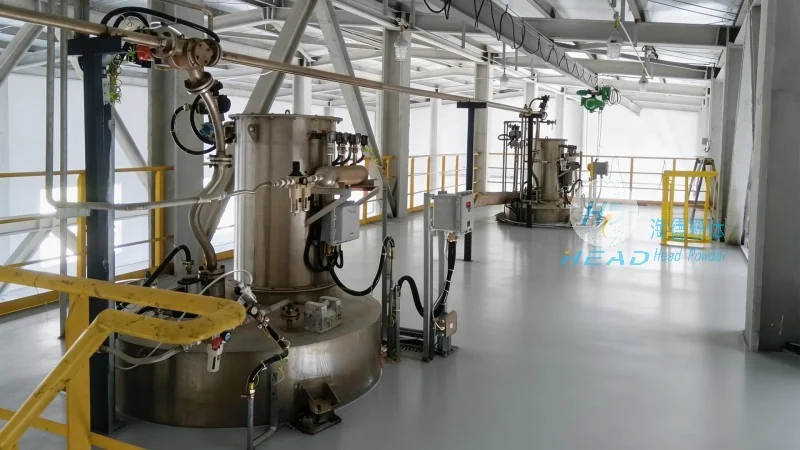
The working scene characteristics of vacuum pneumatic conveying systems are diverse and tailored to specific industrial needs. These systems are commonly employed in sectors like pharmaceuticals, food processing, chemical manufacturing, and mining, where material handling requires precision and cleanliness. In pharmaceutical applications, for instance, the closed system prevents cross-contamination, ensuring product purity. Food processing industries benefit from the hygienic design, which maintains food safety standards. Chemical manufacturers use these systems to transport hazardous materials safely, minimizing exposure risks. Mining operations utilize vacuum conveyors to move ore and minerals from extraction sites to processing facilities, enhancing operational efficiency. The adaptability of vacuum pneumatic conveying systems allows them to integrate seamlessly into existing production lines, improving workflow and reducing downtime.
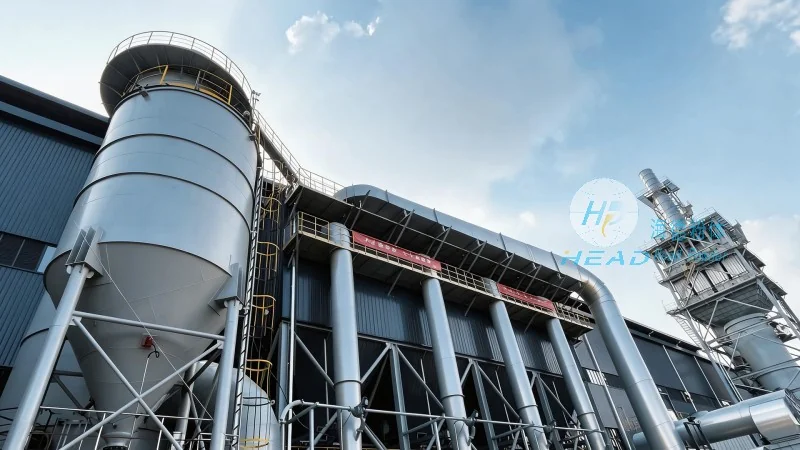
The principle of vacuum pneumatic conveying systems is based on the fundamental physics of air flow and material transport. The system typically consists of a vacuum pump, a material feed hopper, a conveying line, and a discharge point. The vacuum pump creates a low-pressure zone in the pipeline, causing air to flow from the ambient environment into the system, pulling material along with it. The material is fed into the hopper, where it is then drawn into the conveying line by the vacuum. The air and material mixture travels through the pipeline, with the material being separated from the air at the discharge point, often using a cyclone separator or a filter. This separation process ensures that the material is delivered to the destination while the air is recirculated or vented, depending on the system design. The efficiency of the conveying process is influenced by factors such as material properties, air velocity, and pipeline length, all of which are optimized to achieve the desired throughput and material quality.
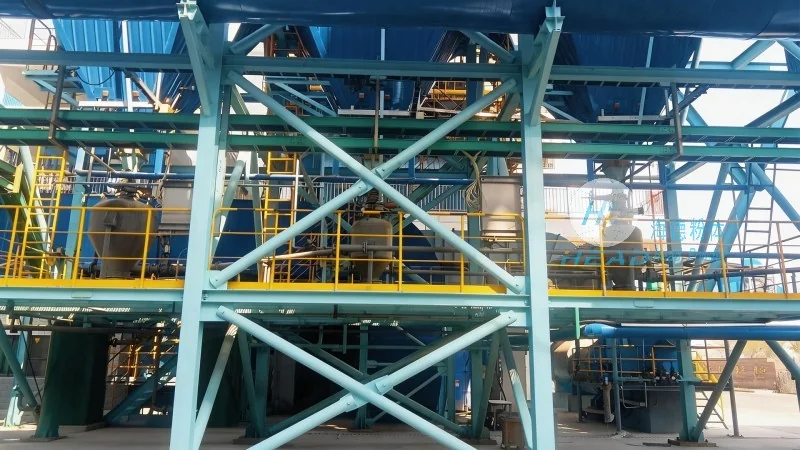
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in vacuum pneumatic conveying systems and related engineering solutions. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted provider of high-quality industrial equipment. Headpowder's expertise lies in designing and manufacturing systems that meet the diverse needs of various industries, ensuring reliability, efficiency, and compliance with international standards. The company's commitment to innovation and customer satisfaction has enabled it to deliver tailored solutions that enhance operational performance and reduce costs for its clients. By leveraging advanced technology and rigorous quality control, headpowder ensures that its vacuum pneumatic conveying systems are durable, efficient, and capable of handling a wide range of materials.
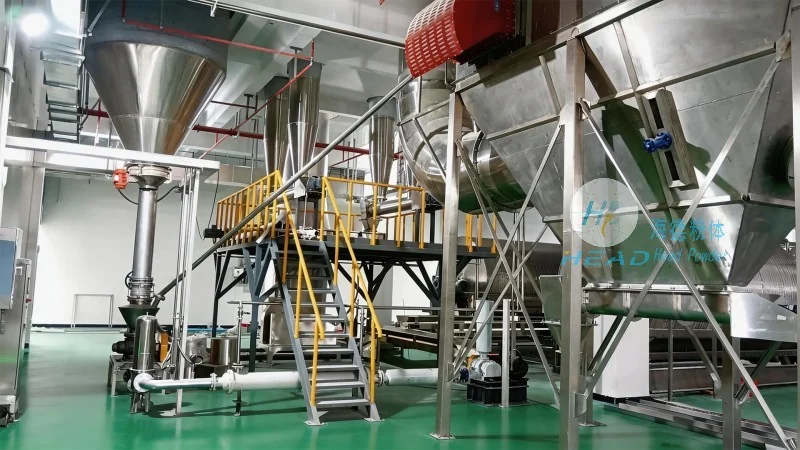
Vacuum pneumatic conveying systems offer several key advantages that make them ideal for many industrial applications. These include the ability to transport materials in a closed system, which prevents dust emissions and contamination, thus improving workplace safety and environmental standards. Additionally, the systems are relatively compact and can be installed in tight spaces, making them suitable for facilities with limited room for equipment. The closed design also reduces material loss and improves product quality by minimizing exposure to air and moisture. From a practical standpoint, vacuum conveyors are easy to integrate with existing production lines and can be customized to handle specific material types and throughput requirements. However, it is important to consider factors such as material density, flowability, and moisture content when designing a vacuum pneumatic conveying system, as these can impact system performance and efficiency. Proper maintenance, including regular cleaning of the conveying line and filter, is also essential to ensure long-term operation and prevent downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top