HeadPowder, a leading manufacturer of industrial material handling solutions, specializes in the design and production of advanced pneumatic conveying systems tailored for transporting bulk materials such as coke and limestone powder. This article explores the fundamental principles behind these systems and highlights the key characteristics of their application across various industrial settings.
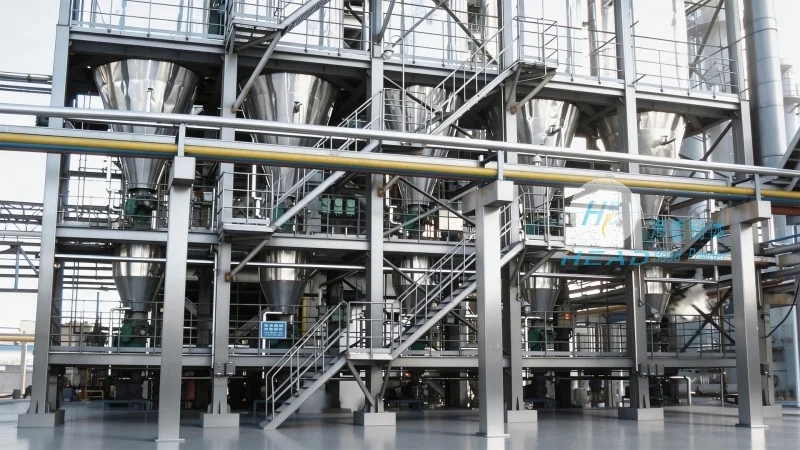
Pneumatic conveying technology has become an essential method for transporting dry bulk materials like coke and limestone powder in modern industrial processes. Unlike traditional mechanical conveyors, which rely on belts, chains, or screws, pneumatic systems utilize a stream of air to move particles through a network of pipes. This approach offers significant advantages, including reduced material degradation, minimal contamination, and the ability to handle materials with high moisture content or abrasive properties.
HeadPowder, based in Shandong, China, is a reputable company dedicated to providing high-quality pneumatic conveying equipment. With years of experience in the industry, the company has developed a comprehensive range of solutions that cater to the unique demands of coke and limestone powder handling. The company's commitment to innovation and customer satisfaction has established it as a trusted partner for businesses seeking reliable material transport solutions.
The core principle of pneumatic conveying involves creating a flow of air within a pipeline to transport solid particles. There are two primary types of systems: suction (or vacuum) conveying and pressure conveying. Suction systems use a vacuum at the inlet to draw material from a hopper or storage silo into the pipeline, while pressure systems use compressed air to push material from a storage vessel through the system. For coke and limestone powder, the choice of system depends on factors such as the distance of material transport, the required flow rate, and the presence of multiple discharge points.
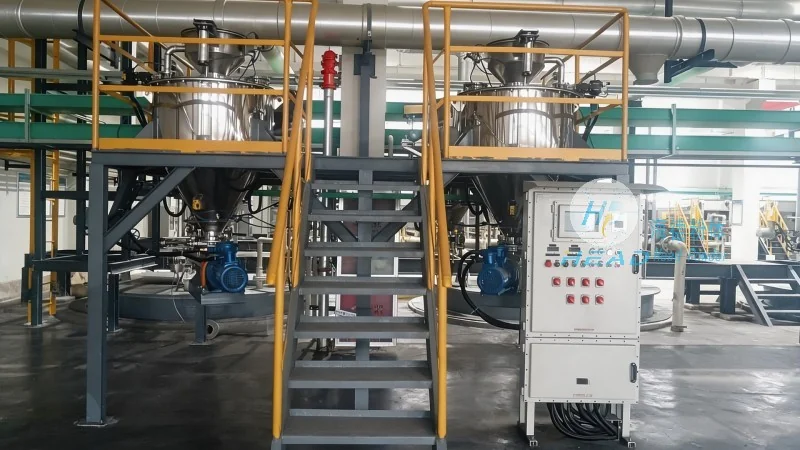
In both systems, the material is suspended in the air stream and carried through the pipeline. The design of the conveying line, including the pipe diameter, bends, and fittings, is critical to maintaining the flow of material and preventing blockages. Additionally, the system incorporates components like airlocks, cyclones, and filters to separate the material from the air and ensure efficient operation.
Coke, a carbon-rich byproduct of coal processing, and limestone powder, a common industrial raw material, have distinct physical properties that influence the design and performance of pneumatic conveying systems. Coke particles typically have a higher density and are more abrasive compared to limestone powder, which may have a finer particle size and varying moisture content. These characteristics affect the selection of materials for the conveying components, such as the use of wear-resistant coatings on pipelines and components to withstand the abrasive nature of coke. Additionally, the moisture content of limestone powder can impact the flowability of the material, requiring adjustments in air pressure and flow rate to maintain consistent performance.
The application of coke and limestone powder pneumatic conveying equipment varies across different industrial sectors, each with its own specific requirements. In the steel industry, for example, coke is a critical raw material used in blast furnaces, and efficient transportation from storage to the furnace is essential for production continuity. The conveying systems in this sector often involve long-distance horizontal transport and vertical elevation to deliver coke to the top of the furnace. In the cement industry, limestone powder is a primary ingredient in clinker production, and the equipment must handle large volumes of material with high flow rates and minimal downtime.
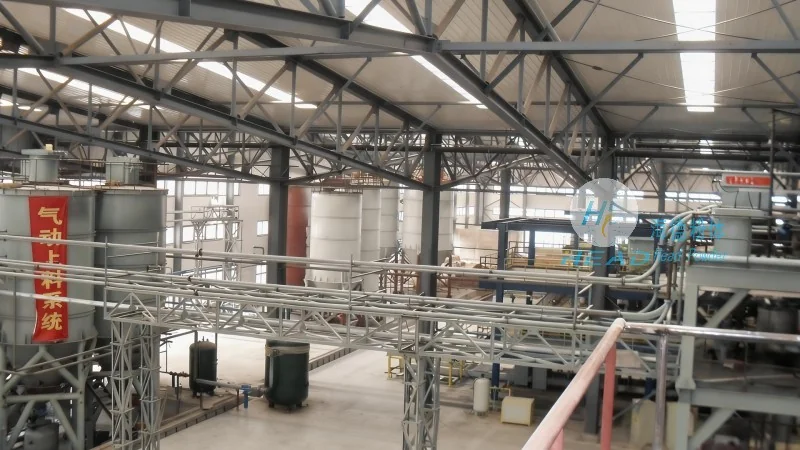
In chemical processing plants, the handling of limestone powder is crucial for flue gas desulfurization processes, where the powder is used to neutralize acidic gases. The conveying systems in these applications must be designed to handle corrosive environments and ensure precise dosing of the material. Furthermore, in power plants, both coke and limestone powder are used in coal-fired boilers, where the equipment must operate under high-temperature and high-pressure conditions while maintaining reliable performance.
The use of pneumatic conveying systems for coke and limestone powder offers several advantages over traditional methods. These include improved safety by reducing manual handling of powders, enhanced environmental protection by minimizing dust emissions, and increased efficiency through automated operation. However, the success of these systems depends on proper design and maintenance. Factors such as the particle size distribution, moisture content, and flow rate must be carefully considered to prevent blockages and ensure consistent material transport. Regular maintenance of components like airlocks, filters, and pipelines is also essential to maintain system efficiency and longevity.
HeadPowder's coke and limestone powder pneumatic conveying equipment exemplifies the advanced technology and engineering expertise required to handle challenging industrial materials. By understanding the principles of pneumatic conveying and adapting to the specific characteristics of coke and limestone powder, these systems provide reliable, efficient, and environmentally friendly solutions for various industrial applications. With a strong presence in Shandong, China, HeadPowder continues to innovate and deliver high-quality equipment that meets the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top