Rare earth powders are critical components in modern industrial applications, including electronics, renewable energy, and advanced materials. Efficient and reliable material handling is essential to maintain product quality and operational efficiency. Pneumatic conveying systems offer a versatile solution for transporting rare earth powders, providing advantages such as dust-free operation, low maintenance, and the ability to handle sensitive materials without degradation. These systems are designed to address the unique challenges posed by rare earth powders, including their fine particle size, hygroscopic nature, and potential for static buildup, ensuring that the material is transported safely and effectively from source to destination.
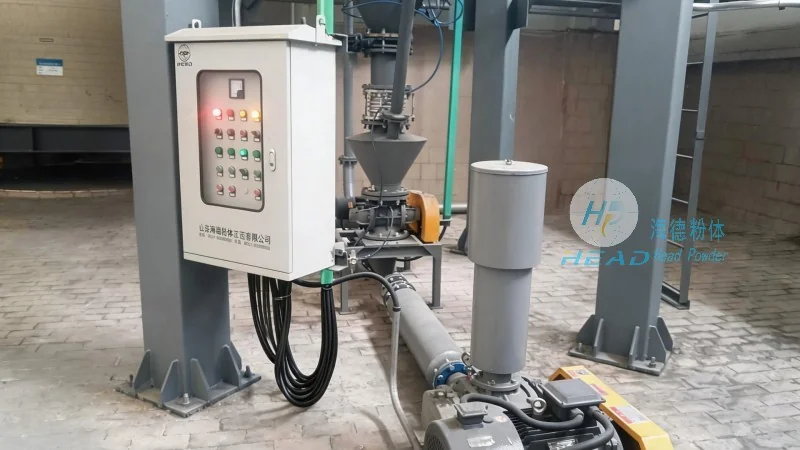
Company Overview
HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of rare earth powder industries. With a strong commitment to innovation and quality, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses seeking advanced material transport technologies. HeadPowder's expertise lies in understanding the specific challenges of rare earth powders, such as their fine particle size, moisture sensitivity, and potential for static discharge, and developing systems that address these challenges effectively. The company's team of engineers and technicians work closely with clients to develop customized solutions that meet their specific operational requirements and industry standards.
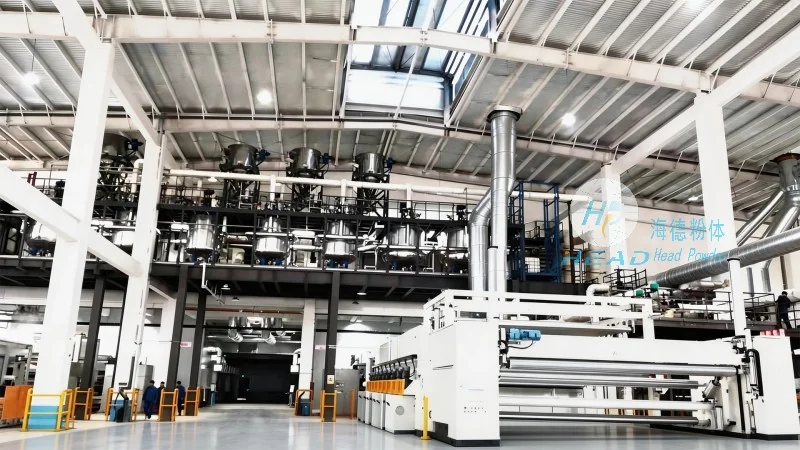
Key Features of Pneumatic Conveying Systems for Rare Earth Powders
Pneumatic conveying systems for rare earth powders are engineered to ensure optimal performance and durability. Key features include:
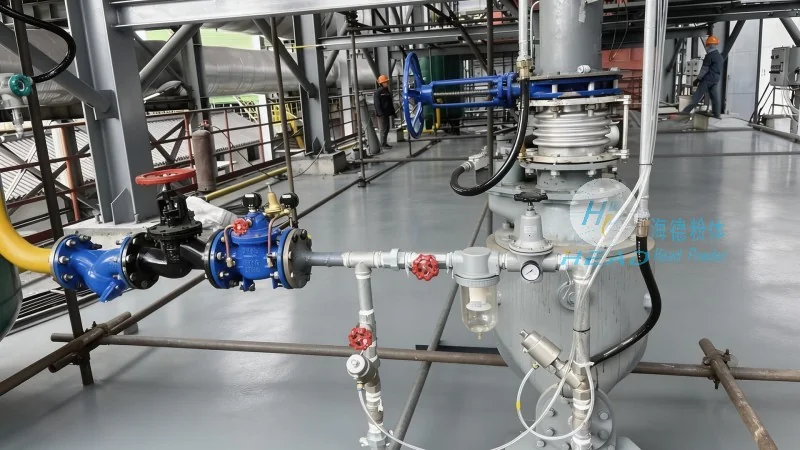
- Dust-Free and Clean Operation: Unlike traditional bulk handling methods, pneumatic systems minimize dust generation, enhancing workplace safety and compliance with environmental regulations. This is particularly important in industries where dust can pose health risks or interfere with downstream processes.
- Low Maintenance Requirements: Advanced materials and robust design reduce the need for frequent repairs, lowering long-term operational costs. Systems are built with components that are resistant to corrosion and wear, ensuring reliable performance over extended periods.
- Adaptability to Material Properties: Systems can be customized to handle varying particle sizes, moisture content, and flow rates, ensuring consistent performance. This adaptability allows HeadPowder to provide solutions that are tailored to the specific characteristics of each rare earth powder, whether it is a light rare earth like cerium or a heavy rare earth like dysprosium.
- Energy Efficiency: Modern systems incorporate energy-saving technologies, reducing operational expenses while maintaining high throughput. By optimizing air pressure and flow rates, these systems minimize energy consumption without compromising material transport efficiency.
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system involves the use of air or gas to transport particulate materials. In the case of rare earth powders, the process typically involves several key steps:
- Feeding: The rare earth powder is fed into the system using a hopper or feeder, ensuring a consistent flow rate. The feeder is designed to prevent material bridging or clogging, which can disrupt the conveying process.
- Conveying: Air is introduced into the system, creating a flow that lifts and transports the powder through a pipeline. The velocity of the air is critical to maintain the powder in suspension and prevent clogging. The air velocity must be sufficient to overcome the gravitational force acting on the particles and to keep them suspended in the air stream.
- Separation and Discharge: At the destination, the air is separated from the powder, often using cyclones or filters, and the powder is collected in a receiving container. The separation process is designed to maximize the recovery of the rare earth powder while minimizing air loss, ensuring efficient material handling.
Technical Specifications and Application Considerations
When selecting a pneumatic conveying system for rare earth powders, several technical specifications and application factors must be considered to ensure optimal performance and reliability:
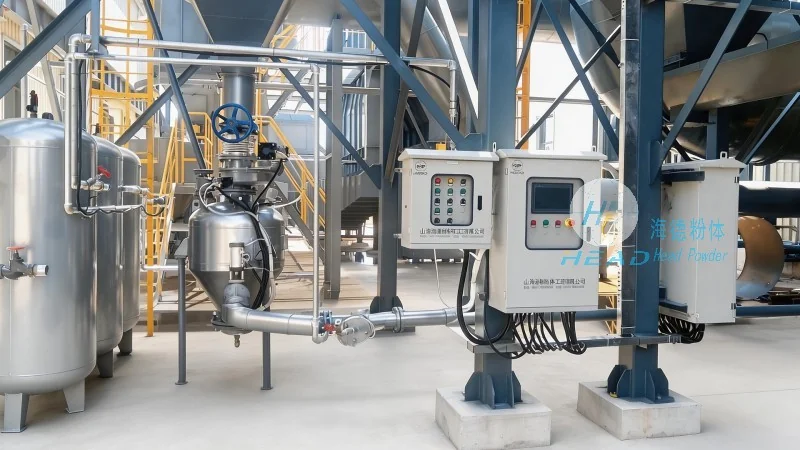
- Particle Size and Density: The system's design must accommodate the specific particle size distribution and density of the rare earth powder to ensure efficient transport. For example, fine powders may require higher air velocities and more efficient separation equipment to prevent loss or clogging.
- Moisture Content: Hygroscopic powders require systems with moisture-resistant components to prevent clumping or degradation. HeadPowder's systems incorporate materials and coatings that resist moisture absorption, ensuring that the rare earth powder remains in a dry, transportable state.
- Static Control: Proper grounding and anti-static measures are essential to prevent static buildup, which can affect material flow and safety. The system design includes features such as conductive materials and grounding straps to mitigate static discharge risks.
- System Pressure and Flow Rate: The pressure and flow rate of the conveying air must be optimized to match the material's properties and the required throughput. HeadPowder provides detailed engineering analyses to determine the optimal pressure and flow rates for each application, ensuring that the system operates efficiently and within safe limits.
Conclusion
Pneumatic conveying systems represent a sophisticated and effective solution for handling rare earth powders, offering numerous benefits over traditional methods. By leveraging advanced engineering and material handling expertise, companies like Shandong HeadPowder Engineering Co., Ltd. provide tailored systems that enhance operational efficiency, maintain product integrity, and ensure compliance with industry standards. For businesses in the rare earth industry, investing in a reliable pneumatic conveying system is a strategic decision that supports long-term success and sustainability. With their commitment to quality and innovation, HeadPowder continues to be a leader in providing cutting-edge material transport solutions for the global rare earth market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
