Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions tailored for agricultural products like beans. The primary challenge in bean transport via pneumatic systems is preventing pipeline blockages, which can lead to operational inefficiencies and increased maintenance costs. This article explores effective strategies and critical design parameters that ensure smooth and reliable bean conveying, minimizing blockage risks.
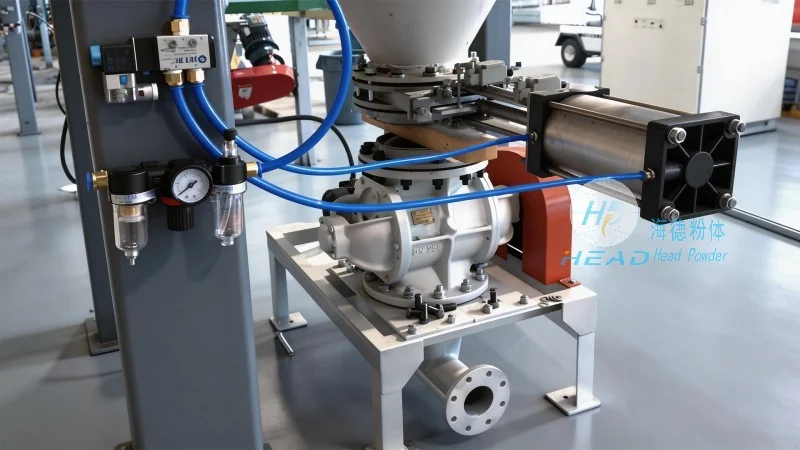
When handling beans, especially those with high moisture content or irregular shapes, the risk of blockages in pneumatic pipelines increases significantly. Blockages can occur due to agglomeration, excessive particle size, or improper air flow dynamics. These issues not only disrupt the conveying process but also damage equipment and reduce overall system efficiency. Therefore, implementing robust design measures is essential to maintain consistent performance and prolong the lifespan of the conveying system.
The success of a pneumatic conveying system in preventing blockages in bean transport hinges on several critical design parameters. These parameters are carefully selected based on the physical properties of the beans, the system layout, and the desired conveying capacity. Below are the most important factors to consider:
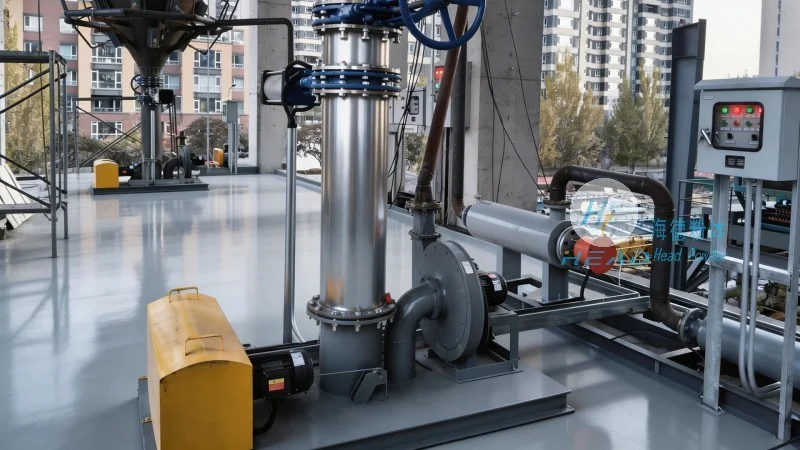
Optimizing air velocity is one of the most effective ways to prevent blockages. The air velocity must be sufficient to lift and transport the beans through the pipeline without causing excessive pressure drops or particle deposition. For beans, a typical air velocity range is between 20 to 30 meters per second (m/s), depending on the bean size and moisture content. A higher velocity reduces the likelihood of particles settling and forming blockages, while maintaining energy efficiency. The flow rate, calculated as the volume of air per unit time, must be matched to the material feed rate to ensure a consistent and stable conveying process.
The diameter of the conveying pipeline is directly related to the risk of blockages. Larger diameter pipes allow for lower air velocities while still maintaining the required flow rate, reducing the chance of particle accumulation. For bean transport, a pipeline diameter of 100 to 150 millimeters is commonly used, depending on the throughput capacity. The length of the pipeline also impacts blockage risk; longer pipelines require higher air velocities or additional air boosters to maintain adequate flow. Properly sizing the pipeline diameter and length ensures that the system operates within optimal pressure and velocity ranges, minimizing the potential for blockages.
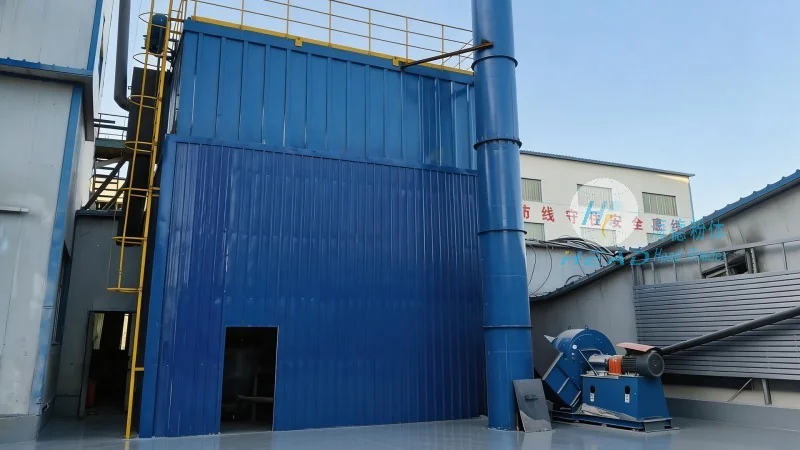
The rate at which beans are fed into the system is a critical factor in preventing blockages. Inconsistent or high feed rates can cause surges that lead to particle agglomeration and blockages. Using feeders such as rotary valves or screw feeders that provide a uniform and controlled feed rate is essential. The feed rate should be matched to the system's capacity, ensuring that the air flow can handle the material without overwhelming the pipeline. Uniformity in feed also helps maintain a stable pressure gradient along the pipeline, reducing the risk of localized blockages.
Appropriate air pressure is crucial for effective bean conveying. The system typically operates under positive pressure, where air is forced through the pipeline carrying the beans. The pressure level is determined by the pipeline length and diameter, as well as the material's density and flow characteristics. Booster systems, which increase the air pressure at intervals along the pipeline, are often used for long-distance conveying. These boosters help maintain the air velocity and prevent pressure drops that could lead to blockages. Properly designed booster systems ensure that the air pressure remains consistent throughout the conveying process, supporting smooth material transport.
The design of the inlet and outlet components plays a significant role in preventing blockages. The inlet, where the beans are introduced into the pipeline, should be designed to minimize turbulence and particle separation. A well-designed inlet ensures that the beans are fully entrained by the air stream, reducing the risk of material buildup at the entry point. The outlet, where the beans are discharged, should be equipped with a suitable valve or diverter to prevent backflow and ensure complete material discharge. Proper inlet and outlet design helps maintain the flow dynamics and prevents blockages at critical junctions.
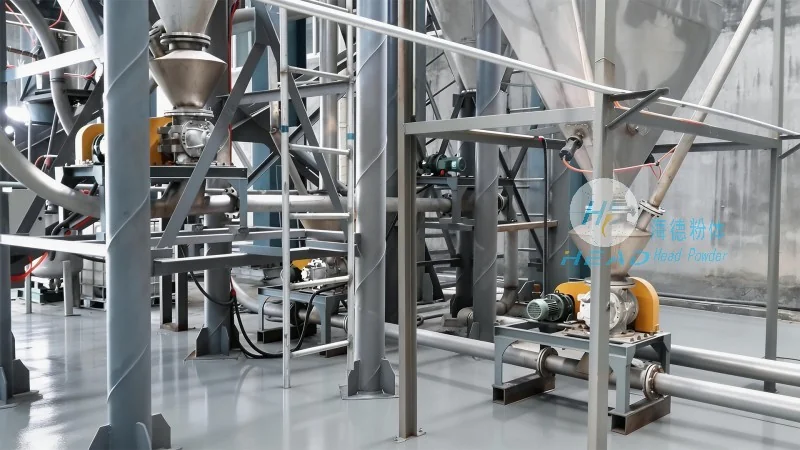
Pre-treating the beans before conveying can significantly reduce blockage risks. Conditioning the beans to adjust their moisture content or applying anti-caking agents can improve their flowability. For example, drying beans to a lower moisture level reduces their tendency to agglomerate, making them easier to convey. Additionally, using screening or sorting equipment to remove oversized or damaged beans can prevent blockages caused by irregular particles. Pre-treatment steps are often integrated into the overall conveying system to ensure that only suitable material is processed, enhancing system reliability.
Preventing pipeline blockages in pneumatic bean transport requires a comprehensive approach that considers multiple design parameters. By optimizing air velocity, pipeline dimensions, feed rate, air pressure, and component design, along with proper material conditioning, the risk of blockages can be minimized. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing such advanced pneumatic conveying systems, ensuring that agricultural products like beans are transported efficiently and reliably. With careful attention to these key parameters, businesses can achieve consistent performance, reduce downtime, and enhance the overall productivity of their bean handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top