When it comes to transporting calcium hydroxide powder using pneumatic conveying systems, a common concern for industrial operations is the risk of pipeline blockages. These blockages can lead to system downtime, increased maintenance costs, and reduced productivity. Understanding the root causes and implementing effective design strategies are crucial for maintaining smooth and efficient material transport. This article explores how to prevent pipeline blockages in pneumatic conveying systems for calcium hydroxide powder, with a focus on key design parameters that Shandong HeadPowder Engineering Co., Ltd. (headpowder) recommends.
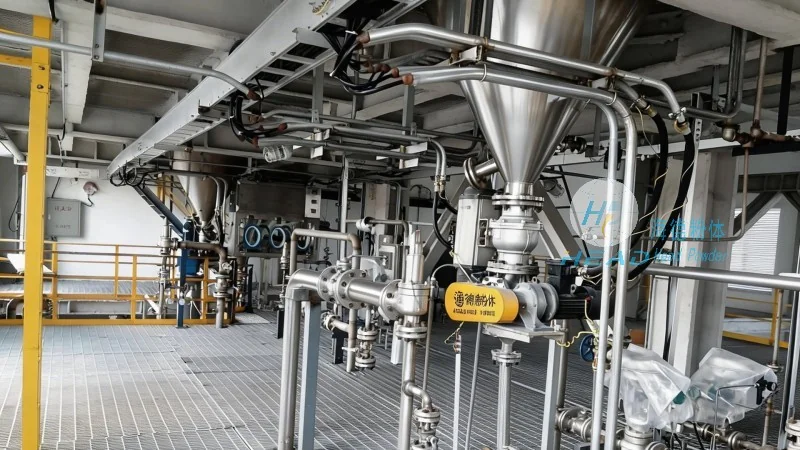
Pipeline blockages in pneumatic conveying systems for calcium hydroxide powder typically arise from several factors. One primary cause is the formation of agglomerates or clumps within the powder due to moisture content or improper blending. When these agglomerates are introduced into the conveying line, they can act as a plug, obstructing the flow of material. Another factor is the high friction between the powder particles and the pipe walls, especially in systems with low air velocity or inadequate air flow rates. Additionally, the presence of foreign materials or contaminants in the powder can contribute to blockages by creating points of friction or causing the material to stick to the pipe interior.
Effective prevention of pipeline blockages in pneumatic conveying systems for calcium hydroxide powder requires careful consideration of several key design parameters. The first parameter is the air velocity within the conveying line. Maintaining an appropriate air velocity is critical to ensure that the powder particles are fully suspended and transported efficiently. For calcium hydroxide powder, headpowder recommends maintaining an air velocity that is at least 20% higher than the minimum fluidization velocity of the powder. This ensures that the particles remain in a fluidized state, reducing the likelihood of agglomeration and blockage.
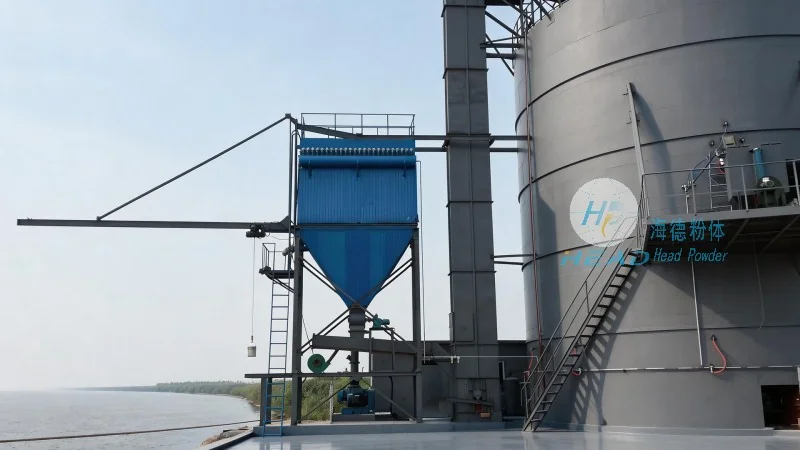
Another critical design parameter is the system's pressure and flow rate. The pressure drop across the conveying line must be carefully managed to prevent excessive friction losses that could lead to reduced air velocity and subsequent blockages. Headpowder suggests using pressure sensors and flow meters to monitor and adjust the system in real-time, ensuring consistent performance. Additionally, the use of appropriate pipe diameters is essential. Larger pipe diameters can reduce the friction between the powder and the pipe walls, allowing for smoother flow and minimizing the risk of blockages. For calcium hydroxide powder, headpowder typically recommends using pipes with diameters ranging from 100mm to 200mm, depending on the system's capacity and the powder's characteristics.
The selection of the right air compressor is also a key design parameter. The compressor must be capable of providing sufficient air volume and pressure to maintain the required air velocity throughout the conveying line. Headpowder recommends using high-efficiency, variable-speed air compressors that can adjust their output based on the system's demand. This not only helps in preventing blockages by maintaining consistent air flow but also reduces energy consumption and operational costs.
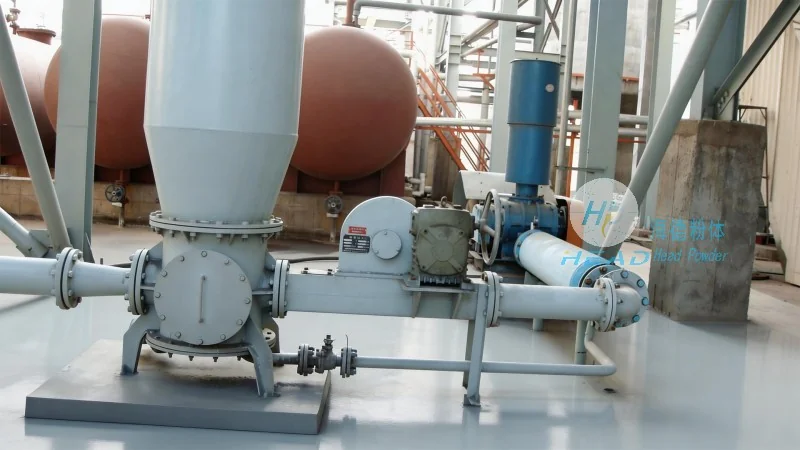
Furthermore, the inclusion of in-line equipment such as cyclones, separators, and filters is important for maintaining system performance and preventing blockages. Cyclones are used to separate the powder from the air stream, while separators can remove larger particles or agglomerates that could cause blockages. Regular maintenance of these components is essential to ensure they function effectively. Headpowder emphasizes the importance of cleaning and replacing filters regularly to prevent clogging, which can otherwise lead to increased pressure drops and system inefficiencies.
Another design parameter is the use of additives or conditioners in the calcium hydroxide powder. Some powders may require the addition of anti-caking agents or lubricants to improve flow characteristics and prevent agglomeration. Headpowder recommends working with the powder supplier to determine the appropriate additives for the specific application, as this can significantly impact the system's performance and reduce the risk of blockages.
While design parameters are crucial, implementing best practices is equally important for preventing pipeline blockages and ensuring the long-term performance of pneumatic conveying systems for calcium hydroxide powder. Regular system maintenance is a top priority. This includes inspecting the conveying line for signs of wear or damage, cleaning the pipe interior to remove any buildup, and checking all components for proper operation. Headpowder advises performing routine maintenance checks at least once a month, or more frequently if the system operates continuously.
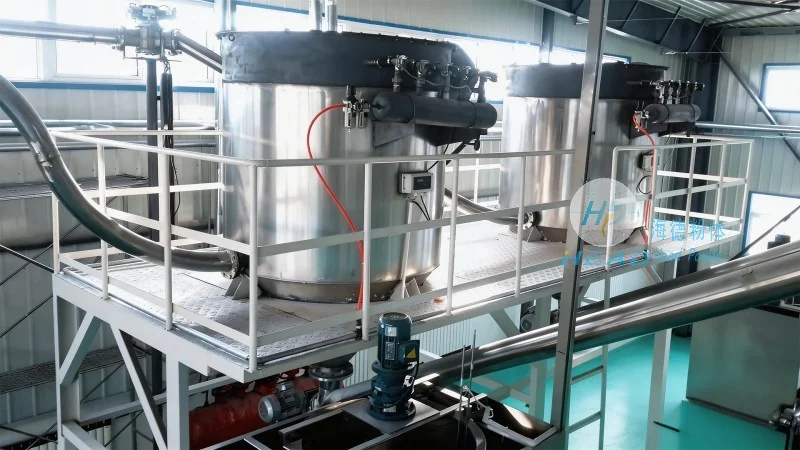
Monitoring system performance is another key practice. Using sensors to track pressure, flow rate, and temperature can help identify potential issues before they lead to blockages. Headpowder recommends setting up a monitoring system that alerts operators to any deviations from normal operating parameters. This allows for timely intervention and prevents minor issues from escalating into major problems.
Training personnel on proper system operation and maintenance is also essential. Operators should be familiar with the system's design and how to recognize signs of potential blockages, such as increased pressure drops or reduced flow rates. Headpowder provides comprehensive training programs for its clients, ensuring that personnel are equipped with the knowledge and skills needed to maintain optimal system performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top