Shandong HeadPowder Engineering Co., Ltd. is a prominent manufacturer specializing in advanced material handling solutions, particularly pneumatic conveying systems. This article delves into the operation process and working principle of a specialized system designed for the efficient transportation of potassium carbonate fertilizer materials. The system is engineered to meet the stringent requirements of modern fertilizer production, ensuring high throughput, minimal material loss, and optimal environmental control. By leveraging compressed air as the primary transport medium, the system offers a reliable and flexible solution for moving bulk materials over varying distances and heights.
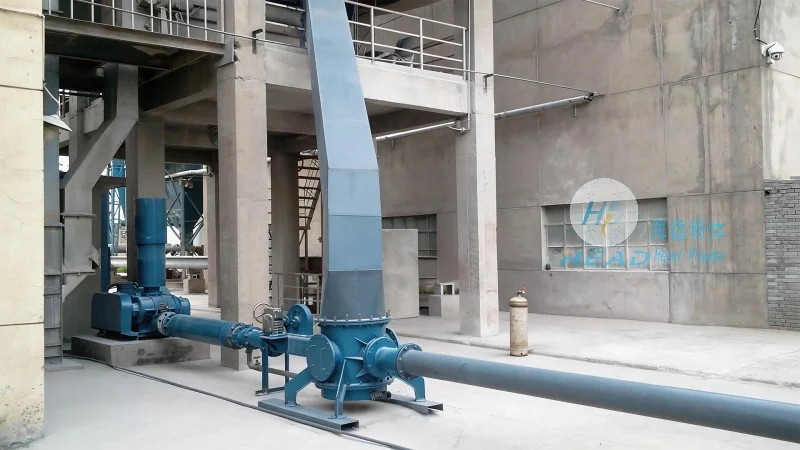
The pneumatic conveying system for potassium carbonate fertilizer materials comprises several critical components that work in concert to achieve seamless material transport. The primary components include a bulk material hopper, a rotary airlock valve, a pneumatic conveying pipeline, a dust filtration unit, and a discharge hopper. The working principle is based on the use of compressed air to create a flow of material through the pipeline. When the material is released from the hopper into the rotary valve, it is metered and then drawn into the conveying line by the airflow generated by the air compressor. The compressed air, typically operating at a pressure range of 0.5 to 0.8 megapascals (MPa), propels the material particles through the pipeline, forming a dense phase flow characterized by a high solid-to-gas ratio. This dense phase flow minimizes material degradation and reduces pressure drop along the pipeline, ensuring efficient transport. The dust filter is essential for maintaining air quality and preventing dust contamination, while the discharge hopper collects the material at the destination point, ready for further processing or packaging.
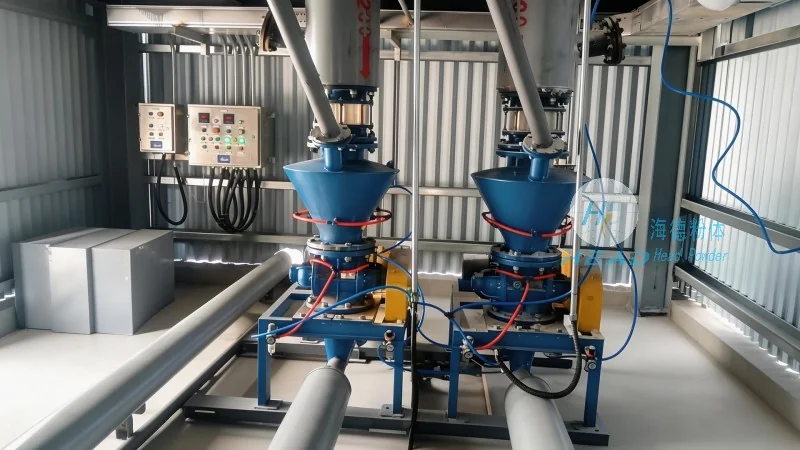
The operation process of the system involves a series of sequential steps that ensure consistent and reliable material handling. Initially, the potassium carbonate fertilizer is loaded into the bulk hopper, where it is stored until required. The rotary airlock valve then regulates the flow of material into the conveying line, controlling the quantity and rate of discharge. The air compressor provides the necessary compressed air, which is directed into the conveying line through a network of pipes and fittings. As the compressed air flows, it creates a negative pressure zone that pulls the material particles into the line, forming a continuous stream. The system is equipped with pressure sensors and control panels that monitor key parameters such as pressure, flow rate, and material level, allowing for real-time adjustments to maintain optimal performance. The material travels through the pipeline to the discharge hopper, where it is collected and then transferred to the next stage of the production process. The entire process is automated, reducing the need for manual intervention and minimizing the risk of material spillage or contamination.
The pneumatic conveying system for potassium carbonate fertilizer materials offers several distinct advantages over traditional material handling methods. It provides a dust-free and hygienic environment, which is crucial for maintaining the quality and purity of fertilizer products. The system is also highly flexible, enabling easy integration with existing production lines and the ability to transport materials over long distances without intermediate storage. Additionally, the system is energy-efficient, as it utilizes compressed air to transport material, reducing reliance on mechanical conveyors and associated maintenance costs. The reliability and efficiency of the system make it an ideal solution for high-volume material handling in the agricultural and chemical industries. It is commonly used in fertilizer manufacturing plants to transport potassium carbonate from storage silos to processing units, or from processing units to packaging lines. The system's ability to handle bulk materials with minimal degradation and loss makes it a preferred choice for industries where material quality is paramount.
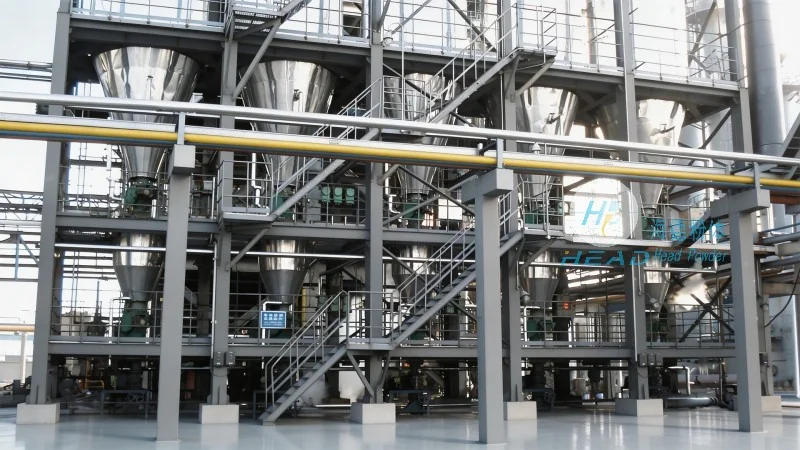
Proper maintenance is essential to ensure the long-term reliability and efficiency of the pneumatic conveying system. Regular inspection of the rotary valve and airlock components is crucial to prevent material blockages and ensure consistent flow rates. The air compressor and dust filter should be checked periodically to maintain optimal performance and prevent air leaks or dust accumulation. The conveying pipeline should be inspected for any signs of wear or damage, as even small leaks can significantly impact system efficiency. By following a regular maintenance schedule, the system can operate at peak performance, minimizing downtime and maximizing material throughput. Additionally, performance optimization techniques such as adjusting the air pressure, modifying the material feed rate, or using different pipeline configurations can be employed to enhance the system's efficiency and adapt to varying production demands.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top