HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of pneumatic conveying systems tailored for the glass manufacturing industry. These systems are engineered to efficiently transport glass raw materials, such as sand, soda ash, limestone, and other additives, from storage to processing equipment with precision and reliability. This article explores the fundamental principles behind pneumatic conveying technology and highlights the key characteristics of its application in various glass production environments.
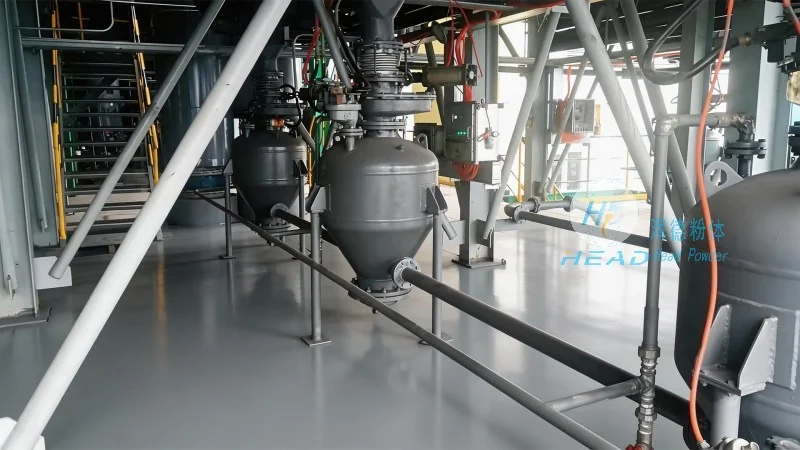
The fundamental principle of pneumatic conveying involves the use of compressed air or gas to move bulk materials through a pipeline. In the context of glass raw materials, this technology enables the transport of powders and granules without the need for mechanical components like belts or buckets. The system typically operates by creating a pressure differential between the inlet and outlet of the pipeline, which propels the material forward. There are two primary modes of operation: suction (or vacuum) conveying and pressure conveying. Suction systems draw material from a hopper or storage bin using a vacuum created by a fan or blower, while pressure systems force material through the pipeline using compressed air from a separate source. Both methods are widely used in glass production, with the choice depending on factors like material properties, distance, and system layout.
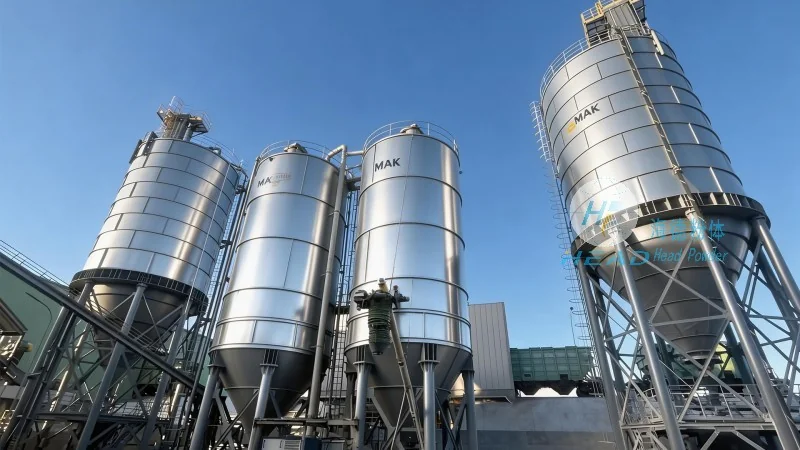
When applied in glass manufacturing facilities, pneumatic conveying systems exhibit several distinct characteristics that make them ideal for handling glass raw materials. First, these systems offer a high degree of cleanliness and contamination control. Since the material is enclosed within a pipeline, there is minimal exposure to the environment, reducing the risk of dust contamination or cross-contamination between different raw materials. This is particularly important in glass production, where even small amounts of impurities can affect the final product's quality and optical properties. Second, pneumatic conveying systems provide excellent scalability and flexibility. They can be easily integrated into existing production lines or expanded to accommodate increased production volumes. The modular design allows for the addition of new conveying lines or the modification of existing ones without major disruptions to the facility. Third, these systems are energy-efficient and cost-effective compared to traditional methods like bucket elevators or belt conveyors. The absence of moving parts reduces maintenance requirements and operational costs, while the ability to transport materials over longer distances with fewer components lowers overall system costs.
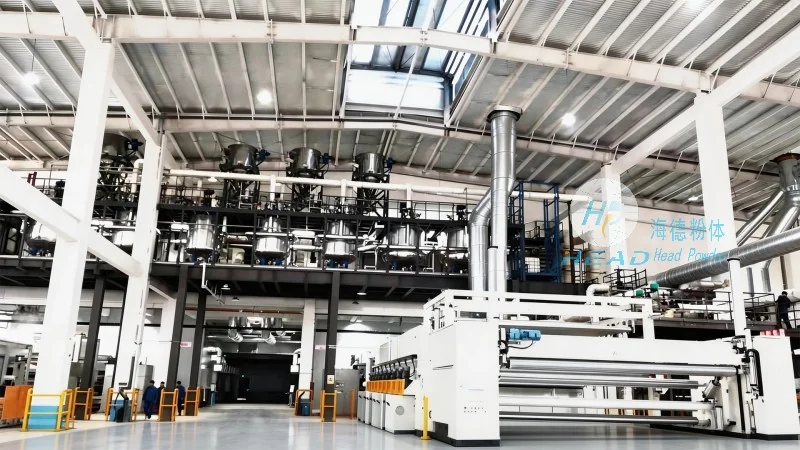
Pneumatic conveying systems are utilized in a variety of working scenarios within glass production plants. One common application is the transfer of raw materials from bulk storage silos or hoppers to the melting furnace. In this scenario, the system ensures a continuous and controlled feed of materials to the furnace, which is critical for maintaining consistent melting temperatures and glass composition. Another application is the transport of additives, such as colorants or fining agents, from storage to the mixing and batching areas. The precision of pneumatic conveying allows for accurate dosing of these additives, ensuring uniform color and clarity in the final glass products. Additionally, these systems are used in quality control and sampling processes, where small quantities of raw materials are conveyed to testing equipment for analysis. The ability to handle fine powders and granules with minimal degradation makes pneumatic conveying suitable for these applications. Finally, in larger glass manufacturing facilities, multiple pneumatic conveying lines may be used to distribute raw materials to different production lines or processing units, such as grinding, refining, or forming equipment. This integrated approach enhances operational efficiency and reduces material handling time.
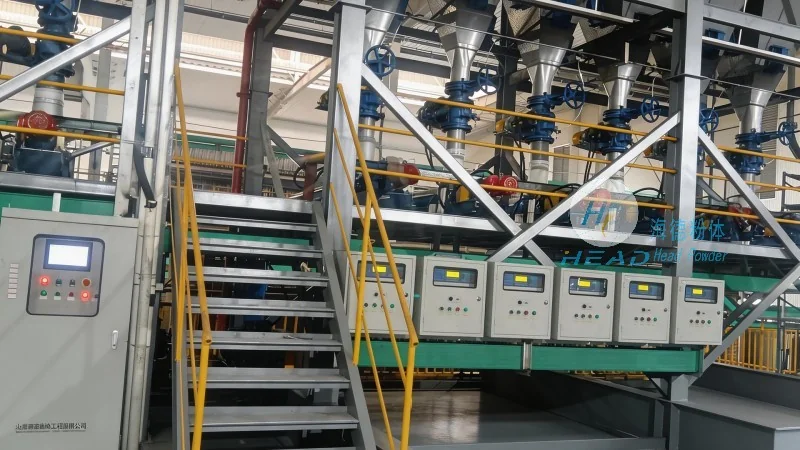
Implementing pneumatic conveying systems for glass raw materials offers several advantages, including improved process control, reduced labor costs, and enhanced safety. The systems allow for automated material handling, minimizing the need for manual labor in transporting raw materials. This not only improves efficiency but also reduces the risk of workplace accidents associated with manual handling of bulk materials. However, there are also considerations to keep in mind when selecting and implementing such systems. For instance, the choice of conveying mode (suction or pressure) depends on the specific characteristics of the raw materials, such as their density, moisture content, and flowability. Additionally, the design of the pipeline system, including the size and layout of the pipes, must be optimized to ensure efficient material transport and minimize pressure losses. Proper maintenance of the air compressors and filters is also essential to ensure the long-term performance and reliability of the system. HeadPowder, with its expertise in industrial material handling, provides comprehensive solutions that address these considerations, ensuring that clients receive systems tailored to their specific glass production needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top