At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and implementation of advanced material handling systems, including air-driven conveyor lines for specialized chemical products such as magnesium sulfate heptahydrate. This article provides a detailed overview of the operation process and working principle of our air-driven magnesium sulfate heptahydrate conveyor line, highlighting key components, operational steps, and the technical foundation that ensures efficient and reliable material transport.
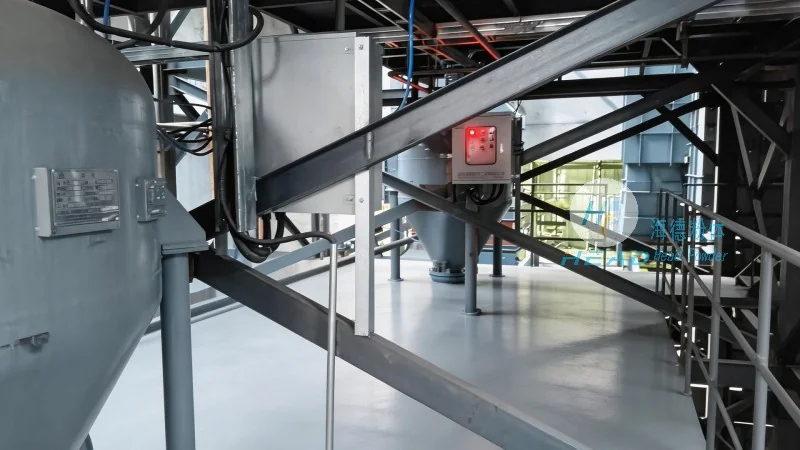
The air-driven conveyor line for magnesium sulfate heptahydrate is engineered to transport bulk materials through a pneumatic system, leveraging compressed air to move the product from the source to the destination. This system is particularly suitable for handling fine or powdery materials like magnesium sulfate heptahydrate, which require gentle handling to prevent degradation or caking. The design incorporates several critical components, including a material hopper, airlock feeders, a conveying pipe network, and a discharge unit, all working in tandem to achieve seamless material flow.
Each component of the air-driven conveyor line plays a vital role in the overall operation. The material hopper serves as the initial storage and feeding point, where the magnesium sulfate heptahydrate is loaded and held before being introduced into the system. The airlock feeder is a crucial element that controls the flow of material into the conveying pipe, preventing air leakage and ensuring a consistent feed rate. This component typically consists of a rotary valve or a slide valve that opens and closes to allow material to pass through under controlled conditions. The conveying pipe network is the main channel through which the material is transported, often made of stainless steel or other corrosion-resistant materials to withstand the chemical properties of magnesium sulfate heptahydrate. The pipe network may include bends, elbows, and straight sections, with appropriate support structures to maintain alignment and prevent sagging. Finally, the discharge unit is responsible for releasing the material from the conveying system, usually into a storage bin or a processing unit. This unit may include a rotary valve or a gate valve to regulate the discharge rate and prevent backflow.
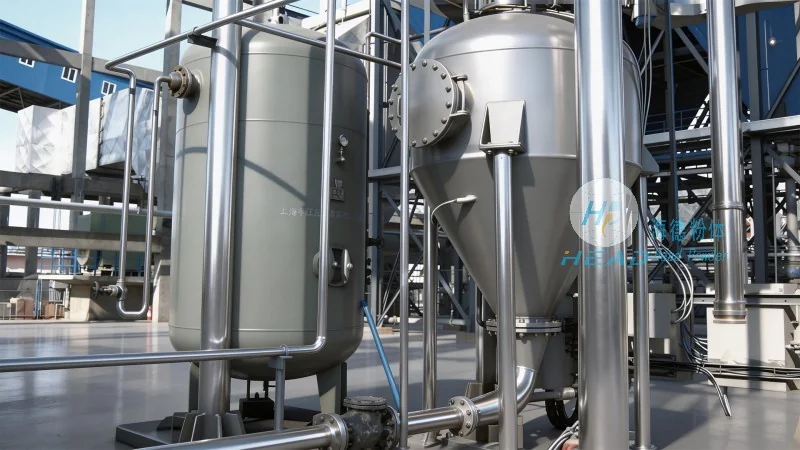
The operation of the air-driven magnesium sulfate heptahydrate conveyor line follows a systematic sequence of steps to ensure efficient material transport. The process begins with the loading of the material into the hopper. The material is then fed into the airlock feeder, which regulates the flow rate and prevents the material from clogging the conveying pipe. Compressed air is introduced into the conveying pipe, creating a pressure differential that propels the material forward. The material travels through the pipe network, navigating bends and changes in direction with minimal impact. At the discharge end, the material is released into the receiving container. The entire process is monitored and controlled by a system of sensors and control valves, which adjust the air pressure and feed rate as needed to maintain optimal performance.
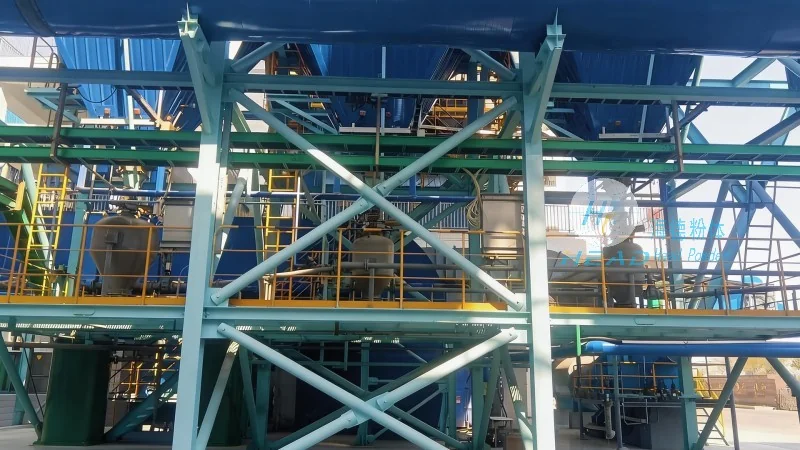
The working principle of the air-driven conveyor line is based on the fundamental physics of pneumatic conveying. Compressed air is used to create a low-pressure environment within the conveying pipe, which draws the material particles into the flow. The air and material mixture moves through the pipe at a velocity sufficient to keep the particles suspended and prevent them from settling or caking. The key to efficient pneumatic conveying is maintaining the correct air-to-material ratio, which balances the velocity of the air with the size and density of the material particles. This ratio ensures that the material is transported without excessive pressure drop or energy consumption. The system also incorporates features such as pulse-jet cleaning to prevent material buildup on the pipe walls, and pressure relief valves to protect the system from overpressure conditions. These mechanisms work together to ensure the consistent and reliable operation of the conveyor line.
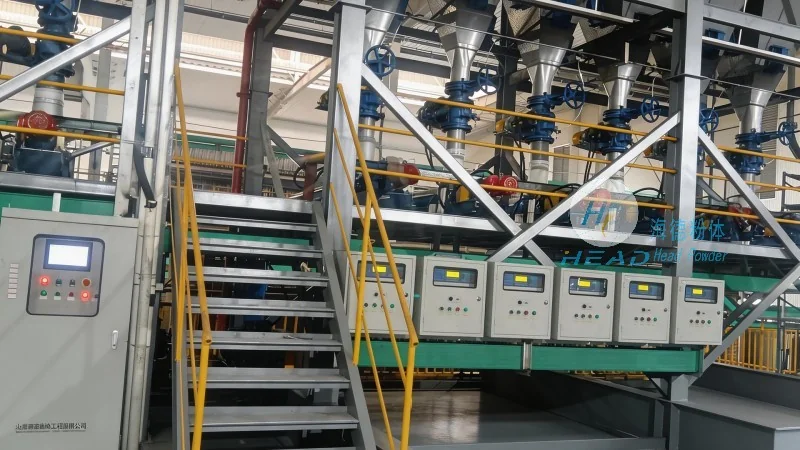
Compared to traditional mechanical conveyor systems, the air-driven conveyor line offers several advantages for handling magnesium sulfate heptahydrate. First, it provides gentle handling of the material, reducing the risk of degradation or caking, which is critical for maintaining the quality of the product. Second, the system is highly flexible, allowing for changes in the conveying route or capacity without major modifications. Third, it is relatively low in maintenance, as there are fewer moving parts compared to mechanical systems. Fourth, the air-driven system is more hygienic and easier to clean, which is important for pharmaceutical or food-grade applications. Finally, the system is energy-efficient, as it uses compressed air to transport the material, which can be generated from the plant's existing compressed air supply.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of material handling systems, specializing in the design and implementation of customized solutions for various industries. Our company is located in Shandong, China, and we have extensive experience in the chemical, pharmaceutical, and food processing sectors. We provide comprehensive services, including system design, manufacturing, installation, and after-sales support, to ensure that our clients receive the best possible solution for their material handling needs. For more information about our air-driven magnesium sulfate heptahydrate conveyor line or other products, please contact us at our headquarters in Shandong, China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top