Alumina sulphate, a vital chemical utilized in water treatment, paper production, and various industrial processes, often necessitates efficient and reliable transportation methods. Pneumatic conveying, a technology that employs air or gas to transport bulk powders such as alumina sulphate, provides a solution that enhances process efficiency and safety. This article delves into the working principles of a pneumatic conveying system specifically designed for alumina sulphate, highlighting its key components and operational mechanisms.
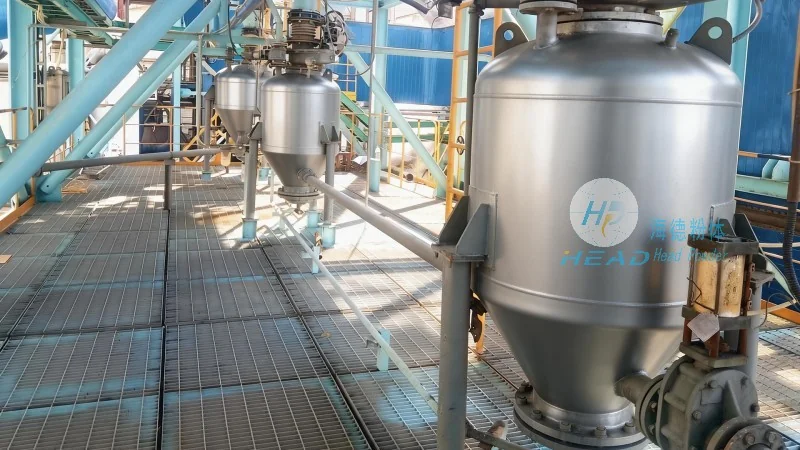
HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring efficient material transport. HeadPowder's expertise lies in creating customized solutions that meet the unique demands of clients, ensuring optimal performance and durability in demanding operational environments.
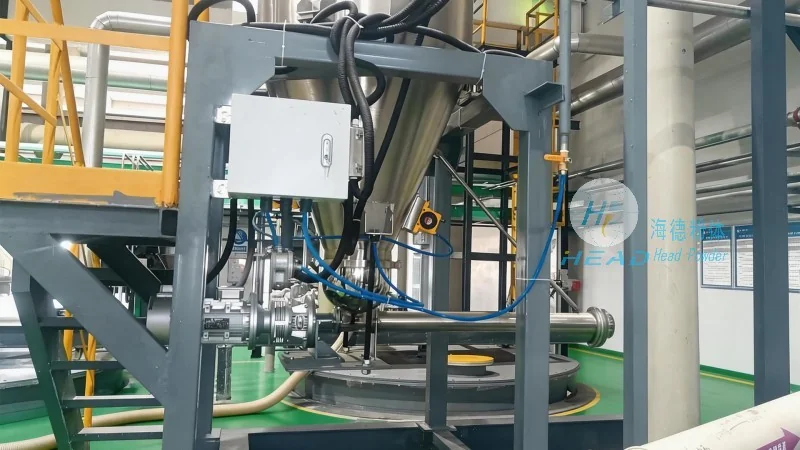
The core of a pneumatic conveying system for alumina sulphate involves the use of a compressor to generate airflow, which then propels the powder particles through a pipeline. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The process begins when the alumina sulphate is fed into the hopper, where it is then transferred to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the amount of powder released into the conveying line. As the compressed air is introduced into the line, it creates a low-pressure zone that draws the powder particles into the airflow, forming a dense phase or dilute phase conveying system depending on the system design and operational parameters.
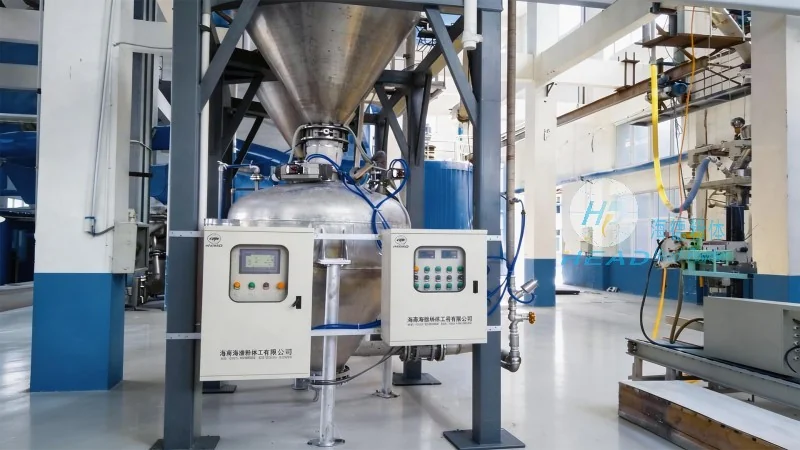
Pneumatic conveying systems offer several advantages when handling alumina sulphate. These include the ability to transport materials over long distances without the need for multiple transfer points, reducing the risk of contamination and material loss. The enclosed system also minimizes dust emissions, enhancing workplace safety and compliance with environmental regulations. Additionally, pneumatic conveying allows for precise control over the flow rate and pressure, ensuring consistent material delivery to downstream processes. The flexibility of the system enables easy integration with existing production lines, and its compact design saves valuable floor space in industrial facilities.
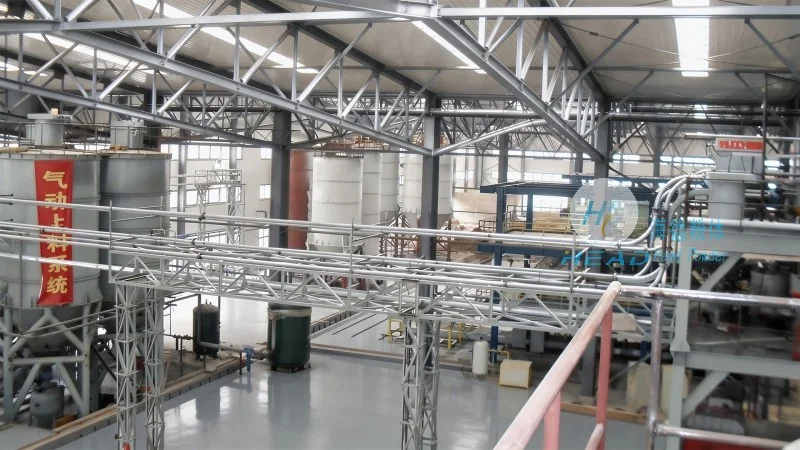
HeadPowder Engineering Co., Ltd. provides comprehensive support for clients seeking pneumatic conveying solutions for alumina sulphate applications. The company's team of experts works closely with clients to understand their specific requirements, from material characteristics to operational constraints, and designs a tailored system that maximizes efficiency and reliability. HeadPowder's manufacturing facilities in Shandong, China, ensure high-quality production standards, with rigorous testing and quality control measures in place to guarantee the performance and durability of each system. By choosing HeadPowder, clients benefit from a reliable partner that delivers innovative, cost-effective solutions tailored to their unique needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top