Diatomite, a natural sedimentary rock composed of fossilized diatoms, is widely used in various industrial applications due to its unique properties such as high porosity, lightweight, and excellent filtration capabilities. When it comes to transporting diatomite powder, pneumatic conveying systems offer an efficient and reliable solution. This article aims to explain the concept of diatomite pneumatic conveying and delve into the fundamental working principles of powder handling systems designed for such materials.
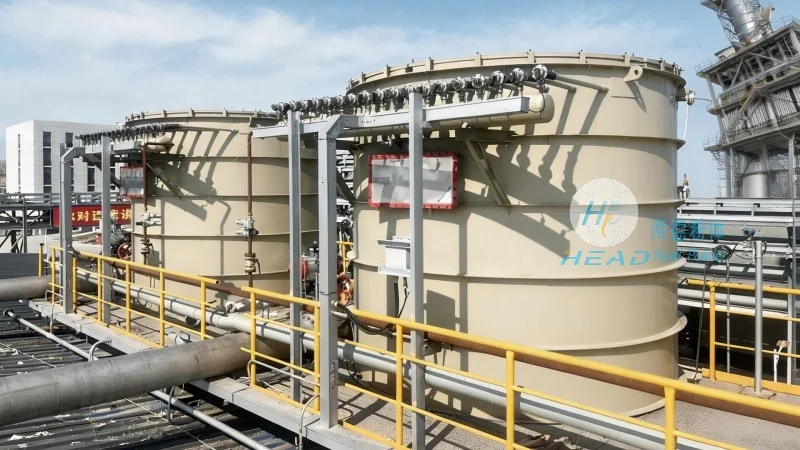
Pneumatic conveying, also known as powder handling systems, utilizes air or gas to transport bulk materials like diatomite from one location to another. The system operates by creating a pressure differential or using vacuum to move the material through a pipeline. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material forward, while vacuum systems employ a vacuum to draw the material into the pipeline. Both methods are effective for diatomite, which is often handled in bulk due to its low density and fine particle size.
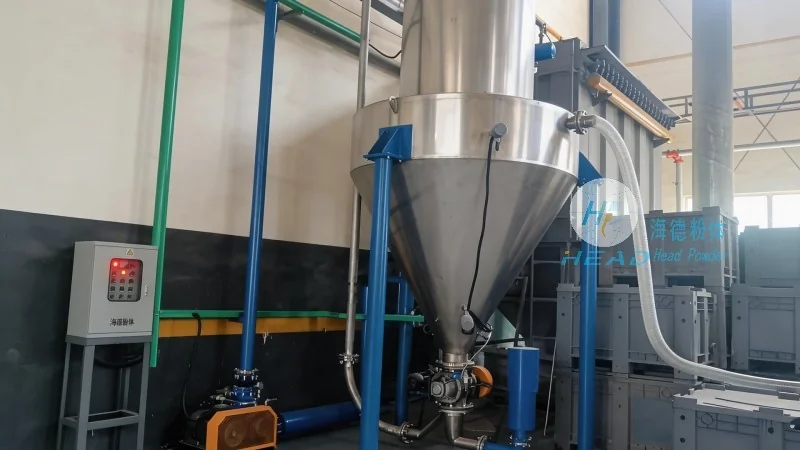
The core of a diatomite pneumatic conveying system involves several key components that work in tandem to ensure smooth material transport. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. A blower or compressor provides the necessary air pressure to move the diatomite particles. As the air and powder mixture travels through the pipeline, the diatomite is suspended and carried to the destination point. At the receiving end, a separator or cyclone separates the powder from the air, allowing the diatomite to be collected in a storage bin or processing unit. The air, now clean, is either recirculated or vented to the atmosphere, depending on the system design. This closed-loop or open-loop system ensures efficient and dust-free transport of diatomite, minimizing environmental impact and maintaining product quality.
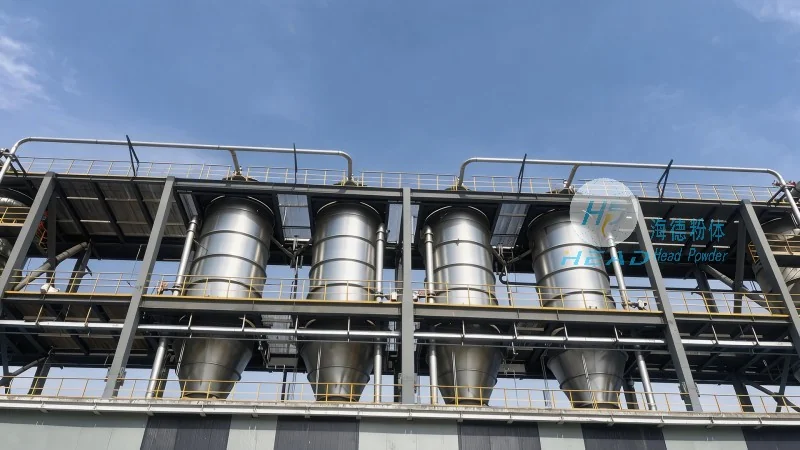
Several critical components are integral to the operation of a diatomite pneumatic conveying system. The feeder or hopper is responsible for controlling the flow rate of the diatomite, ensuring a consistent and controlled feed into the system. The blower or compressor generates the air pressure required to move the material. The pipeline, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and prevent material buildup. The separator or cyclone is essential for separating the diatomite from the air, preventing clogging and maintaining system efficiency. Additionally, filters and cleaning mechanisms are often included to ensure the air is free from dust particles, which is crucial for maintaining air quality and preventing equipment damage.
Implementing a pneumatic conveying system for diatomite offers numerous advantages over traditional methods such as bucket elevators or belt conveyors. One of the primary benefits is the ability to transport diatomite in a dust-free environment, which enhances workplace safety and product purity. The system also allows for flexible and compact installation, as the pipeline can be routed around obstacles and in tight spaces. Furthermore, pneumatic conveying systems are highly efficient in terms of energy consumption and can handle a wide range of particle sizes and moisture contents. The closed-loop design reduces material loss and environmental contamination, making it an environmentally friendly option for diatomite transport.
Diatomite pneumatic conveying systems are widely used in various industrial sectors where diatomite is a key raw material. In the filtration industry, diatomite is used to produce filter media for water treatment and industrial filtration processes. The pneumatic conveying system ensures that the diatomite is transported to the filtration equipment without contamination, maintaining the quality of the final product. In the food and beverage industry, diatomite is used as a filtration aid and clarifying agent. The system's ability to handle fine powders and maintain hygiene standards makes it ideal for these applications. Additionally, in the chemical and pharmaceutical industries, diatomite is used as a filler or adsorbent, and the pneumatic conveying system ensures that the material is transported safely and efficiently to the processing units.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling systems, including pneumatic conveying solutions for diatomite and other bulk materials. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the industry. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest technology and skilled personnel. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients, ensuring optimal performance and reliability. The company's commitment to customer satisfaction and product excellence has earned it a reputation for delivering high-quality solutions that meet the stringent requirements of various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top