Coffee powder pneumatic conveying is a specialized method used in the coffee processing and distribution industry to transport coffee grounds or other fine powders efficiently and hygienically. This technology is crucial for maintaining product quality and ensuring smooth operations in coffee production facilities. The following article provides an in-depth look at the working principles of such systems, highlighting how they operate and the benefits they offer.
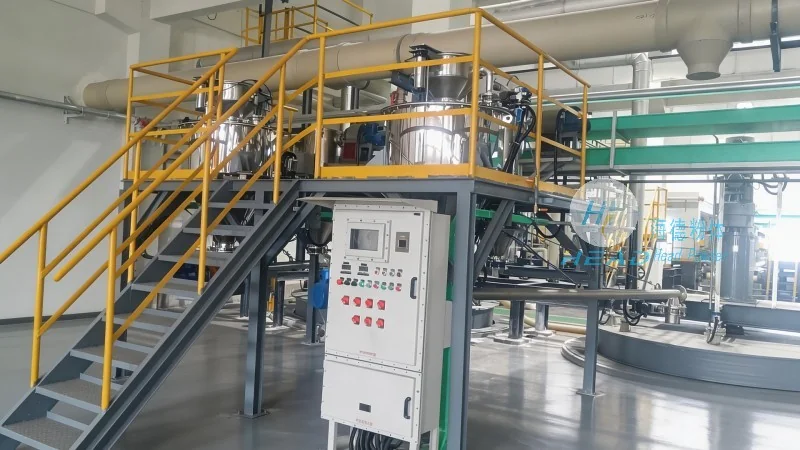
Pneumatic conveying systems for coffee powders are designed to move dry, fine particles like coffee grounds from one location to another using air pressure. Unlike traditional mechanical conveyors, which rely on physical components like belts or screws, pneumatic systems utilize air to transport the material. This method is particularly advantageous for coffee powders due to their delicate nature and the need for a clean, dust-free environment. The system typically consists of a hopper, a conveyor line, and a receiver, all connected by a network of pipes. The coffee powder is fed into the hopper, where it is then drawn into the conveyor line by a vacuum or pressure source. The air, carrying the coffee powder particles, travels through the pipes to the destination, where the powder is separated from the air and collected in the receiver.
The core of a coffee powder pneumatic conveying system is the air flow mechanism that propels the powder. There are two main types of pneumatic conveying systems: pressure and vacuum. Pressure systems use compressed air to push the material through the pipes, while vacuum systems use a vacuum to pull the material. For coffee powders, vacuum systems are often preferred as they are gentler on the product and can handle longer distances more effectively. The system operates by creating a pressure differential between the hopper and the receiver. The vacuum pump or compressor generates a low-pressure area in the receiver, causing the coffee powder to be drawn into the conveyor line. As the air flows through the pipes, it carries the coffee grounds along, maintaining a consistent flow rate. The velocity of the air is carefully controlled to ensure that the coffee powder particles are not damaged or agglomerated during transport.
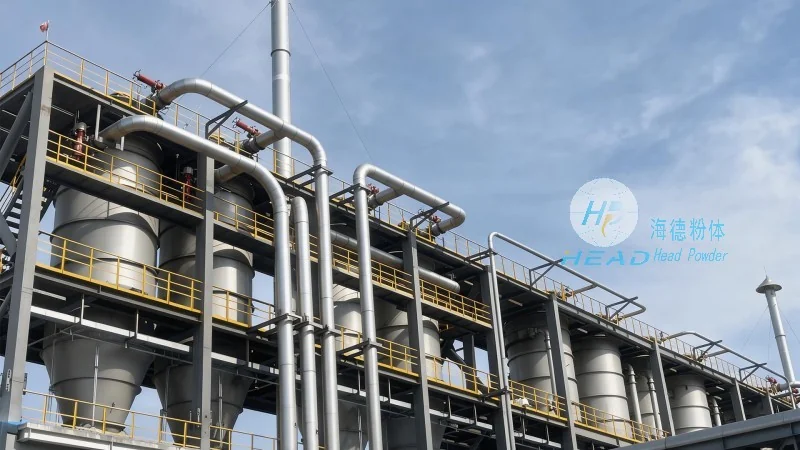
Several key components work together to ensure the efficient operation of a coffee powder pneumatic conveying system. The hopper is the initial container where the coffee powder is stored before being fed into the system. It is designed to hold a sufficient quantity of material and to provide a smooth, controlled flow into the conveyor line. The conveyor line itself is made of materials that are resistant to the coffee powder and to the air used in the system, such as stainless steel or food-grade plastic. The pipes are typically arranged in a straight or slightly curved path to minimize pressure loss and to ensure the coffee powder reaches the receiver without clogging. The receiver is the final container where the coffee powder is collected after being separated from the air. It is equipped with a filter or cyclone to separate the powder from the air, preventing dust from escaping into the environment. The control system, which includes sensors and valves, monitors the flow rate and pressure, ensuring that the system operates within optimal parameters. This system allows for precise control over the amount of coffee powder being transported, which is essential for maintaining consistent product quality.
Implementing a pneumatic conveying system for coffee powders offers several benefits that enhance both the efficiency and quality of coffee processing operations. One of the primary advantages is the ability to maintain a clean and hygienic environment. Since the system is enclosed, there is no risk of contamination from external sources, which is critical for coffee products that are consumed directly. The enclosed design also reduces dust emissions, improving workplace safety and compliance with environmental regulations. Another benefit is the gentleness of the conveying process. Unlike mechanical conveyors that can cause friction and damage to the coffee powder particles, pneumatic systems use air to move the material, preserving the texture and flavor of the coffee grounds. This is particularly important for specialty coffees, where the quality of the powder directly impacts the final product. Additionally, pneumatic conveying systems are highly flexible and can be easily integrated into existing production lines. They can transport coffee powder over long distances and can be adapted to different production volumes, making them suitable for both small-scale and large-scale coffee processing facilities. The system also offers cost savings in the long run, as it reduces the need for manual handling and minimizes product loss due to spillage or clogging.
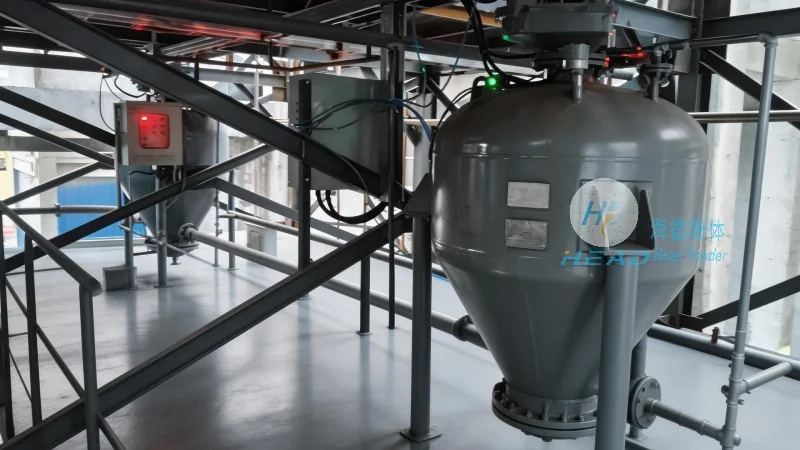
Coffee powder pneumatic conveying systems are widely used in various stages of coffee processing and distribution. In the production phase, these systems are used to transport freshly ground coffee from the roasting machine to the packaging area. This ensures that the coffee powder is handled quickly and efficiently, reducing the risk of oxidation and maintaining its freshness. During the packaging process, the system can transport the coffee powder from the storage silos to the filling machines, ensuring a consistent and hygienic flow of material. In the distribution phase, pneumatic conveying systems are used to move coffee powder from the production facility to the warehouse or to the final customers. This method is particularly useful for large-scale distribution, as it allows for the efficient transport of large quantities of coffee powder without the need for manual handling. The systems are also used in coffee roasting plants to convey raw coffee beans to the roasting machines and to transport roasted beans to the grinding and packaging stages. Overall, the applications of coffee powder pneumatic conveying systems are diverse and essential for maintaining the quality and efficiency of coffee processing operations.
In conclusion, coffee powder pneumatic conveying is a vital technology in the coffee industry, providing an efficient and hygienic method for transporting coffee grounds and other fine powders. The working principles of these systems, which rely on air pressure to move the material, offer several advantages over traditional mechanical conveyors. By maintaining a clean and enclosed environment, preserving the quality of the coffee powder, and offering flexibility in operation, pneumatic conveying systems enhance the overall efficiency and quality of coffee processing operations. As the coffee industry continues to grow and demand for high-quality coffee products increases, the use of advanced pneumatic conveying systems will become even more critical. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in designing and manufacturing such systems, providing coffee processing facilities with reliable and effective solutions for their powder handling needs. With their expertise in the field, these companies help ensure that coffee powders are transported safely and efficiently, contributing to the success of coffee production and distribution worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top