Multi-hopper pneumatic conveying systems represent a sophisticated approach to material handling, offering efficient and flexible solutions for transporting bulk materials over varying distances. This technology is particularly valuable in industries where dust control, material integrity, and system reliability are paramount. The operation and working principles of such systems are integral to understanding their effectiveness and application in diverse industrial settings.
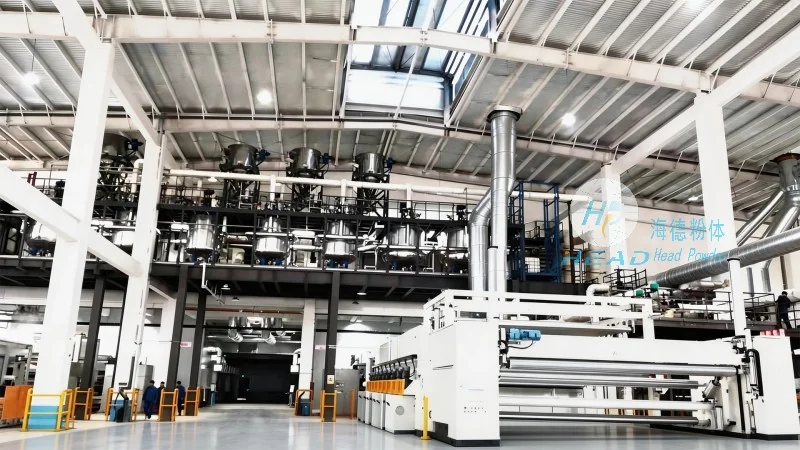
At the core of multi-hopper pneumatic conveying systems is the ability to handle multiple material streams simultaneously or sequentially. These systems typically consist of several hoppers, each dedicated to a specific material, connected to a central conveying pipeline. The design allows for the independent or combined transport of different materials, enhancing operational flexibility. The system integrates components such as feeders, airlocks, and a conveying pipeline, all working in tandem to ensure smooth material movement. The choice of system configuration—whether pressure or vacuum-based—depends on the specific material characteristics and the distance over which the material needs to be conveyed.
The effectiveness of a multi-hopper pneumatic conveying system is determined by its key components, each playing a critical role in the overall operation. The hoppers serve as storage vessels for the bulk materials, ensuring a steady supply to the system. Each hopper is equipped with a feeder, which controls the material flow into the conveying pipeline. Airlocks are installed at the discharge points of the hoppers to prevent backflow and maintain system pressure. The conveying pipeline transports the material-air mixture from the hoppers to the destination point, such as a silo or processing unit. A control system manages the operation of all components, ensuring precise control over material flow rates and air pressure. The system may also include filters and cyclones to separate the material from the air, maintaining air quality and preventing material loss.
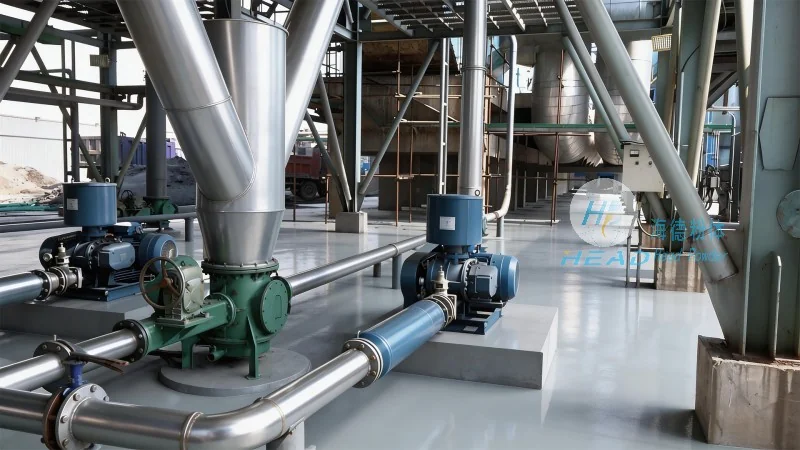
The operation of a multi-hopper pneumatic conveying system involves several sequential steps, each designed to ensure efficient material transport. The process begins with the loading of materials into the respective hoppers. Each hopper is then connected to the conveying pipeline via its feeder and airlock. The control system initiates the conveying process by adjusting the air pressure and flow rate. As air is introduced into the pipeline, it creates a flow that pulls the material from the hoppers. The material is then transported as a slurry or dilute phase through the pipeline to the receiving vessel. The system may operate in either continuous or batch mode, depending on the operational requirements. In continuous operation, materials are fed continuously, while in batch operation, the system is activated for a specific duration to transport a set amount of material. The control system monitors parameters such as pressure, flow rate, and material level, making adjustments as needed to maintain optimal performance.
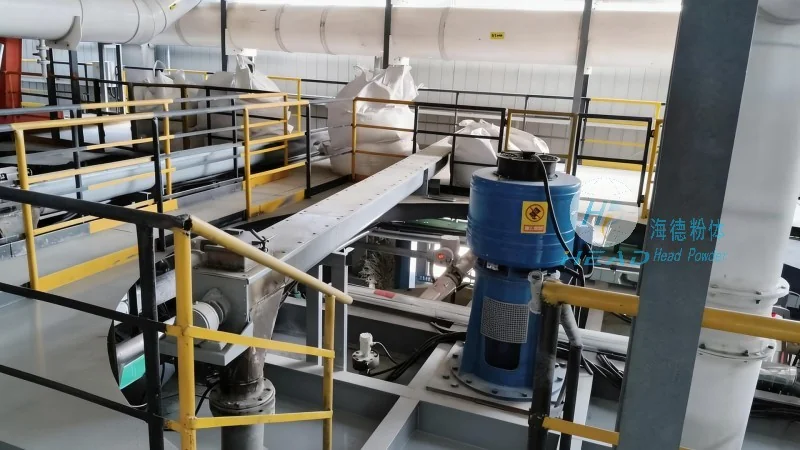
The working principle of multi-hopper pneumatic conveying systems is based on the principles of fluid dynamics and material transport. The system utilizes compressed air or vacuum to create a flow that moves the material through the pipeline. In pressure systems, air is pumped into the conveying pipeline, creating a positive pressure that pushes the material forward. The material is suspended in the air stream, moving as a dilute phase. In vacuum systems, a vacuum is created at the receiving end, pulling the material and air through the pipeline. The material is again suspended in the air stream, moving as a dilute phase. The key to efficient operation is maintaining the correct air-to-material ratio, which ensures that the material is fully suspended and transported without clogging or degradation. The system's design, including the size of the pipeline and the speed of the air flow, is critical in achieving this balance. The multi-hopper configuration allows for the independent control of each material stream, ensuring that the air-to-material ratio can be optimized for each material's specific characteristics.
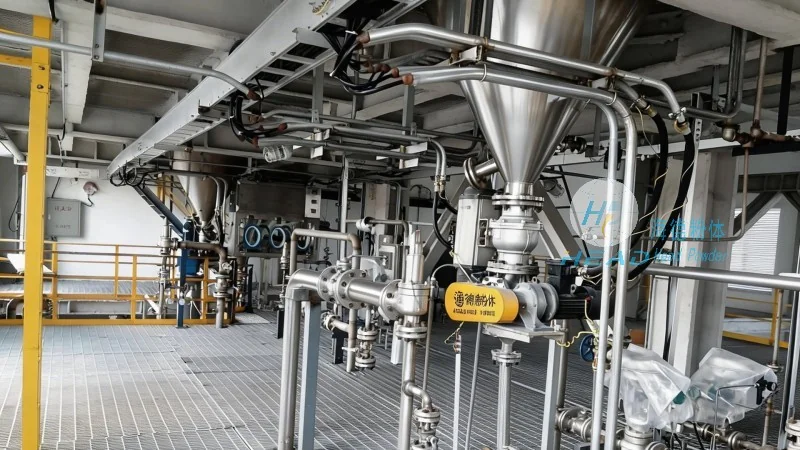
Multi-hopper pneumatic conveying systems offer several advantages that make them suitable for a wide range of industrial applications. These systems provide efficient and dust-free material handling, which is essential in industries such as food, pharmaceuticals, and chemicals where material purity is critical. The ability to handle multiple materials simultaneously enhances operational flexibility, allowing for the integration of different production lines. The systems are also compact and can be installed in confined spaces, making them suitable for facilities with limited floor space. Additionally, the systems are relatively low maintenance, with fewer moving parts compared to mechanical conveying systems. The applications of multi-hopper pneumatic conveying systems are diverse, including the transport of powders, granules, and bulk materials in industries such as cement, mining, and agriculture. The systems are also used in the food and beverage industry for the transport of ingredients and finished products.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions, specializing in the design, manufacturing, and installation of multi-hopper pneumatic conveying systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the industry, offering customized solutions tailored to the specific needs of its clients. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest technology and equipment. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their operational requirements and develop solutions that meet their performance and budgetary constraints. The company adheres to international quality standards and provides comprehensive after-sales support, ensuring that its systems operate at peak efficiency throughout their service life. HeadPowder's expertise in multi-hopper pneumatic conveying systems has enabled it to serve a wide range of industries, including chemical, food, pharmaceutical, and mining, helping clients improve their material handling processes and enhance overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top