Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for industrial applications. With a focus on efficiency and reliability, the company has established itself as a leading provider in the field, particularly for handling bulk materials like soda ash. Headquartered in Shandong, China, headpowder leverages years of industry experience to deliver customized solutions that meet the unique demands of various industrial sectors.
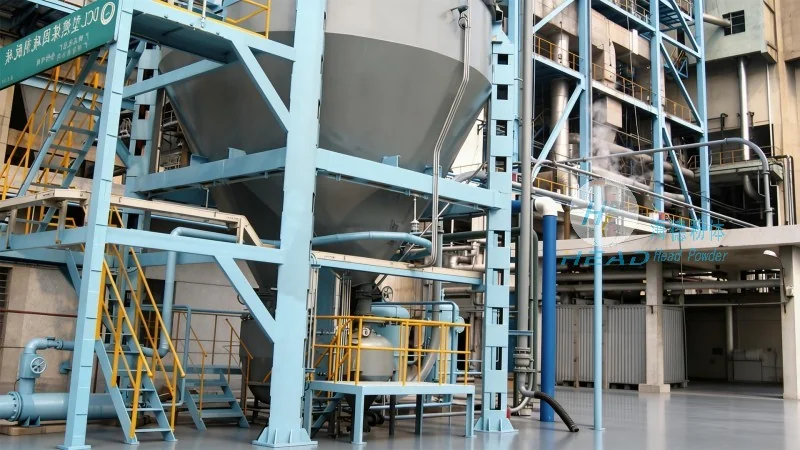
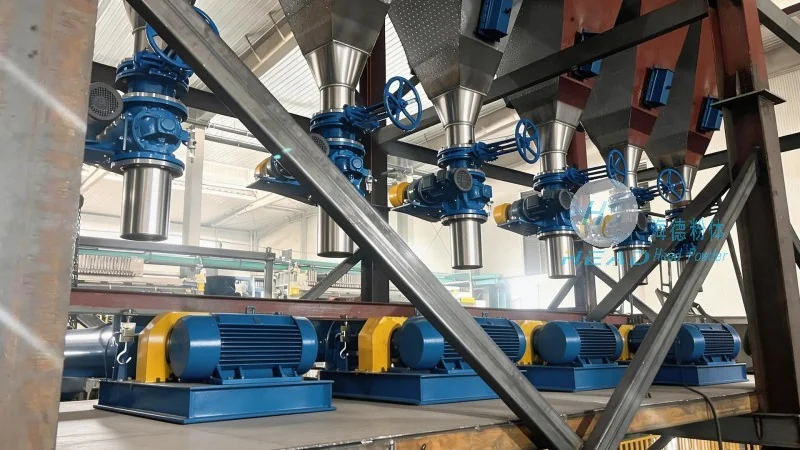
Pneumatic conveying systems operate on the fundamental principle of transporting bulk materials through a pipeline using a gas stream, typically air or other gases. The process involves creating a pressure differential between the inlet and outlet of the system, which propels the material along the pipeline. In a typical setup, a material is introduced into a hopper or feeder, where it is then entrained by the moving gas stream. The gas, often under positive or negative pressure, carries the material through the pipeline to the discharge point. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency. The system's effectiveness depends on several factors, including the material's properties (such as particle size, density, and flowability), the gas velocity, and the system's pressure and configuration.
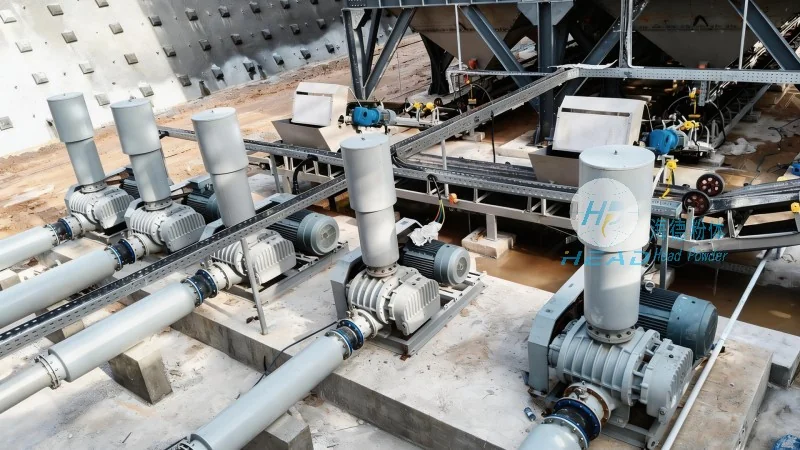
Soda ash, also known as sodium carbonate, is a widely used industrial chemical in sectors like glass manufacturing, chemical processing, and water treatment. The handling of soda ash presents unique challenges due to its granular nature and potential for dust generation. Pneumatic conveying systems offer an effective solution by providing a dust-free, enclosed transport method that minimizes environmental impact and ensures product integrity. In industrial settings, these systems are commonly employed in scenarios where material needs to be moved between storage silos, processing units, or packaging areas. For example, in a glass production facility, soda ash is transported from bulk storage to the furnace or mixing area, where it is used as a raw material. The working scene characteristics of such systems include high material throughput, consistent flow rates, and the ability to handle varying material loads without interruption. Additionally, the systems are designed to accommodate different pipeline lengths and layouts, making them adaptable to diverse plant configurations. The enclosed design of the conveying lines also helps in controlling dust emissions, which is crucial for maintaining a safe and compliant working environment. Furthermore, the systems can be integrated with other process equipment, such as mixers or reactors, to form a seamless material handling workflow. This integration enhances overall plant efficiency by reducing downtime and improving material transfer accuracy.
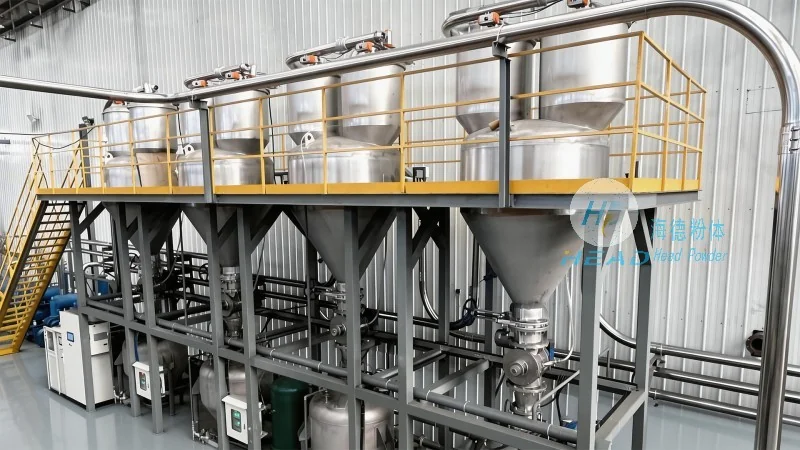
The working scene characteristics of soda ash pneumatic conveying systems are defined by several key advantages that make them suitable for demanding industrial applications. One of the primary benefits is the ability to handle large volumes of material with minimal labor input. The automated operation of the system ensures consistent and reliable transport, reducing the risk of human error and improving product quality. Another advantage is the reduced maintenance requirements compared to traditional mechanical conveying methods. Since there are no moving parts in direct contact with the material, the system experiences less wear and tear, leading to lower operational costs over time. The enclosed nature of the conveying lines also contributes to improved safety, as it prevents dust from escaping into the workplace and minimizes the risk of material spillage. In terms of operational features, the systems are designed to be flexible and adaptable. They can be configured to handle different material types and sizes, and the flow rate can be adjusted to match the specific requirements of the process. This flexibility allows plants to scale their operations without significant changes to the conveying infrastructure. Moreover, the systems are equipped with monitoring and control systems that provide real-time data on material flow and system performance. This allows operators to detect and address any issues promptly, ensuring optimal system operation. The working scene characteristics also include the ability to integrate with existing plant infrastructure, such as silos and processing equipment, without major modifications. This makes the systems a cost-effective solution for upgrading or expanding material handling capabilities. Overall, the working scene characteristics of soda ash pneumatic conveying systems highlight their role as a reliable and efficient solution for bulk material transport in industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top