Phosphates sodium pneumatic conveying systems are advanced industrial equipment designed to transport phosphate-based materials efficiently through a pressurized air or gas stream. These systems are widely used in various industrial applications, particularly in the chemical and fertilizer sectors, where the handling of bulk materials like phosphates requires reliable and safe transportation solutions. The core principle of pneumatic conveying lies in the use of air or gas to move solid particles, eliminating the need for mechanical components like belts or buckets that are common in traditional conveyor systems.
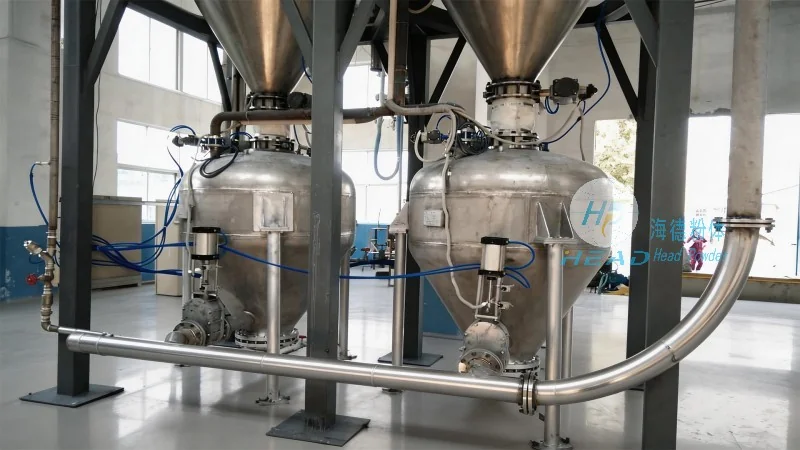
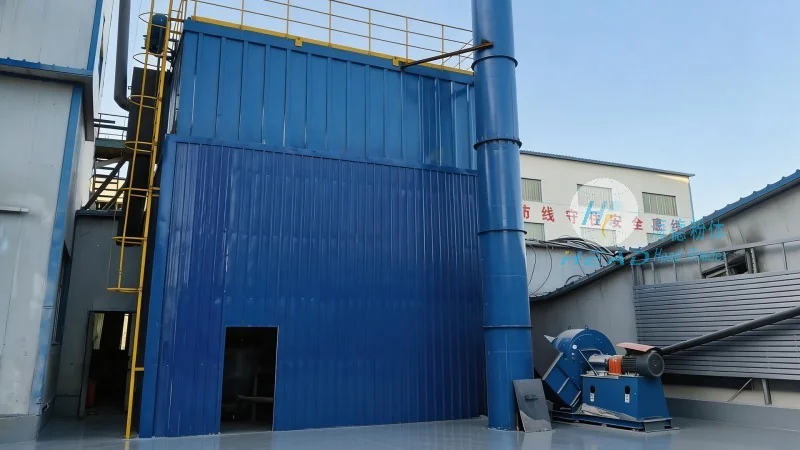
The operation of a phosphates sodium pneumatic conveying system involves several key components and processes. At its heart, the system uses a blower or compressor to generate a high-pressure air stream. This air is then directed into a hopper or feeder where the phosphate sodium material is introduced. The material is then drawn into the air stream by the pressure differential, forming a slurry or suspension that is carried through the pipeline to the destination point. The system typically includes features such as a filter or separator to remove any fine particles from the air before it is released back into the environment, ensuring compliance with environmental regulations. The design of the system is tailored to handle the specific properties of phosphates sodium, including its density, flowability, and potential moisture content, ensuring optimal performance and minimal material degradation.
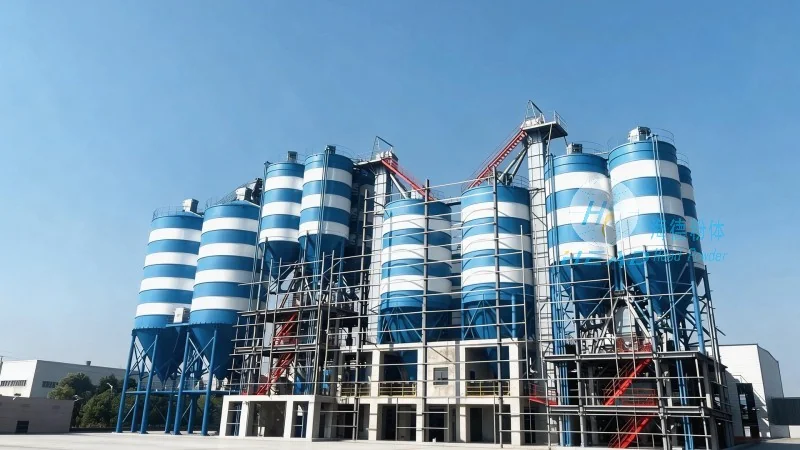
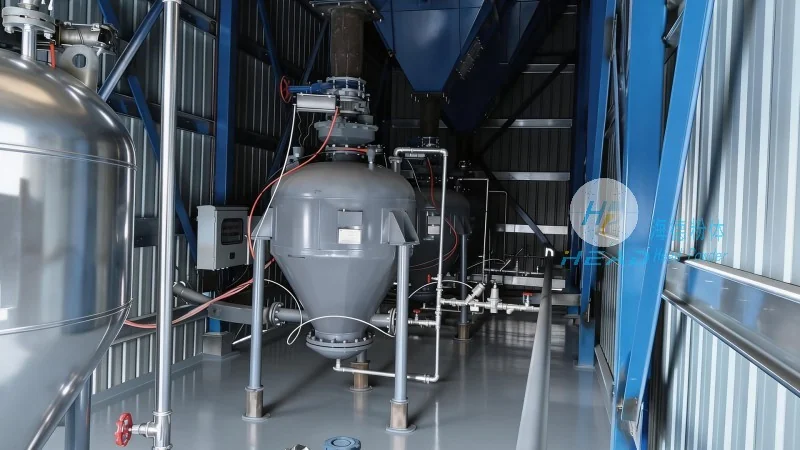
The working scene characteristics of phosphates sodium pneumatic conveying systems are crucial for understanding their application in real-world industrial settings. These systems are particularly suited for environments where the material needs to be transported over long distances or through complex layouts, such as in large-scale fertilizer production plants or chemical processing facilities. The ability to handle large volumes of material with minimal maintenance makes them ideal for continuous operation, which is essential in industries where production rates are high and downtime is costly. Additionally, the systems are designed to operate in a variety of conditions, including different ambient temperatures and humidity levels, ensuring consistent performance regardless of the operating environment. The safety features integrated into these systems, such as pressure relief valves and explosion-proof designs, are critical for handling potentially hazardous materials like phosphates sodium, which can be reactive under certain conditions.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. With a focus on phosphates sodium and other bulk materials, the company leverages years of experience in the field to provide customized solutions that meet the specific needs of its clients. The company's facilities are located in Shandong, China, where it employs a team of skilled engineers and technicians dedicated to ensuring the quality and reliability of its products. By combining innovative technology with rigorous quality control, headpowder aims to deliver systems that not only meet but exceed industry standards, providing long-term value to its customers. The company's commitment to customer support extends beyond the initial installation, with ongoing maintenance and technical assistance available to ensure the continued optimal performance of the conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top