HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for calcium carbonate applications. This article delves into the fundamental principles behind these systems and highlights key working scene characteristics that make them ideal for various industrial processes.
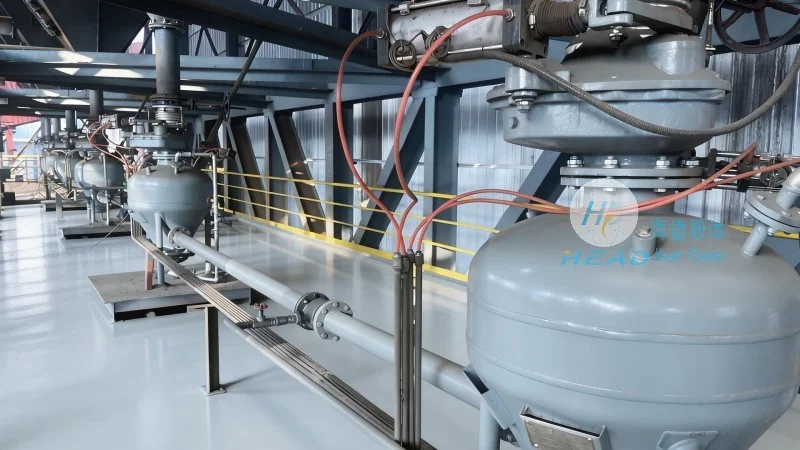
The core principle of a pneumatic conveying system involves the use of compressed air or gas to transport bulk materials like calcium carbonate from one location to another. Unlike traditional mechanical conveyors, which rely on physical contact and moving parts, pneumatic systems utilize air pressure to create a flow of material through a pipeline. The system typically consists of a hopper, a rotary valve for material feeding, a conveying line, and a receiver or discharge point. Compressed air is introduced into the system, creating a pressure differential that propels the calcium carbonate particles through the pipeline. The velocity and pressure of the air are carefully controlled to ensure efficient and reliable material transport without causing excessive wear or degradation to the product.
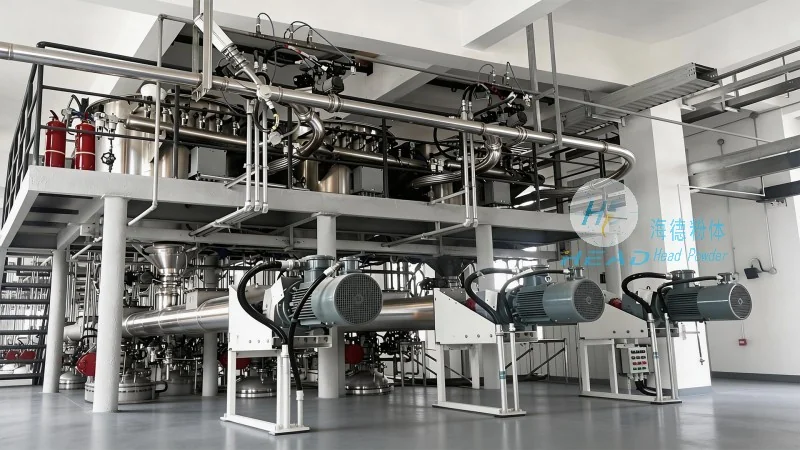
Several distinct characteristics define the working scenes where calcium carbonate pneumatic conveying systems are deployed. Firstly, these systems are highly effective in environments where traditional conveyors may face challenges, such as handling fine powders or materials with high moisture content. The air-based transport minimizes material degradation and prevents caking or blockages that are common in mechanical systems. Secondly, the flexibility of pneumatic systems allows for easy integration into existing production lines, enabling seamless material transfer between different processing stages. This adaptability is particularly valuable in manufacturing facilities where space constraints or layout changes are frequent. Thirdly, the systems offer superior control over material flow, allowing operators to adjust the conveying rate based on production demands. This dynamic control helps optimize production efficiency and reduce downtime. Additionally, the absence of moving parts in the conveying line reduces maintenance requirements and operational costs over time, making these systems economically viable for long-term use.
When applied to calcium carbonate processing, pneumatic conveying systems exhibit several advantages that enhance overall operational performance. For instance, the gentle handling of particles prevents agglomeration, which is crucial for maintaining the quality of calcium carbonate used in applications like paper coating, plastics, and construction materials. The system's ability to transport materials over long distances without significant pressure loss ensures consistent material delivery to downstream processes. Furthermore, the integration of dust collection and filtration systems within the conveying line helps maintain a clean and safe working environment, adhering to industrial safety standards. These features collectively contribute to improved product quality, reduced waste, and enhanced operational reliability in calcium carbonate processing facilities.
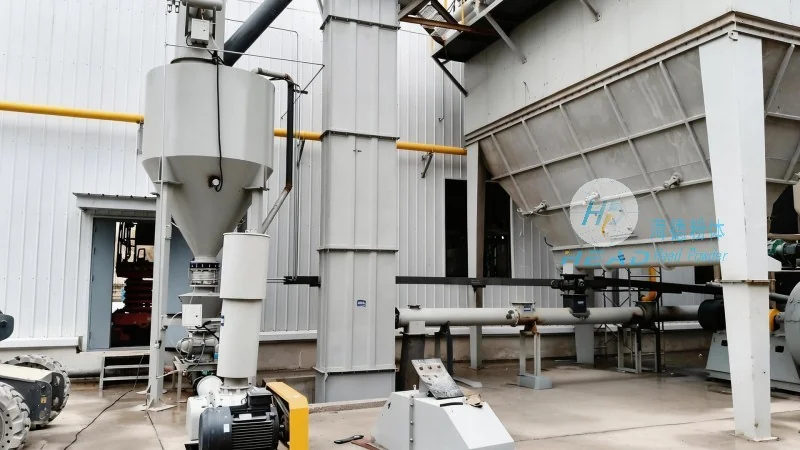
Calcium carbonate pneumatic conveying systems, as developed by HeadPowder, represent a sophisticated solution for efficient material transport in industrial settings. By leveraging the principles of air-based transport and incorporating advanced design elements, these systems address the unique challenges of handling calcium carbonate while delivering reliable performance. With their adaptability, cost-effectiveness, and ability to maintain product integrity, they remain a preferred choice for manufacturers seeking to optimize their production processes. HeadPowder's commitment to quality and innovation ensures that these systems meet the evolving demands of the calcium carbonate industry, providing sustainable and efficient solutions for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top