Nitrogen-protected powder pneumatic conveying is a specialized technology used in industrial applications to transport bulk powders safely and efficiently. This method involves using an inert gas, typically nitrogen, to create a protective atmosphere that prevents oxidation, moisture absorption, or other degradation of the powder during transport. The technology is particularly crucial for handling sensitive materials such as food additives, pharmaceuticals, and high-value chemicals where maintaining product integrity is paramount.
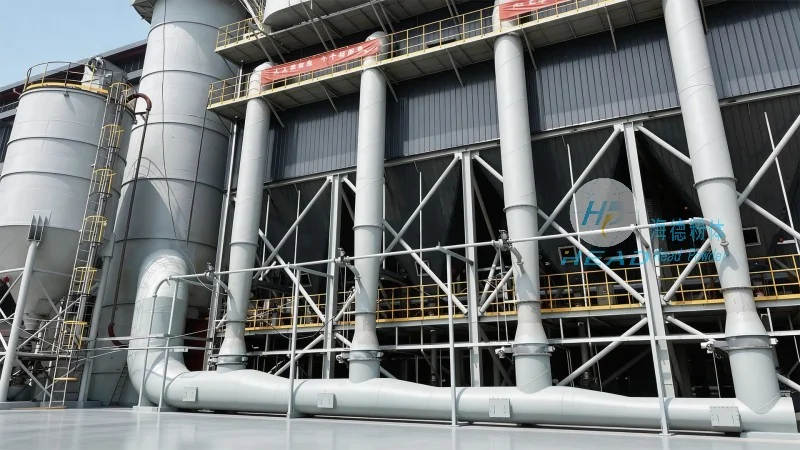
The core principle of nitrogen-protected powder pneumatic conveying is the creation of a closed or semi-closed system where nitrogen gas is introduced to displace air and create an inert environment. In this system, the powder is conveyed through a pipeline using a combination of pressure or vacuum, with nitrogen continuously purging the system to maintain a low oxygen level. This process ensures that the powder remains stable and free from contamination throughout the conveying process. The nitrogen gas acts as a barrier against external factors, such as moisture from the air or oxidation from oxygen, which could otherwise compromise the quality of the material.
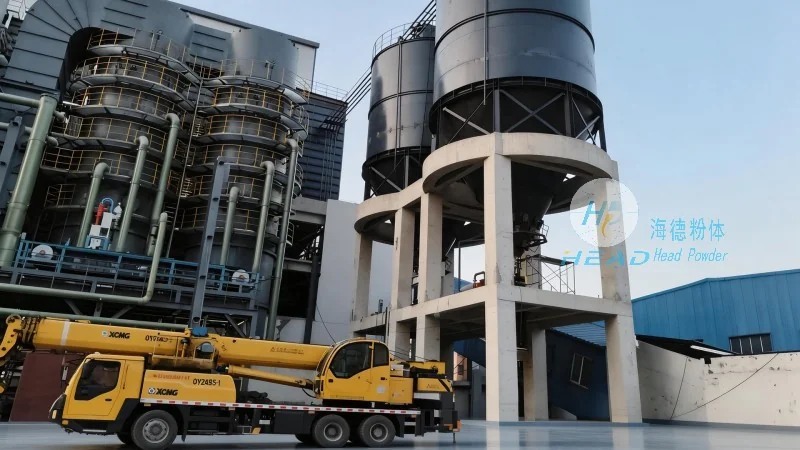
The working scene characteristics of nitrogen-protected powder pneumatic conveying are tailored to specific industrial needs, offering flexibility and adaptability in various applications. One of the primary characteristics is the ability to handle a wide range of powder types, from fine powders to bulk materials, with minimal degradation. The system is also designed to operate in environments where product purity is critical, such as in pharmaceutical manufacturing or food processing, where cross-contamination must be avoided. Additionally, the technology allows for precise control over the conveying rate and pressure, enabling efficient material handling while maintaining product quality. The working scenes often involve integration with existing industrial processes, such as storage silos, mixing equipment, and packaging lines, to create a seamless material flow.
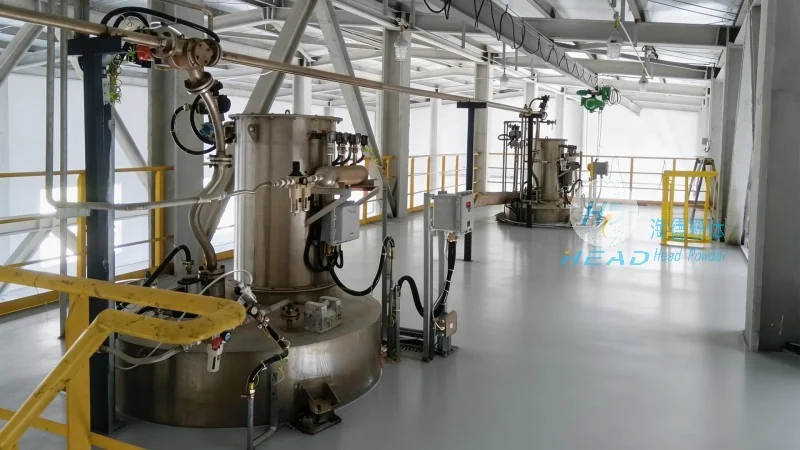
Real-world applications of nitrogen-protected powder pneumatic conveying span multiple industries, demonstrating its versatility and effectiveness. In the pharmaceutical industry, for example, this technology is used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, ensuring that the final product meets stringent regulatory standards. Similarly, in the food industry, it is employed to convey food-grade powders like sugar, flour, and dairy products, maintaining their freshness and preventing spoilage. The system is also utilized in chemical manufacturing to handle reactive or sensitive chemicals, where the inert nitrogen atmosphere prevents unwanted reactions or degradation. These applications highlight the importance of the technology in maintaining product integrity and operational efficiency across diverse industrial sectors.
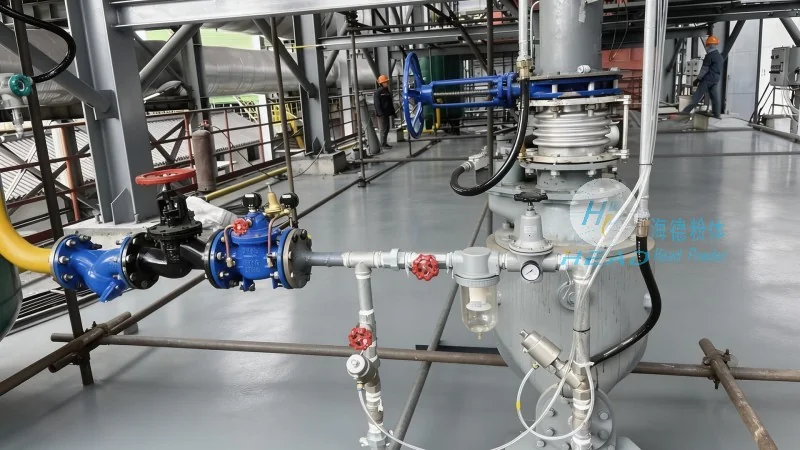
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced powder handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing nitrogen-protected pneumatic conveying systems tailored to the unique needs of various industries. HeadPowder's expertise lies in creating customized solutions that ensure efficient, safe, and reliable powder transport, helping clients optimize their production processes and maintain product quality. The company's commitment to excellence is reflected in its state-of-the-art manufacturing facilities and rigorous quality control measures, ensuring that every system meets the highest industry standards. Based in Shandong, China, headpowder serves a global clientele, delivering solutions that enhance operational efficiency and support sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top