HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and implementation of ash pneumatic conveying lines. These systems are engineered to efficiently transport ash and similar bulk materials from various industrial sources to designated disposal or processing locations. The core principle behind these systems involves the use of air pressure to move material through a pipeline network, offering a flexible and effective method for handling ash in power plants, waste incineration facilities, and other industrial settings.
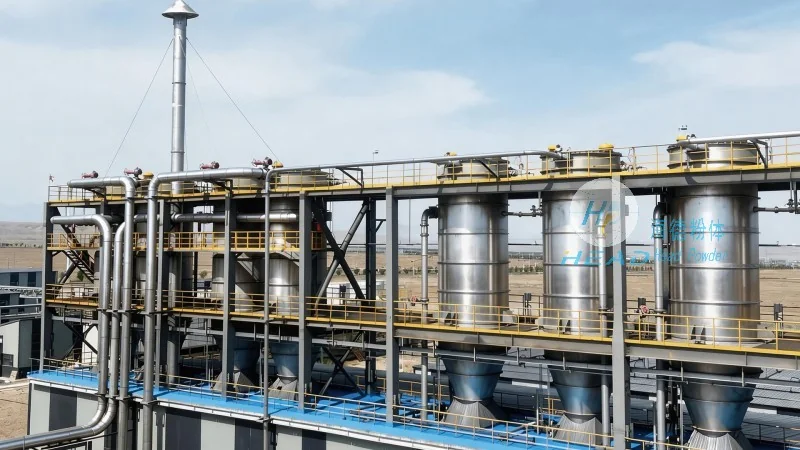
The fundamental principle of ash pneumatic conveying is based on the creation of a pressure differential within a sealed pipeline system. By generating a high-pressure air stream, typically using a positive displacement blower or a rotary lobe pump, the system creates sufficient force to lift and transport the ash particles. The air, often mixed with the ash, moves through the pipeline, carrying the material to the discharge point. This method eliminates the need for mechanical components like buckets or belts, reducing maintenance requirements and increasing operational reliability. The system can operate in both positive and negative pressure modes, adapting to different application requirements and material characteristics.
Ash pneumatic conveying lines typically consist of several critical components that work in concert to ensure efficient material transport. These include the air supply unit, which generates the necessary pressure; the conveying pipeline, which forms the transport path; the ash feed system, which introduces the material into the pipeline; and the discharge and control equipment, which manages the material's exit and system regulation. The air supply unit is responsible for maintaining the required pressure and airflow, while the conveying pipeline is designed to handle the material's specific properties, such as particle size and moisture content. The ash feed system may include hoppers or feeders that ensure a consistent material flow, preventing blockages and ensuring smooth operation. The discharge equipment, such as rotary valves or silos, controls the release of the ash to the next stage of processing or disposal.
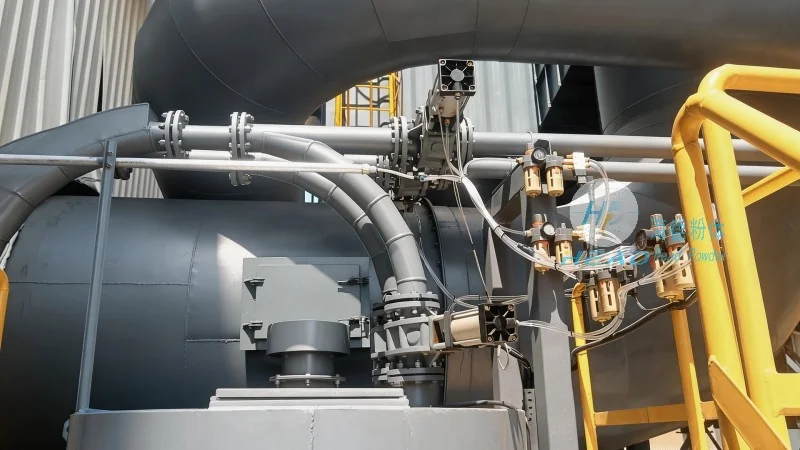
The application of ash pneumatic conveying systems is characterized by several key features that make them suitable for specific industrial environments. One of the primary advantages is their ability to handle ash with varying particle sizes and moisture levels, which is common in power generation and waste treatment facilities. The systems are designed to operate in both indoor and outdoor settings, adapting to the operational needs of different plants. For example, in power plants, these systems are often used to transport fly ash from boiler hoppers to storage silos or to transfer bottom ash from ash hoppers to disposal sites. In waste incineration facilities, they are employed to move ash from the incinerator to landfills or recycling facilities. The flexibility of the system allows for integration with existing infrastructure, minimizing the need for major construction or modifications to the plant layout.
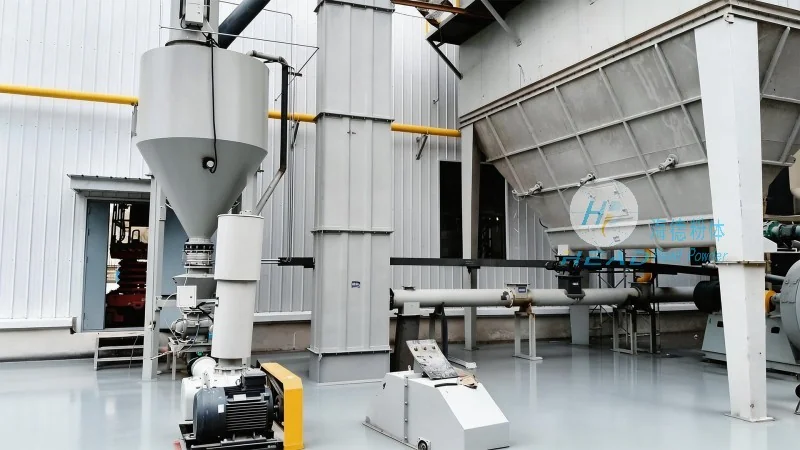
HeadPowder's ash pneumatic conveying lines offer several advantages over traditional mechanical conveying methods. These include reduced labor costs due to the automated operation of the system, lower maintenance requirements as there are fewer moving parts, and increased safety as the system operates in a sealed environment, minimizing dust exposure and potential hazards. Additionally, the systems are highly efficient in terms of energy consumption, as the air pressure can be optimized to match the material's characteristics, resulting in lower operational costs. The compact design of the conveying lines also allows for space-saving installations, which is particularly beneficial in existing industrial facilities where space is limited. Furthermore, the systems are designed for durability and long-term performance, with components constructed from materials resistant to corrosion and wear, ensuring reliable operation over extended periods.
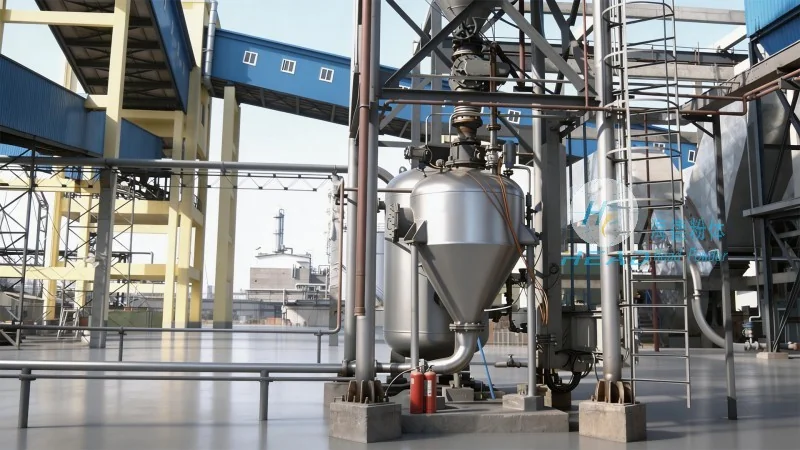
Real-world applications of ash pneumatic conveying systems demonstrate their effectiveness in various industrial scenarios. In a thermal power plant, for instance, the system may be used to transport fly ash from the boiler's bottom ash hopper to a storage silo, with the ash being conveyed through a network of pipelines to the storage facility. The system operates continuously, ensuring a steady supply of ash for disposal or further processing. In a municipal waste incineration plant, the ash from the incinerator is conveyed to a landfill or a recycling facility, with the system designed to handle the high moisture content and varying particle sizes of the ash. The positive pressure mode is often used in these applications to prevent the ingress of external air and maintain the integrity of the ash material. Another example is in a cement production facility, where ash is used as a raw material in the cement-making process, and the pneumatic conveying system efficiently transports the ash from storage silos to the cement production line.
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides advanced ash pneumatic conveying solutions that leverage the principles of air pressure to efficiently transport ash and similar bulk materials. These systems are designed to meet the specific needs of industrial applications, offering flexibility, efficiency, and reliability. By incorporating the latest technology and engineering expertise, HeadPowder ensures that its ash pneumatic conveying lines deliver optimal performance and contribute to the safe and effective management of ash in various industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top