HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and manufacturing of dry cobblestone pneumatic conveying systems. This article explores the classification and essential components of such systems, highlighting their functionality and application in material handling processes.
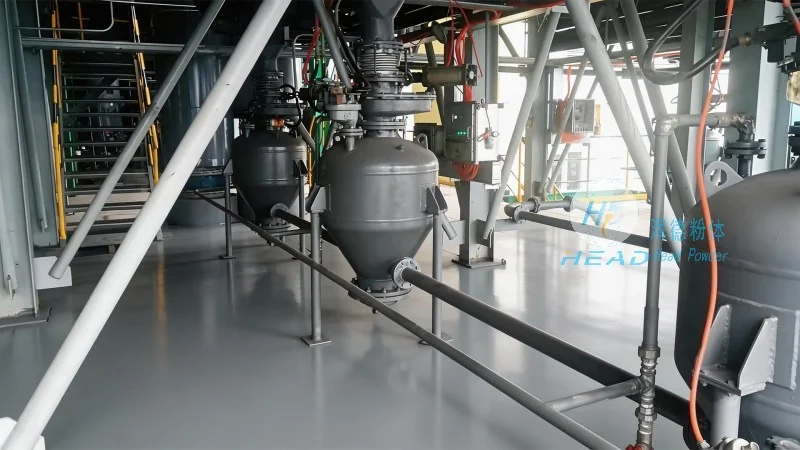
Dry cobblestone pneumatic conveying systems are primarily categorized based on the pressure differential within the system. The two main types are positive pressure systems and negative pressure systems, each with distinct operational characteristics and suitability for different material handling scenarios.
Positive pressure systems operate by generating air pressure within the conveying line, typically using a blower or fan. This method is effective for transporting materials over long distances or through complex layouts, as the pressurized air pushes the material forward. Negative pressure systems, on the other hand, create a vacuum in the conveying line, drawing material from the source and pulling it through the system. This approach is often preferred for applications requiring dust control and containment, as it prevents material from escaping into the environment.
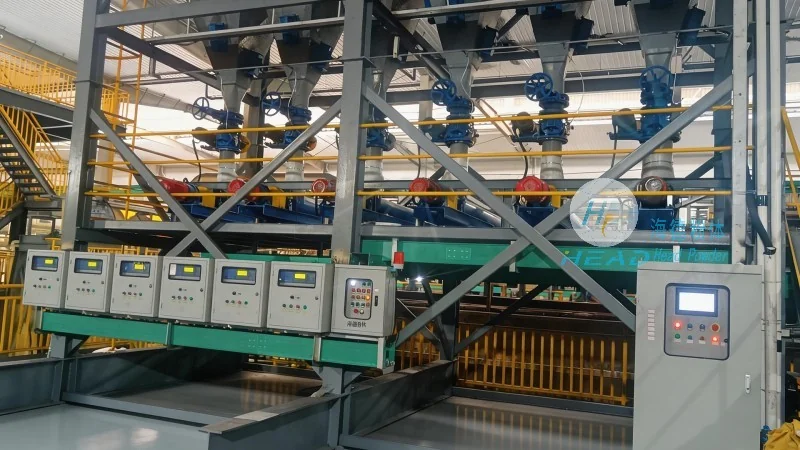
The dry cobblestone pneumatic conveying system consists of several critical components that work in tandem to ensure efficient material transport. The primary components include the material feed hopper, the air supply unit (blower or fan), the conveying pipeline, the material separator, and the discharge outlet.
The material feed hopper is responsible for storing and feeding the dry cobblestone material into the system. It is designed to handle bulk materials and ensure a consistent flow rate, preventing blockages and maintaining system efficiency. The air supply unit provides the necessary airflow to move the material through the pipeline. This component can be a positive displacement blower or a centrifugal fan, depending on the system's requirements and the material's characteristics.
The conveying pipeline is the main channel through which the material and air travel. It is typically made of durable materials such as stainless steel or plastic, chosen for their resistance to abrasion and corrosion from the dry cobblestone. The pipeline may include bends, elbows, and other fittings to navigate the system layout, and its diameter is carefully selected to optimize airflow and material transport efficiency.
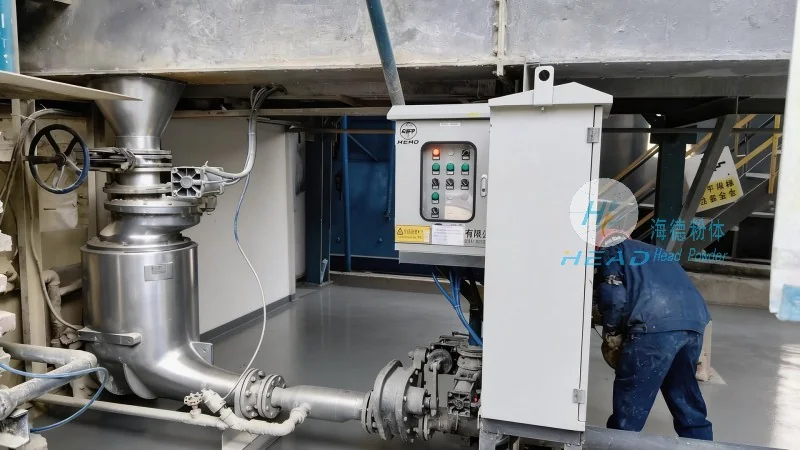
The material separator, also known as a cyclone or filter, is a crucial component for separating the material from the air stream. As the mixture of material and air enters the separator, the centrifugal force causes the heavier cobblestone particles to be separated and collected in a hopper. The cleaned air is then discharged back into the environment or recirculated, depending on the system's design. This separation process is vital for maintaining system performance and ensuring that the material is delivered to the discharge point without contamination.
The discharge outlet is the final component of the system, where the dry cobblestone material is released from the conveying line. It is typically equipped with a valve or gate to control the flow rate and prevent material spillage. The design of the discharge outlet may vary based on the application, such as a screw conveyor or a hopper, to ensure that the material is transferred to the next stage of the process smoothly.
Dry cobblestone pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These systems are highly efficient in transporting materials over long distances, with minimal energy consumption compared to other methods. They also provide excellent dust control, as the material is contained within the system, reducing environmental impact and improving workplace safety. Additionally, the systems are flexible and can be easily adapted to different layouts and material types, making them suitable for a wide range of industrial applications.
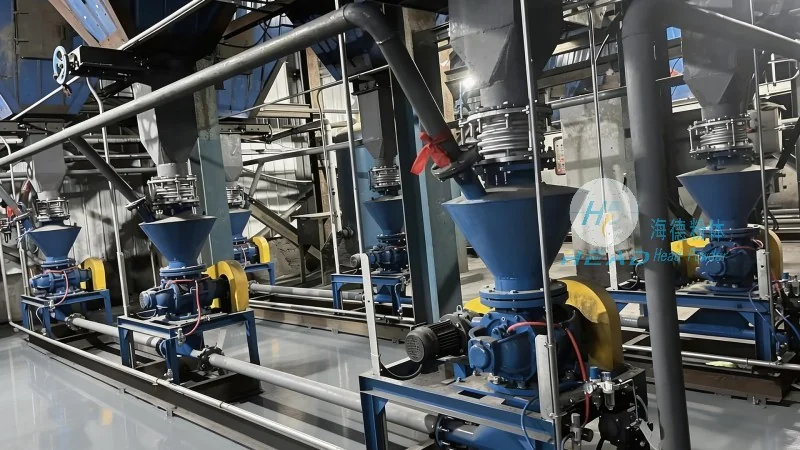
Common applications of dry cobblestone pneumatic conveying systems include the transportation of construction materials, such as gravel and crushed stone, in road and building projects. They are also used in mining operations to move ore and other bulk materials from extraction sites to processing facilities. The systems are versatile and can be integrated into various industrial processes, including manufacturing, packaging, and material handling in warehouses.
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the development and implementation of dry cobblestone pneumatic conveying systems. By understanding the classification and key components of these systems, industries can optimize their material handling processes, improve efficiency, and reduce operational costs. The company's expertise in designing customized solutions ensures that clients receive systems tailored to their specific needs, enhancing productivity and operational reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top