Efficient and reliable sugar handling is crucial for the sugar industry, and modern conveying systems play a pivotal role in optimizing the entire production process. This article provides an overview of sugar conveying systems, with a focus on the advantages and features of sugar pneumatic conveying technology.
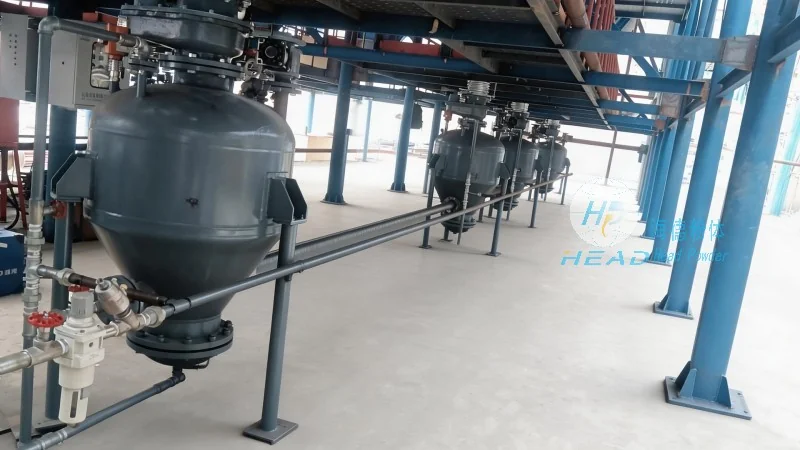
Sugar conveying systems are designed to transport sugar from one location to another within a processing facility or between different stages of production. These systems can be categorized into various types, including mechanical, pneumatic, and hydraulic conveyors. Each type has its own set of applications and operational characteristics, but for high-volume and high-speed sugar transport, pneumatic conveying systems have become increasingly popular due to their efficiency and flexibility.
Sugar pneumatic conveying, also known as air conveying, utilizes air pressure to move sugar particles through a pipeline. This method offers several key advantages that make it an ideal choice for sugar processing plants. First, it provides a dust-free and hygienic environment, which is essential for maintaining product quality and meeting regulatory standards. Unlike mechanical conveyors that may generate dust and cause contamination, pneumatic systems keep the sugar clean and free from external particles.
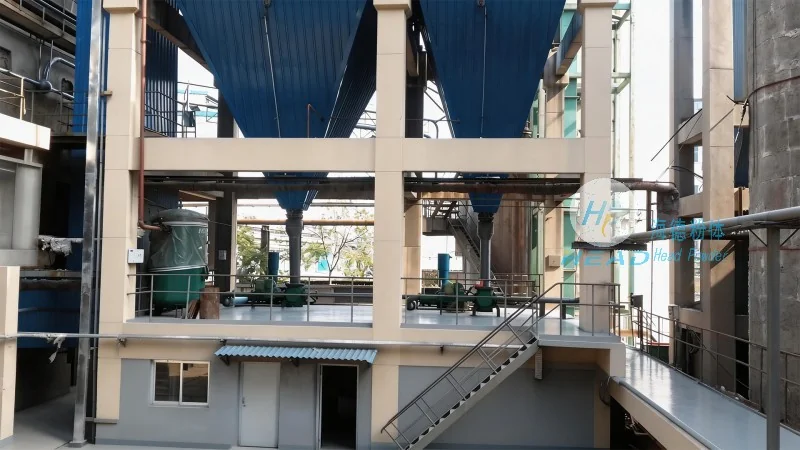
Second, pneumatic conveying systems offer high transport capacities and can handle a wide range of sugar types, including granulated, powdered, and crystalline forms. The flexibility of the system allows for the transportation of sugar over long distances and through complex layouts, making it suitable for large-scale industrial operations. Additionally, these systems can be easily integrated with other processing equipment, such as mixers, classifiers, and packaging machines, enhancing overall operational efficiency.
Third, the energy efficiency of sugar pneumatic conveying is a significant advantage. By using compressed air as the primary driving force, the system minimizes the need for mechanical components that require constant maintenance and energy consumption. This results in lower operational costs and reduced downtime, contributing to the long-term profitability of the sugar processing facility.
Modern sugar pneumatic conveying systems are equipped with several advanced features that enhance their performance and reliability. One of the most important features is the use of positive displacement blowers or rotary lobe pumps, which provide consistent air pressure and flow rates. These components ensure that the sugar is transported smoothly and without clogging, even with varying particle sizes and moisture content.
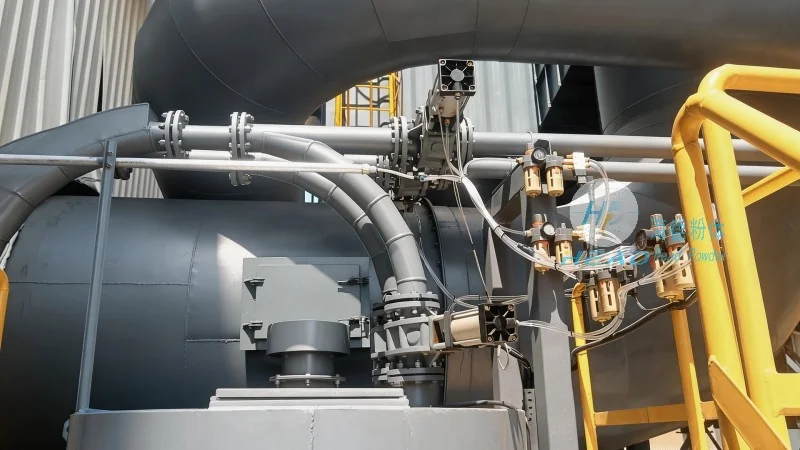
Another critical feature is the inclusion of filtration and separation equipment. Pneumatic systems often incorporate cyclone separators and bag filters to remove any fine particles or moisture from the air, preventing contamination and maintaining the purity of the sugar. This is particularly important in the food industry, where product quality and safety are paramount.
Furthermore, advanced control systems are integrated into modern sugar conveying systems to monitor and regulate the conveying process. These systems can adjust air pressure, flow rate, and conveyor speed in real-time, ensuring optimal performance and preventing overloading or underloading of the system. The use of sensors and feedback mechanisms allows for precise control, reducing the risk of product loss or damage.
Sugar pneumatic conveying systems are widely used in various stages of sugar processing, from raw material handling to final product packaging. In the raw material handling stage, these systems can transport sugar beets or cane from storage areas to processing units, ensuring a continuous supply of raw material. During the refining process, pneumatic conveyors are used to move sugar crystals from one stage to another, such as from the crystallizer to the classifier or the dryer.
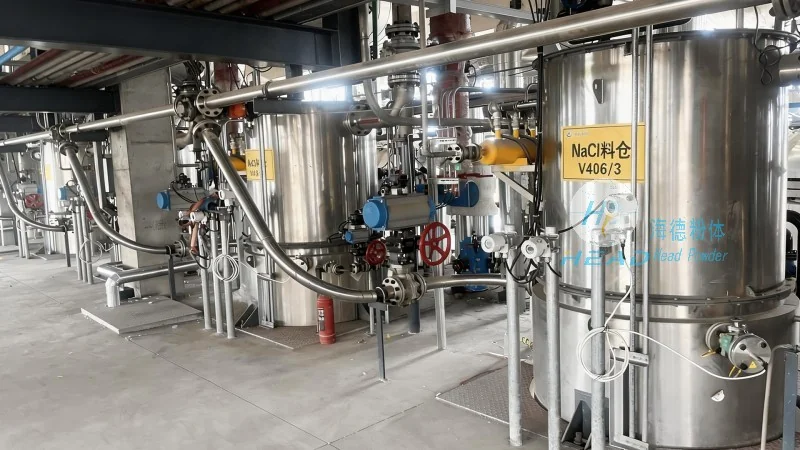
In the final stages of production, sugar pneumatic conveying systems are used to transport finished sugar products to packaging lines. This ensures that the sugar is delivered to the packaging equipment in a clean and controlled manner, minimizing the risk of contamination and ensuring consistent product quality. The ability to handle different sugar forms and transport them over long distances makes pneumatic systems versatile and adaptable to various production requirements.
Sugar conveying systems, particularly pneumatic conveying, are essential components of modern sugar processing facilities. The advantages of dust-free operation, high capacity, energy efficiency, and flexibility make these systems the preferred choice for many sugar manufacturers. By leveraging advanced technology and design, companies like Shandong HeadPowder Engineering Co., Ltd. in China are providing reliable and efficient solutions to meet the evolving needs of the sugar industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top