Understanding the cement fly ash material handling system is crucial for optimizing industrial operations, especially in the cement and power generation sectors where fly ash is a byproduct requiring efficient transport and utilization. This system is engineered to handle the unique properties of fly ash, a fine powder that is often used as a supplementary cementitious material in concrete production. The design principles behind such systems are centered on ensuring efficient, safe, and cost-effective material transport, addressing challenges like dust control, material flow, and system durability.
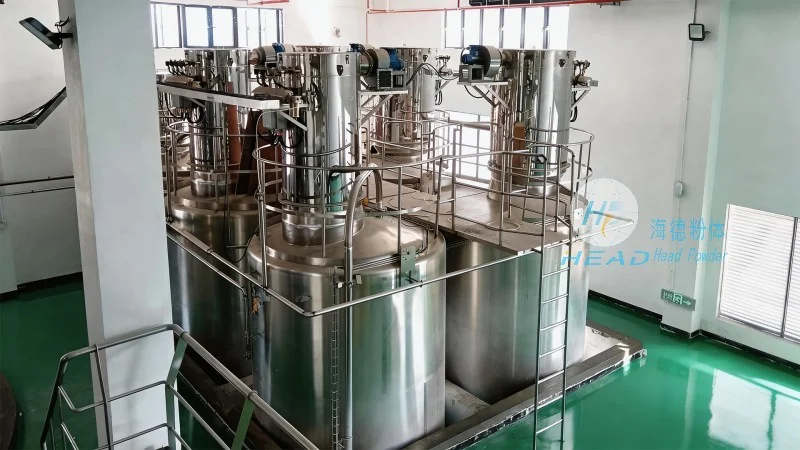
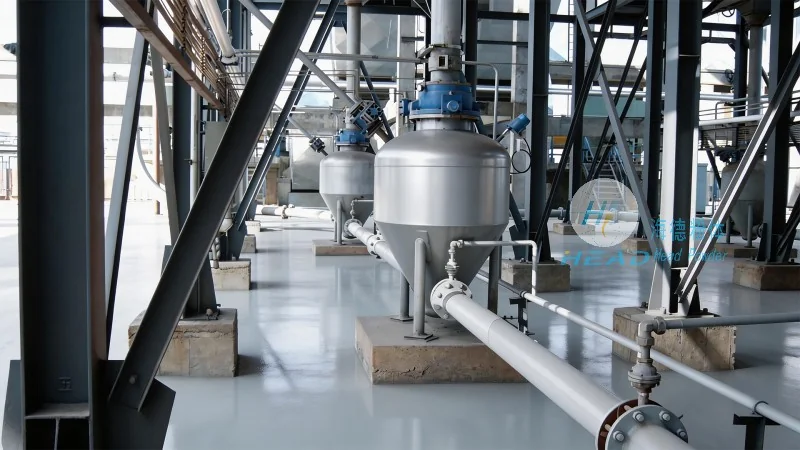
The cement fly ash material handling system typically consists of several critical components that work in tandem to achieve seamless material transport. These components include feeders, conveyors, storage silos, and control systems. The feeders are responsible for uniformly feeding the fly ash from the source, such as a storage silo or a hopper, into the conveyor system. The conveyors, often using technologies like belt conveyors or pneumatic systems, transport the fly ash to the desired destination, such as a mixing plant or a storage facility. Storage silos are integrated to provide temporary storage, allowing for buffer capacity and preventing interruptions in the material flow. Control systems, equipped with sensors and automation, monitor the system's performance, ensuring optimal operation and safety.
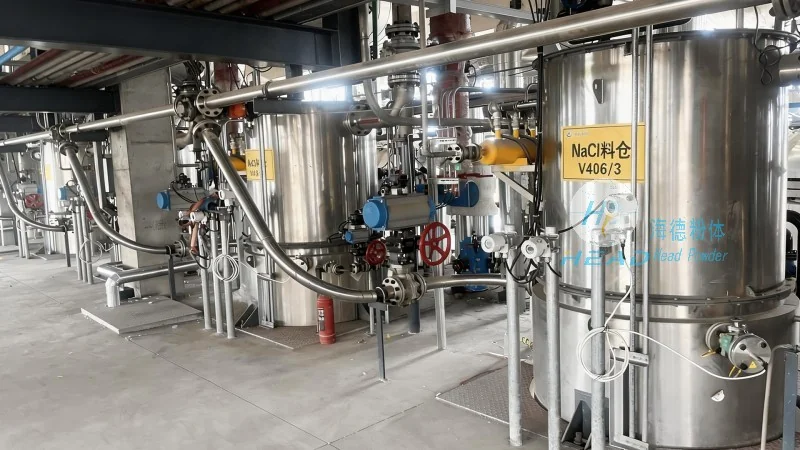
The design of a cement fly ash material handling system is guided by several key principles aimed at maximizing efficiency and minimizing operational risks. One of the primary principles is the consideration of material properties. Fly ash is a fine, abrasive powder that can cause wear on equipment and generate dust, which necessitates the use of materials like stainless steel or specialized coatings for components like hoppers and conveyors. Another critical principle is the optimization of material flow. The system is designed to maintain a consistent flow rate, preventing blockages or surges that could lead to system failures. This involves careful selection of conveyor speeds, feeder capacities, and silo dimensions to match the production requirements. Additionally, the design incorporates dust control measures, such as sealed systems and dust collection equipment, to comply with environmental regulations and ensure workplace safety. The system is also engineered for durability and low maintenance, using robust components that can withstand the abrasive nature of fly ash and the operational stresses of continuous use.
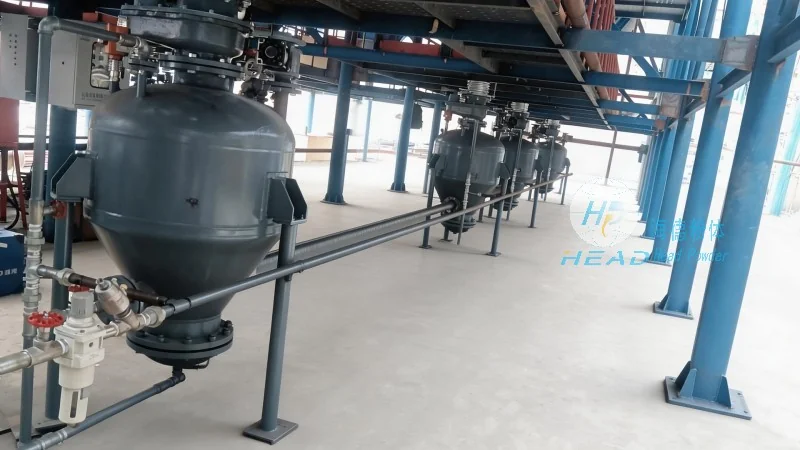
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and installation of cement fly ash material handling systems. With a focus on tailored solutions that meet the specific needs of clients, HeadPowder leverages advanced engineering principles and industry experience to deliver systems that enhance operational efficiency and reduce costs. The company's expertise lies in understanding the unique challenges of handling fly ash, such as its fine particle size and potential for dust generation, and addressing these through innovative design solutions. By integrating state-of-the-art technologies and adhering to international standards, HeadPowder ensures that its systems are not only effective but also reliable and sustainable. The company's commitment to quality and customer satisfaction is reflected in its comprehensive approach to system design, from initial consultation and engineering to final installation and after-sales support. With operations based in Shandong, China, HeadPowder serves clients globally, providing customized material handling solutions that contribute to the efficient utilization of fly ash in construction and other industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top