Food material handling equipment is essential in the food processing sector, facilitating the safe, efficient, and hygienic movement of raw materials and finished products. These systems are engineered to meet stringent sanitary standards and operational requirements, playing a critical role in maintaining product quality and regulatory compliance. Understanding the components, functions, and design principles of such equipment is vital for businesses aiming to optimize their production workflows.
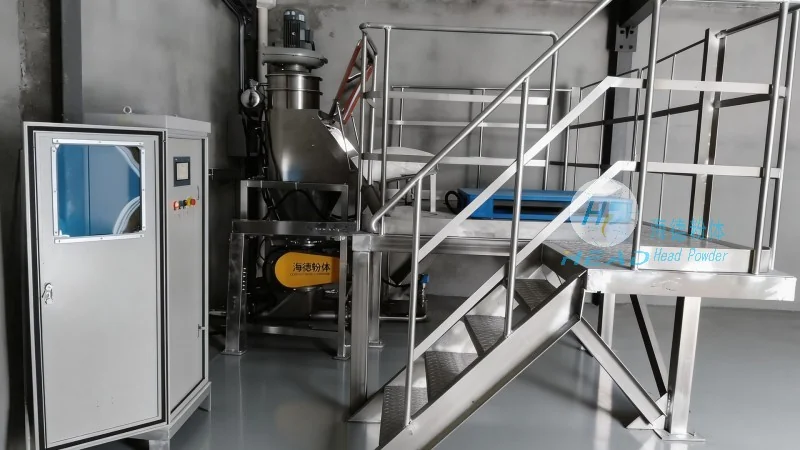
Food material handling equipment comprises interconnected components, each serving a specific purpose in material flow. Conveyors, for example, transport bulk or packaged goods over short to medium distances, including belt, chain, or roller types, designed to handle diverse food products while ensuring cleanliness and preventing contamination. Pneumatic conveying systems are critical for powders and granules, using air pressure to move materials through pipelines. Sorting and inspection equipment like metal detectors or checkweighers are integrated to ensure product safety and quality before further processing.
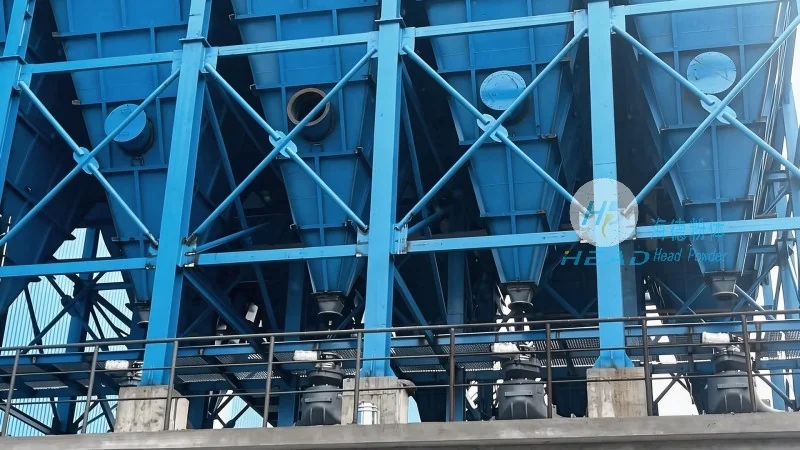
The design of food material handling equipment follows key principles to ensure optimal performance and compliance. Hygiene is paramount, with equipment constructed from stainless steel for easy cleaning and corrosion resistance. The design minimizes product contact with surfaces to reduce cross-contamination risk. Efficiency is achieved via energy-efficient motors and optimized layouts to reduce downtime and increase throughput. Flexibility is essential, as modular designs allow reconfiguration to adapt to different product types or production volumes.
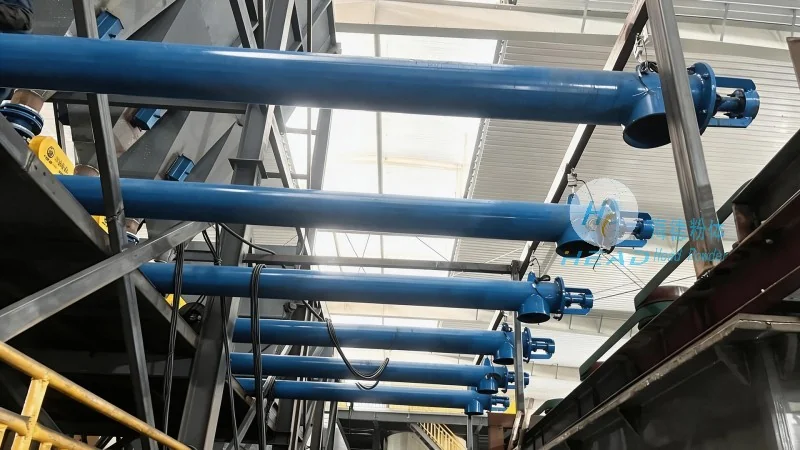
Food material handling equipment is used across various production stages, from raw material reception to packaging. In the bakery industry, conveyors transport dough and baked goods; in the dairy sector, pneumatic systems handle powdered milk and ingredients. Equipment adheres to strict standards like FDA regulations and EU GMP, emphasizing cleanability, durability, and safety features to withstand daily use and maintain product integrity.
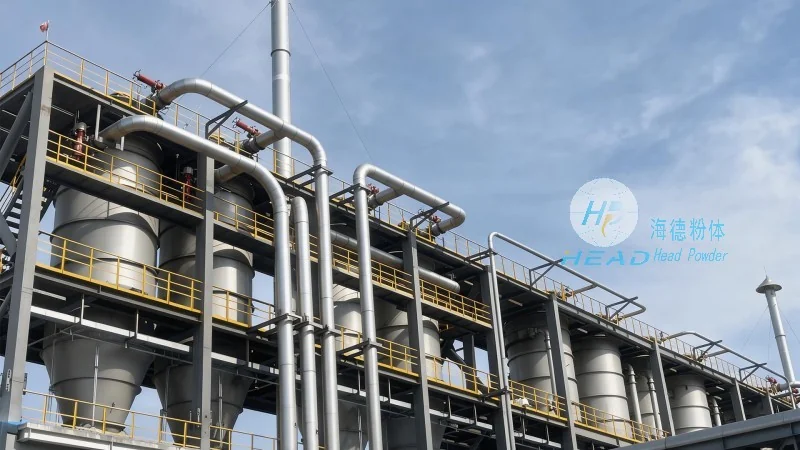
HeadPowder, a leading manufacturer of food material handling equipment, focuses on providing high-quality, tailored solutions for the food processing industry. Committed to innovation and customer satisfaction, the company has built a reputation as a trusted partner. HeadPowder’s products leverage advanced technology and engineering principles, meeting top hygiene and performance standards. The company’s headquarters is in Shandong, China, with a state-of-the-art manufacturing facility equipped with advanced machinery and skilled technicians. HeadPowder’s dedication to quality and customer service has earned it industry recognition, making it a preferred choice for food processing companies globally.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top