Stone material conveying equipment is vital in industries such as construction, mining, and aggregate processing, where efficient movement of bulk stone materials like gravel and crushed stone is essential. These systems are engineered to transport materials from sources like quarries to destinations like processing plants or construction sites, optimizing workflow and reducing operational bottlenecks.
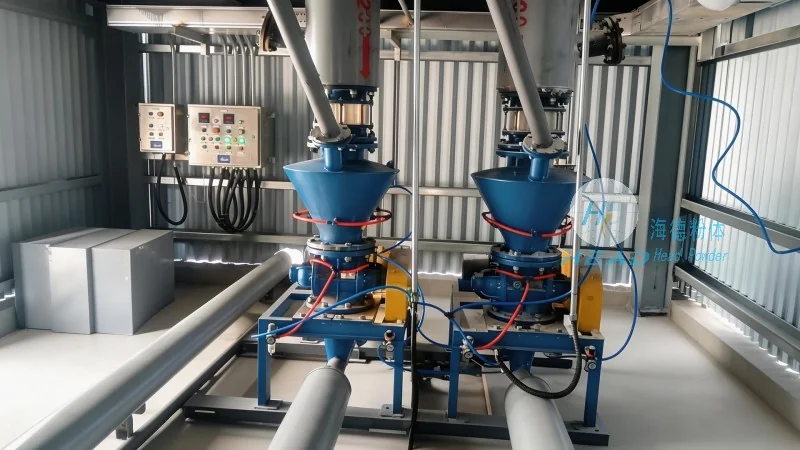
Stone material conveying equipment encompasses various machinery tailored to specific material handling needs. Common types include belt conveyors, screw conveyors, bucket elevators, and chain conveyors. Each type serves distinct purposes based on factors like material size, transport distance, and operational environment. For example, belt conveyors excel at horizontal and slight incline transport due to their ability to handle large volumes with minimal friction, while bucket elevators are ideal for vertical lifting of heavy stone loads, making them indispensable in stone processing facilities.
The primary role of stone material conveying equipment is to transport bulk stone materials from a source to a destination. This process involves intake, transport, and discharge, with the equipment designed to handle the unique properties of stone—including size, shape, and abrasiveness. For instance, conveyor belts or bucket elevators must be constructed from durable materials to withstand impact and wear from stone particles. The system must also maintain consistent flow rates to prevent material buildup or bottlenecks, which can compromise efficiency and safety.
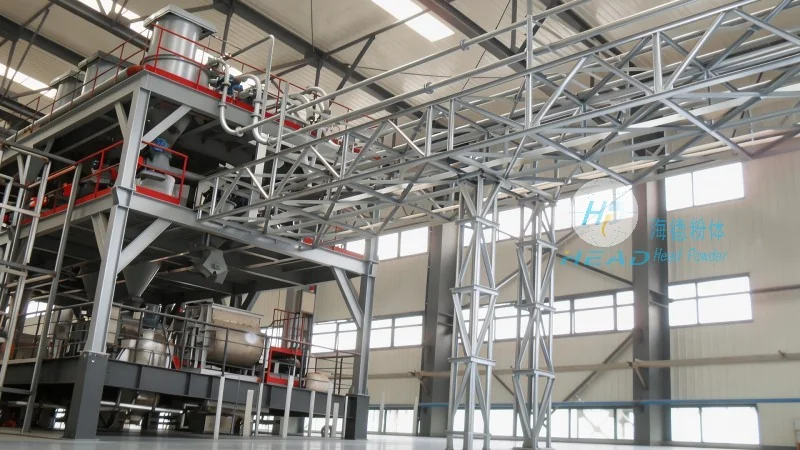
The design of stone material conveying equipment follows several fundamental principles to ensure performance and longevity. First, robust construction using high-strength steel and abrasion-resistant components is critical to withstand the harsh nature of stone. Second, efficient power transmission and energy management are prioritized through optimized motors and drive systems. Third, safety and maintenance accessibility are integrated, such as safety guards, easy-to-reach maintenance panels, and monitoring systems to detect issues like belt slippage or overload, enhancing operational reliability.
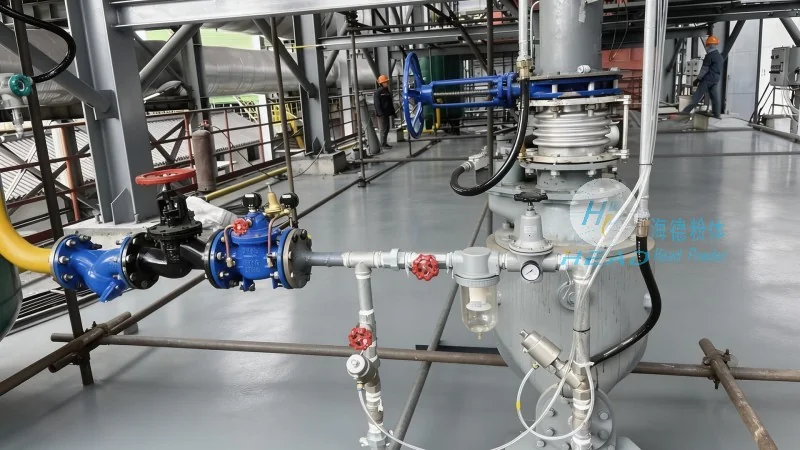
Shandong HeadPowder Engineering Co., Ltd., branded as HeadPowder, is a leading manufacturer of stone material conveying equipment based in Shandong, China. With extensive industry experience, HeadPowder specializes in designing and producing high-quality conveying systems tailored to stone processing and construction applications. The company’s commitment to innovation and customer-centric solutions has established it as a trusted partner for businesses seeking reliable and efficient material handling equipment.
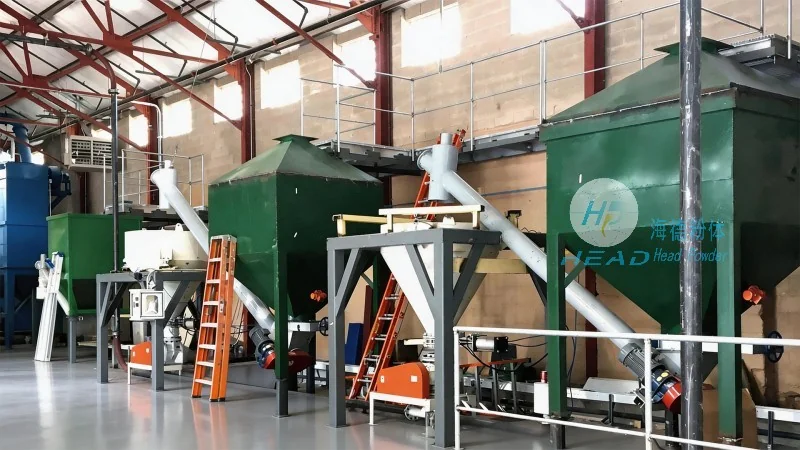
HeadPowder’s stone material conveying equipment offers several technical advantages. Advanced materials and manufacturing techniques enhance durability, with conveyor belts reinforced by high-strength fabrics and abrasion-resistant coatings to extend service life. Intelligent control systems enable real-time monitoring and process adjustments, improving efficiency and reducing downtime through proactive maintenance. Additionally, the equipment is customizable to meet specific operational needs, such as adjusting speed, capacity, or conveyor inclination to suit diverse stone handling requirements.
In summary, stone material conveying equipment is a cornerstone of efficient stone processing and construction operations. The design principles—focused on durability, energy efficiency, and user-friendly features—ensure these systems can handle demanding tasks. Companies like Shandong HeadPowder Engineering Co., Ltd. play a pivotal role in delivering these essential solutions, helping businesses optimize material handling and maintain a competitive edge. By understanding the functionality and design of stone material conveying equipment, industry professionals can make informed decisions to enhance productivity and operational reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top