When it comes to industrial processes involving the handling and transportation of ash materials, the use of specialized equipment is crucial for maintaining efficiency and safety. Purified ash material handling equipment, as the name suggests, is specifically designed to manage ash materials that have undergone purification processes, ensuring that the material is handled in a clean and controlled manner. This equipment plays a vital role in various industrial applications, from power plants to waste management facilities, where the efficient transport of ash is essential for operational continuity.
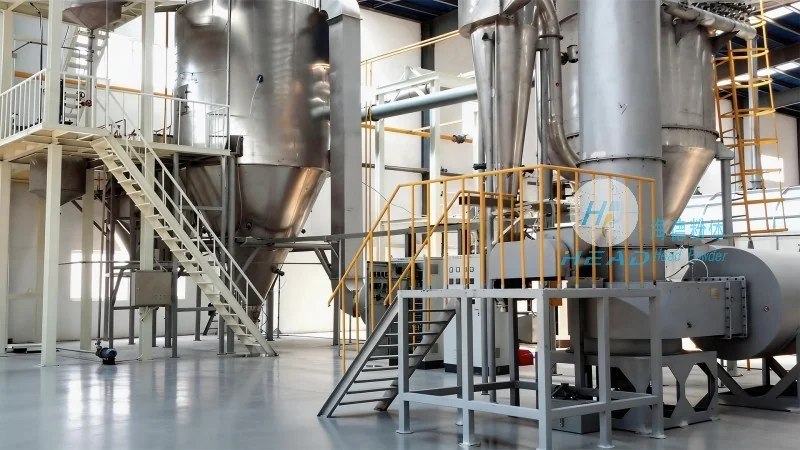
The design of purified ash material handling equipment is built around several key components that work in tandem to ensure optimal performance. These components include high-quality conveyor systems, dust control mechanisms, and material handling units that are engineered to handle the specific characteristics of purified ash. The conveyor systems are typically made from materials resistant to corrosion and abrasion, such as stainless steel or specialized alloys, to withstand the harsh conditions of ash handling. Additionally, the equipment incorporates advanced sealing and filtration systems to minimize dust emissions and maintain a clean working environment. The design also emphasizes durability and reliability, as these systems often operate under high pressure and continuous load conditions.
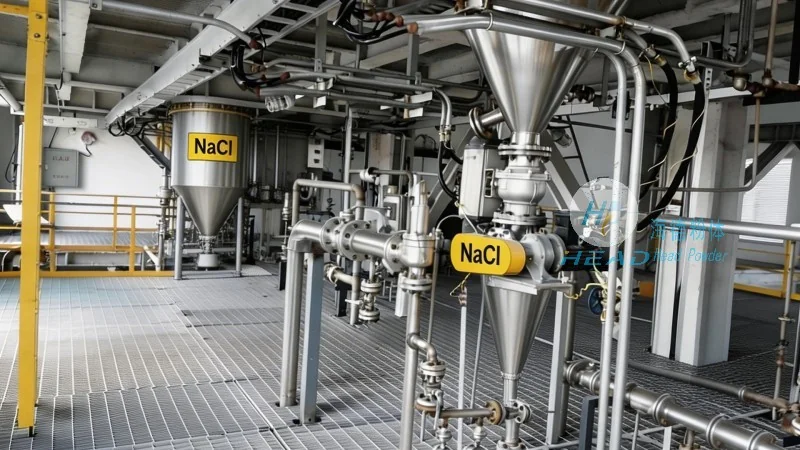
The operational principles of purified ash material handling equipment revolve around the seamless integration of various mechanical and control systems. The process typically begins with the ash being fed into the system, where it is then transported through the conveyor belts or pipes. The equipment uses a combination of gravity and mechanical force to move the ash from one location to another, ensuring a consistent flow rate. Advanced control systems monitor the flow and adjust the speed of the conveyor as needed, maintaining an optimal balance between efficiency and safety. The design also includes safety features such as emergency stop buttons and overload protection to prevent accidents and equipment damage. Furthermore, the equipment is equipped with sensors that detect any blockages or irregularities in the material flow, triggering automatic shutdowns to prevent further issues.
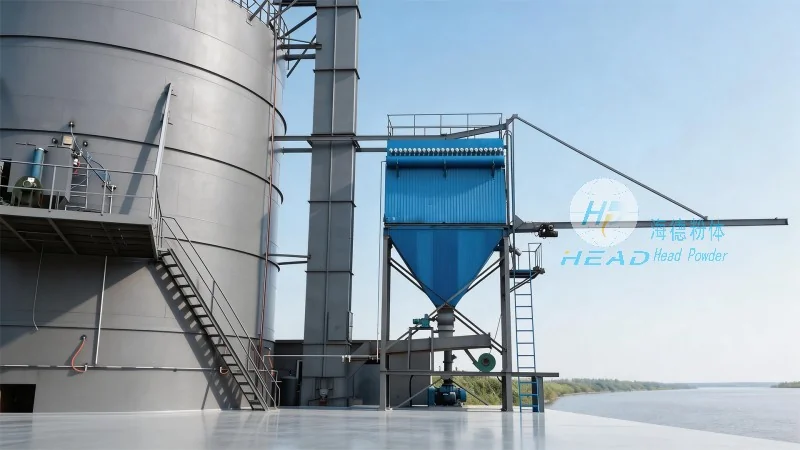
Implementing purified ash material handling equipment offers numerous benefits for industrial operations. Firstly, it enhances operational efficiency by providing a reliable and continuous transport of ash materials, reducing downtime and increasing overall productivity. The equipment’s design minimizes material loss and spillage, which not only improves safety but also reduces the environmental impact of ash handling. Additionally, the advanced dust control systems help maintain a clean and healthy working environment for personnel, reducing the risk of respiratory issues and other health hazards associated with ash exposure. The durability and low maintenance requirements of these systems also contribute to long-term cost savings, as they require fewer repairs and replacements compared to older or less efficient equipment.
Purified ash material handling equipment is widely used across various industries, each with its specific requirements. In power plants, for example, this equipment is essential for transporting ash from the boiler to disposal sites or recycling facilities. The equipment’s ability to handle high volumes of ash efficiently ensures that the power generation process remains uninterrupted. In waste management facilities, the equipment is used to transport ash from incinerators to landfills or other disposal locations, helping to streamline the waste processing workflow. Additionally, in industrial manufacturing plants that generate ash as a byproduct, the equipment facilitates the transport of ash to storage or treatment facilities, ensuring that the manufacturing process can continue without interruptions.
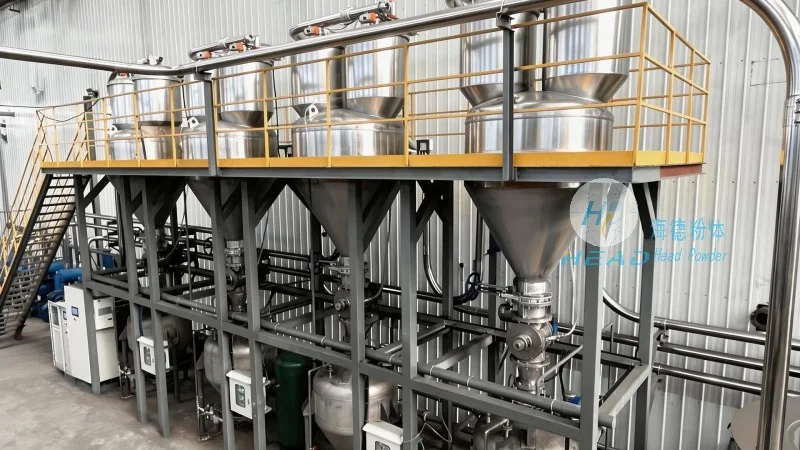
In conclusion, purified ash material handling equipment is a critical component in modern industrial operations, designed to efficiently and safely transport purified ash materials. The equipment’s advanced design and operational principles ensure high performance, reliability, and safety, making it an indispensable tool for various industries. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in providing high-quality equipment tailored to the specific needs of their clients. With a focus on durability, efficiency, and environmental responsibility, HeadPowder has established itself as a trusted partner in the industrial equipment sector. Based in Shandong, China, the company leverages its expertise and experience to deliver solutions that meet the evolving demands of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top