This article provides an overview of malt spent grain material handling equipment, focusing on its design principles and operational aspects. Malt spent grain, a byproduct of the brewing process, requires efficient handling and transportation for various industrial applications. The equipment designed for this purpose is engineered to manage the unique physical and chemical properties of malt spent grain, ensuring optimal performance in processing and material transport.
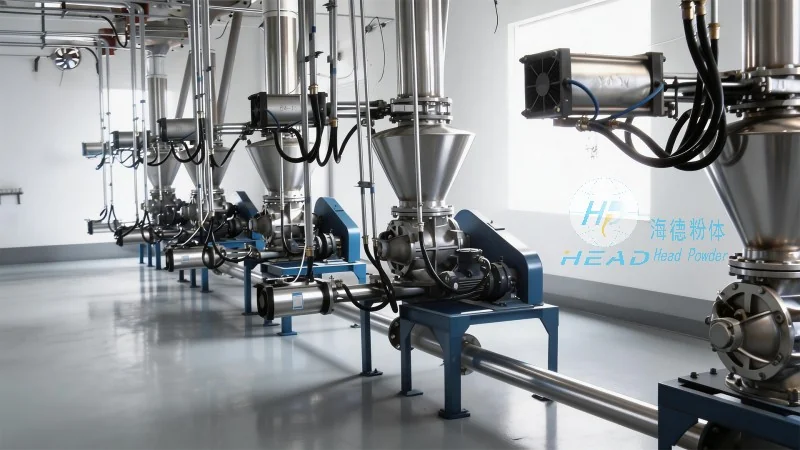
HeadPowder, a prominent company in the material handling industry, specializes in developing and manufacturing equipment tailored to the needs of the food and beverage sector. With a strong presence in Shandong, China, HeadPowder has established itself as a reliable partner for businesses seeking efficient solutions for handling malt spent grain and other similar materials. The company's commitment to quality and innovation has positioned it as a key player in providing advanced material handling equipment for industrial applications.
Malt spent grain, also known as spent grain or brewers' grain, is the solid residue left after the malting and brewing processes. It consists of spent barley or other grains, along with water and other byproducts. Due to its high moisture content and fibrous nature, handling this material requires specialized equipment that can manage its bulk, reduce dust generation, and ensure safe and efficient transport. The design of malt spent grain material handling equipment must consider factors such as material flow, moisture control, and environmental impact to meet the demands of modern industrial operations.
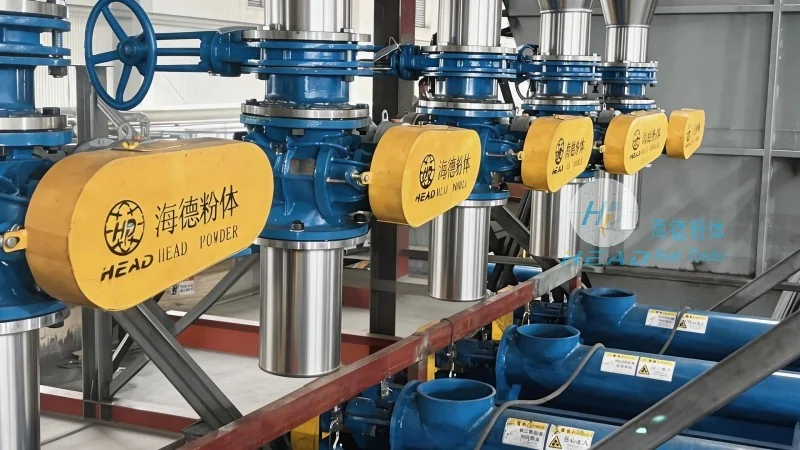
The design of malt spent grain material handling equipment is guided by several critical principles to ensure effective and reliable operation. These principles include: 1. **Material Compatibility**: The equipment must be constructed from materials that are resistant to the acidic and fibrous nature of malt spent grain, preventing corrosion and wear. 2. **Efficient Flow Control**: Proper design ensures smooth material flow, minimizing blockages and ensuring consistent throughput. 3. **Moisture Management**: Features such as moisture control mechanisms help maintain the material's properties and prevent issues like caking or clumping. 4. **Safety and Environmental Considerations**: Equipment is designed to minimize dust emissions and ensure safe handling, adhering to environmental regulations and workplace safety standards. 5. **Durability and Maintenance**: Robust construction and easy maintenance features extend the equipment's lifespan and reduce downtime.
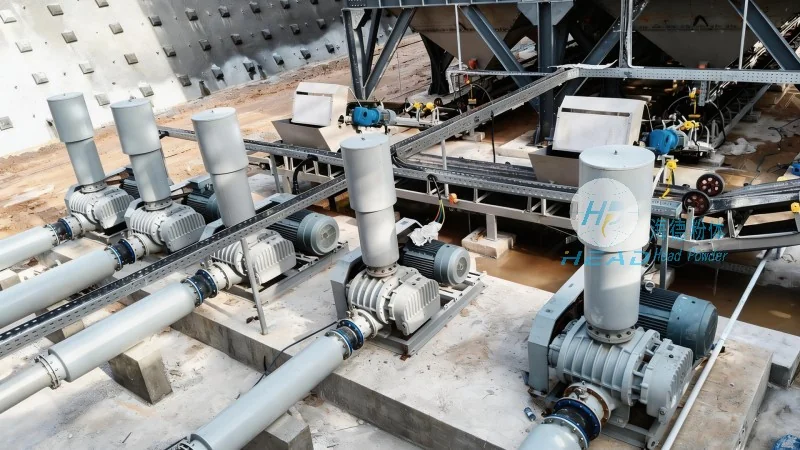
Malt spent grain material handling equipment typically consists of several key components that work together to achieve efficient material transport. These components include: 1. **Feed Hoppers**: These are used to store and feed the malt spent grain into the handling system, ensuring a consistent supply of material. 2. **Conveyors**: Various types of conveyors, such as belt conveyors or screw conveyors, are used to transport the material horizontally or vertically. 3. **Dust Control Systems**: To manage dust generation, equipment may include dust collection systems or enclosed conveyor designs. 4. **Control Panels**: Advanced control panels allow operators to monitor and adjust the equipment's performance, ensuring optimal operation. 5. **Cleaning and Maintenance Features**: Designed for easy cleaning and maintenance, these features help maintain the equipment's efficiency and longevity.
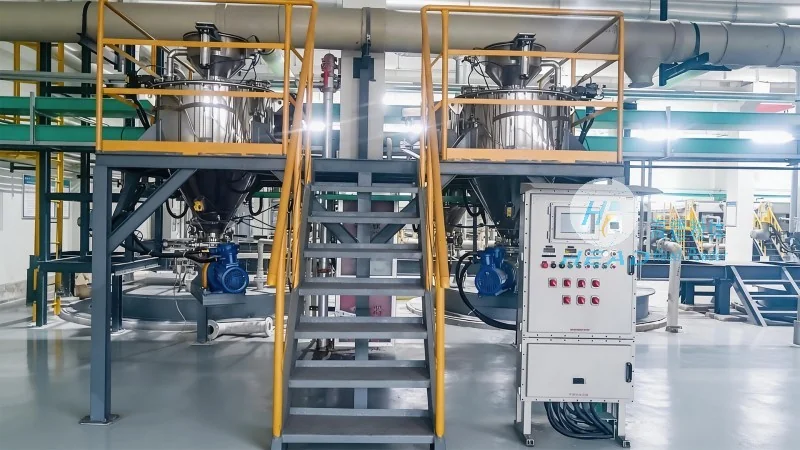
Malt spent grain material handling equipment is widely used in various industrial applications, including: 1. **Breweries**: For the efficient transport of spent grain from brewing tanks to storage or processing areas. 2. **Animal Feed Production**: The equipment helps in handling malt spent grain for use as a feed ingredient, providing a cost-effective and sustainable source of nutrients. 3. **Energy Recovery**: Some systems are designed to recover energy from the material, such as through biogas production or composting. The benefits of using such equipment include improved operational efficiency, reduced labor costs, enhanced safety, and compliance with environmental regulations.
In conclusion, malt spent grain material handling equipment plays a crucial role in the efficient management of malt spent grain, a valuable byproduct of the brewing industry. The design principles and components of this equipment are tailored to address the unique challenges associated with handling this material, ensuring optimal performance and sustainability. Companies like HeadPowder continue to innovate in this field, providing advanced solutions that meet the evolving needs of the industry. By investing in high-quality malt spent grain material handling equipment, businesses can enhance their operational efficiency, reduce costs, and contribute to a more sustainable industrial practice.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top