Ton bag material conveying lines are specialized industrial systems engineered to efficiently handle and transport bulk materials packaged in ton bags, commonly known as super sacks or bulk bags. These systems are crucial in various industries, including mining, construction, agriculture, and chemical processing, where large volumes of raw materials need to be moved from storage or processing areas to production lines or other destinations. The core function of a ton bag conveying line is to automate the process of lifting, moving, and discharging ton bags, reducing manual labor and enhancing operational safety and efficiency.
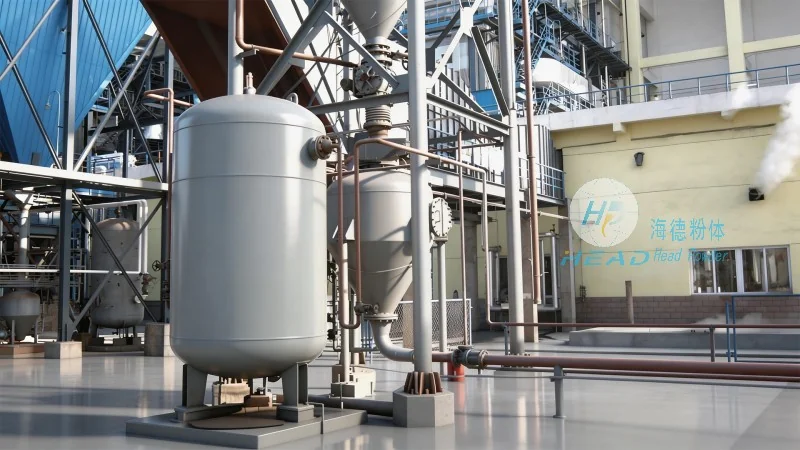
At Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, we specialize in designing and manufacturing high-quality ton bag material conveying lines tailored to meet the specific needs of our clients. Our company, with its headquarters in Shandong, China, has built a strong reputation for delivering reliable and efficient material handling solutions that integrate seamlessly into existing production workflows. The design principles of our ton bag conveying lines are centered on durability, adaptability, and user-friendliness, ensuring that they can handle a wide range of materials and operating conditions.
The design of a ton bag material conveying line involves several critical principles that ensure optimal performance and longevity. First, the system must be capable of safely and efficiently lifting ton bags from the ground or a storage rack. This is typically achieved through the use of mechanical hoists or cranes, which are designed to handle the heavy weight of filled ton bags, often weighing several hundred kilograms or more. The lifting mechanism must be robust and reliable to prevent accidents and ensure consistent operation.
Second, the conveying system itself, such as a conveyor belt or a pneumatic conveyor, is designed to transport the ton bags horizontally or vertically, depending on the layout of the facility. The choice of conveyor type depends on the material characteristics, such as bulk density, flowability, and potential for dust generation. For example, a belt conveyor is often used for dry, free-flowing materials, while a pneumatic conveyor may be preferred for dusty or fine powders to minimize dust exposure and improve air quality.
Third, the discharge mechanism is a critical component of the design. It must be able to open the ton bag and release the material in a controlled manner, preventing spillage and ensuring that the material is directed to the intended destination, such as a silo, hopper, or processing machine. The discharge system may include valves, gates, or other control devices that allow for precise regulation of the material flow rate.
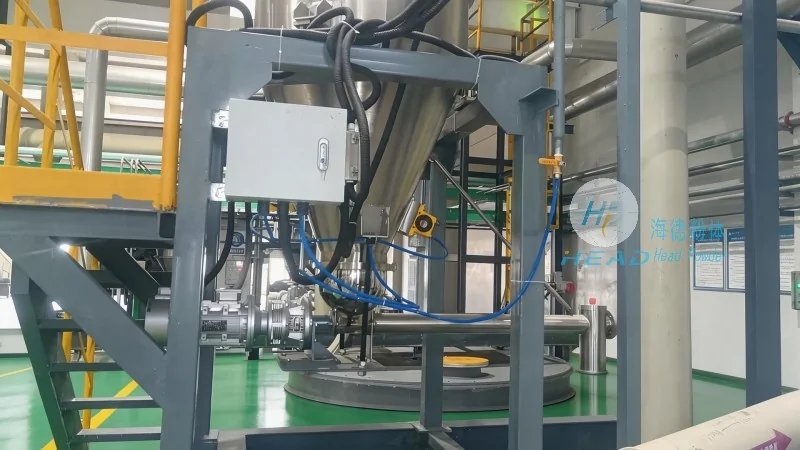
Fourth, safety and maintenance considerations are integral to the design. The system must incorporate safety features, such as emergency stop buttons, overload protection, and guarding to protect operators from moving parts. Additionally, the design should facilitate regular maintenance and cleaning to ensure long-term performance and reduce downtime. For instance, easy access to components like belts, pulleys, and filters can simplify maintenance procedures and extend the service life of the equipment.
Ton bag material conveying lines are widely used in various industrial applications due to their versatility and efficiency. In the mining industry, they are used to transport ore from storage areas to processing plants, where the material is crushed and refined. In the construction industry, they help move cement, sand, and other aggregates from bulk storage to concrete mixing sites. In agriculture, they assist in handling fertilizers, seeds, and other agricultural products, ensuring that they are delivered to farms or processing facilities in a timely manner.
One of the primary benefits of using a ton bag material conveying line is the significant reduction in manual labor. Traditionally, handling ton bags required workers to lift and move heavy bags, which can lead to injuries and fatigue. The automated conveying system eliminates this need, improving workplace safety and reducing the risk of accidents. Additionally, the system enhances operational efficiency by allowing for continuous material flow, which can increase production output and reduce processing time.
Another key benefit is the improvement in material handling accuracy and consistency. Manual handling of ton bags can result in uneven distribution of material, leading to variations in product quality. The automated conveying line ensures that the material is discharged in a controlled manner, maintaining consistent flow rates and reducing the risk of overloading or underloading processing equipment. This consistency is particularly important in industries where product quality is critical, such as pharmaceuticals or food processing.
Furthermore, the use of ton bag material conveying lines can lead to cost savings over time. By reducing the need for manual labor and minimizing material spillage, the system can lower operational costs. Additionally, the durability and reliability of the equipment, designed with high-quality components, can reduce maintenance and replacement costs, providing a long-term return on investment.
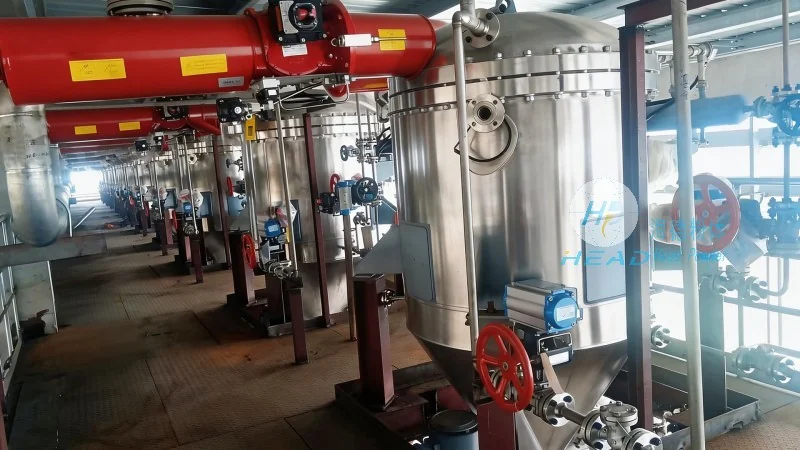
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial facility has unique requirements and constraints. Therefore, our ton bag material conveying lines are designed to be customizable to meet specific client needs. We work closely with our clients to assess their operational requirements, facility layout, and material characteristics to develop a tailored solution that maximizes efficiency and minimizes costs.
Our conveying lines can be integrated with existing systems, such as storage racks, silos, and processing equipment, to create a seamless material handling workflow. For example, a ton bag can be lifted from a storage rack, transported to a processing plant, and discharged directly into a hopper, all without manual intervention. This integration not only improves efficiency but also reduces the need for additional equipment and space, making it an ideal solution for facilities with limited space or complex layouts.
We also offer a range of accessories and optional features to enhance the functionality of our conveying lines. These may include dust collection systems, material level sensors, and control panels with user-friendly interfaces. The dust collection system helps maintain a clean and safe working environment by capturing and filtering dust generated during material handling. The material level sensors provide real-time monitoring of the material level in the hopper or silo, allowing for automatic control of the conveying system to prevent overfilling or underfilling. The control panels enable operators to monitor and control the system from a central location, improving operational oversight and reducing the need for on-site supervision.
Ton bag material conveying lines are essential industrial equipment that plays a vital role in the efficient handling and transportation of bulk materials. The design principles of these systems, including robust lifting mechanisms, suitable conveying methods, controlled discharge systems, and safety features, ensure that they can operate reliably and safely in various industrial environments. At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing high-quality, customized ton bag material conveying lines that meet the specific needs of our clients, helping them improve operational efficiency, enhance workplace safety, and reduce costs. With our expertise and dedication to quality, we are a trusted partner for businesses seeking reliable material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top