Tote bag unloading powder material conveyors are specialized industrial equipment designed to efficiently transfer bulk powder materials from tote bags into processing systems or storage containers. These systems are widely used in various industries such as chemical, food, pharmaceutical, and mining, where handling large volumes of powders is essential for production processes. The primary function of a tote bag unloading conveyor is to automate the process of emptying tote bags, reducing manual labor and minimizing material loss during transfer.
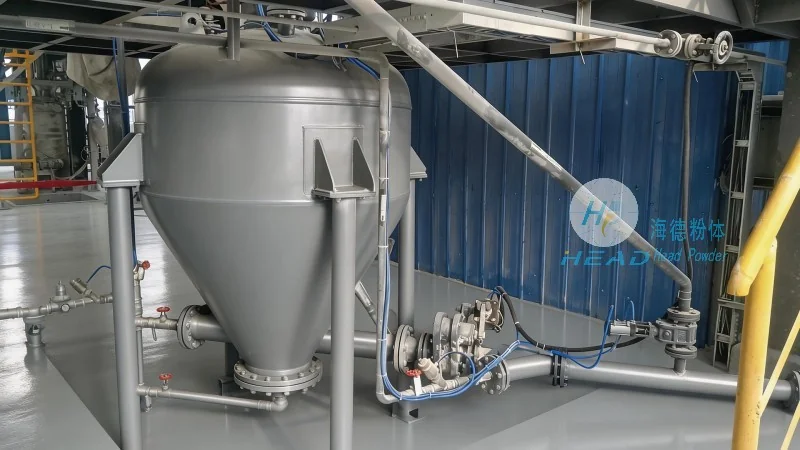
A tote bag unloading powder material conveyor typically consists of a hopper or receiving chamber that captures the material from the tote bag, a discharge mechanism that controls the flow of powder, and a conveyor system that transports the material to the next stage of processing. The equipment is engineered to handle a wide range of powder types, including fine powders, granules, and bulk materials, with varying moisture content and flow characteristics. The design ensures that the material is transferred smoothly and without segregation, maintaining the integrity of the product.
The design of a tote bag unloading powder material conveyor is based on several key principles to ensure optimal performance and reliability. First, the system must be capable of handling the weight and dimensions of standard tote bags, which are commonly used in industrial settings. The receiving hopper is designed with a sloped or conical shape to facilitate the flow of powder from the tote bag into the conveyor. This design minimizes the risk of material bridging or caking, which can occur with certain powder types. Second, the discharge mechanism, often a rotary valve or a gate valve, is engineered to control the flow rate of the material, preventing overloading of downstream equipment. The valve is typically made of durable materials such as stainless steel to withstand the abrasive nature of powders and to maintain hygiene standards, especially in food and pharmaceutical applications.
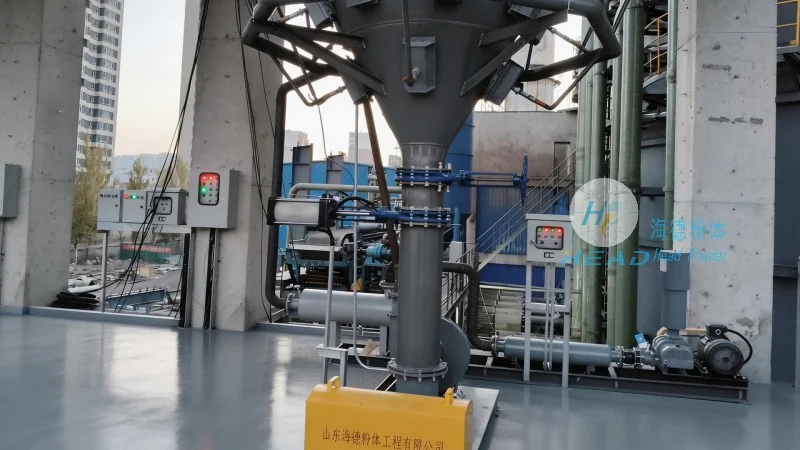
HeadPowder, a leading manufacturer of bulk material handling equipment, specializes in the design, manufacturing, and supply of tote bag unloading powder material conveyors. With a strong presence in China, particularly in Shandong province, HeadPowder has built a reputation for delivering high-quality, reliable equipment tailored to the specific needs of various industries. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and cost-effective powder handling solutions. HeadPowder's facilities are equipped with advanced technology and skilled engineering teams, ensuring that each product meets stringent quality standards and industry regulations.
HeadPowder's tote bag unloading powder material conveyors offer several key features that enhance operational efficiency and product quality. One of the primary benefits is the reduction of manual handling, which not only improves workplace safety but also minimizes the risk of product contamination. The automated system ensures consistent flow rates, reducing the likelihood of overfilling or underfilling containers, which can lead to production delays or material waste. Additionally, the design minimizes material loss during transfer, as the conveyor is engineered to capture and transfer all material from the tote bag, leaving minimal residue. This is particularly important for valuable or sensitive powders, where even small amounts of loss can impact profitability. The equipment is also designed for easy maintenance, with accessible components that allow for quick cleaning and repair, reducing downtime and maintenance costs.
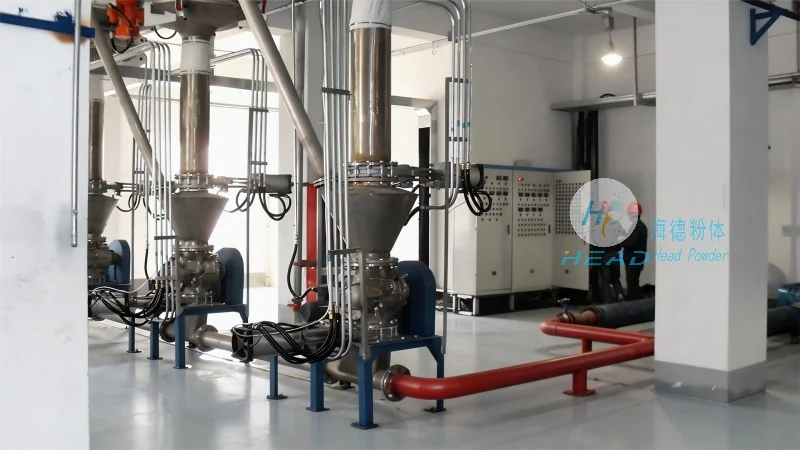
Tote bag unloading powder material conveyors are versatile and can be applied in a wide range of industries. In the chemical industry, these systems are used to transfer raw materials such as powders and granules into reactors or storage tanks. In the food and beverage industry, they are essential for handling ingredients like flour, sugar, and spices, ensuring that the products remain fresh and uncontaminated. The pharmaceutical industry also relies on these conveyors to handle active pharmaceutical ingredients (APIs) and excipients, maintaining strict hygiene and quality control standards. Additionally, in the mining and mineral processing sectors, tote bag unloading conveyors are used to transfer mined materials, such as ores and concentrates, into processing equipment. The adaptability of the system allows it to be customized to meet the specific requirements of each application, making it a valuable asset for any bulk material handling operation.
In summary, a tote bag unloading powder material conveyor is a critical piece of equipment for efficiently handling bulk powders in various industrial applications. The design principles, including the receiving hopper, discharge mechanism, and conveyor system, are engineered to ensure smooth and reliable material transfer. HeadPowder, with its expertise and commitment to quality, provides top-tier solutions that enhance operational efficiency, reduce costs, and maintain product integrity. For businesses seeking to optimize their powder handling processes, a tote bag unloading powder material conveyor from HeadPowder is a reliable and effective choice.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top