Limestone pneumatic conveying systems are industrial solutions designed to transport limestone powder or granules through a pipeline using air as the conveying medium. These systems are widely used in various industries, including chemical, cement, and mining, due to their efficiency and ability to handle bulk materials over long distances. The design of such equipment involves several key components and principles that ensure reliable and effective material transport. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in developing and supplying high-quality limestone pneumatic conveying systems tailored to meet the diverse needs of industrial clients.
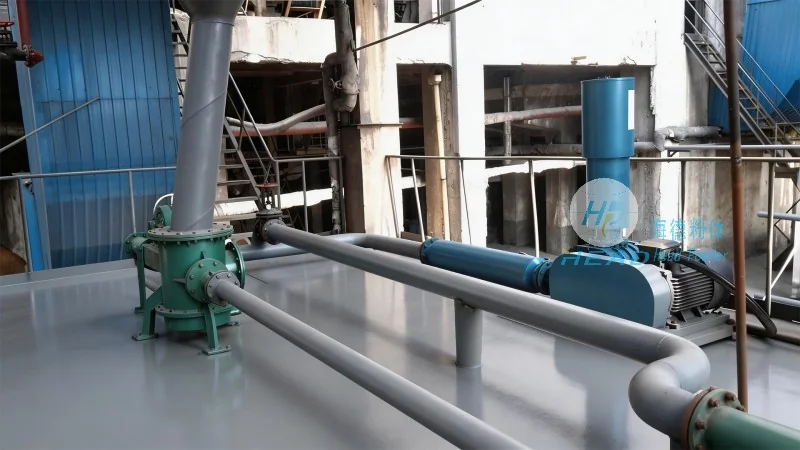
The core components of a limestone pneumatic conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a blower or compressor to generate the air flow, and a receiver for the discharged material. Each component plays a crucial role in the overall operation of the system. The hopper ensures a consistent supply of limestone, while the feeder regulates the material feed rate to match the air flow, preventing blockages or uneven flow. The conveying pipeline is designed with appropriate diameter and length to accommodate the material characteristics and the required conveying distance. The blower or compressor provides the necessary pressure and airflow to move the limestone particles through the pipeline. Finally, the receiver collects the conveyed material and may include features like a dust filter to ensure environmental compliance.
The design principles of limestone pneumatic conveying systems focus on optimizing material handling efficiency, minimizing energy consumption, and ensuring system reliability. One of the primary design considerations is the selection of the appropriate conveying method, which can be classified as dilute-phase or dense-phase. Dilute-phase systems use high air velocities to suspend the limestone particles, suitable for short to medium distances and low to medium material loads. Dense-phase systems, on the other hand, use lower air velocities and higher material concentrations, ideal for long-distance transport and handling of abrasive or sensitive materials. The choice between these methods depends on the specific application requirements, such as the distance between the source and destination, the material characteristics, and the desired flow rate.
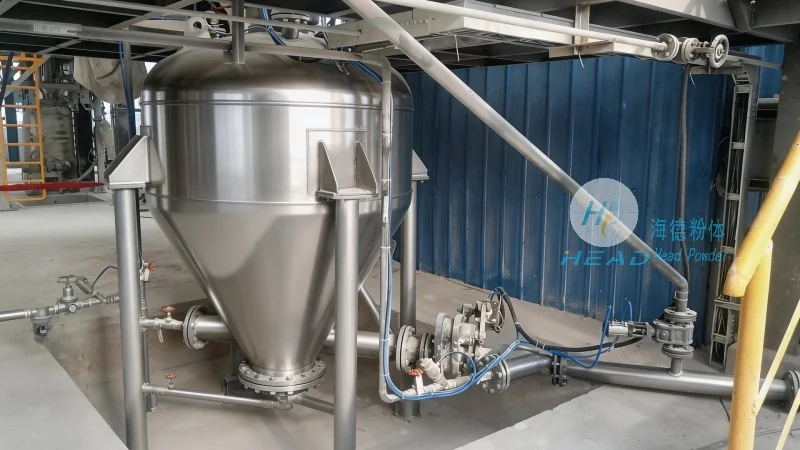
When designing a limestone pneumatic conveying system, several material handling factors must be considered to ensure optimal performance. The particle size and density of the limestone are critical parameters, as they affect the air velocity required for suspension and the risk of pipeline blockages. Larger or denser particles may require higher air velocities or different pipeline configurations to prevent settling or clogging. Additionally, the moisture content of the limestone can impact the system's efficiency, as excess moisture may cause the material to clump or stick to the pipeline walls, leading to reduced conveying capacity or increased maintenance needs. Proper material preparation, such as drying or screening, is often necessary to mitigate these issues and ensure smooth operation.
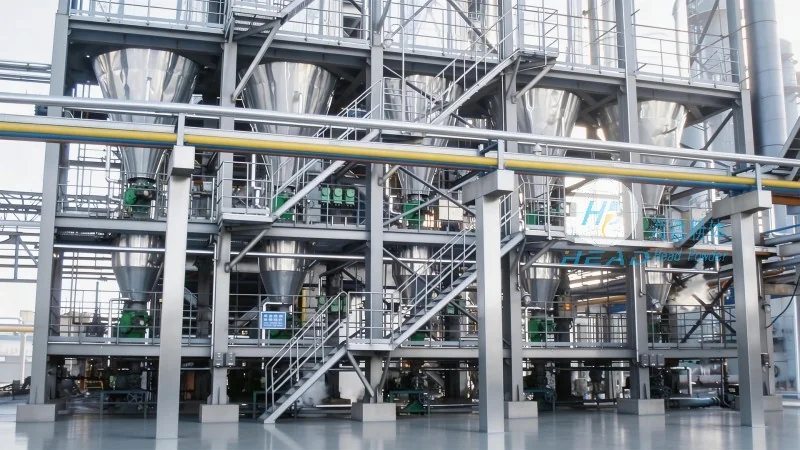
Optimizing the performance of a limestone pneumatic conveying system involves balancing several variables, including air pressure, flow rate, and material feed rate. The system's design must account for the specific material characteristics and the operational conditions to achieve the desired conveying capacity and efficiency. Regular maintenance and monitoring are essential to ensure the system operates within its design parameters and to identify any potential issues before they escalate. This includes checking the blower or compressor performance, inspecting the pipeline for blockages or wear, and verifying the feeder's operation to maintain consistent material flow. By implementing these optimization strategies, the system can achieve high reliability, low energy consumption, and minimal downtime, making it a cost-effective solution for limestone transport.
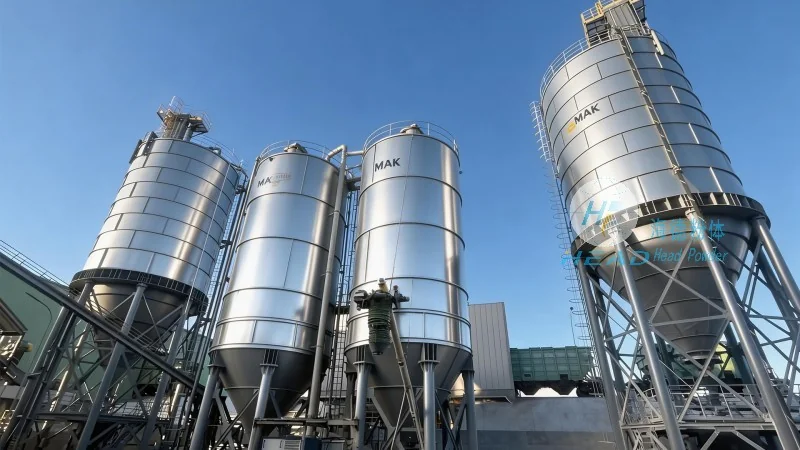
Limestone pneumatic conveying systems are utilized in a variety of industrial applications where the transport of bulk limestone is required. In the cement industry, these systems are commonly used to convey limestone from storage silos to cement production lines, ensuring a steady supply of raw material. In the chemical industry, they may be employed to transport limestone for processing into limestone-based products, such as calcium carbonate. Additionally, in mining operations, limestone pneumatic conveying can be used to transport crushed limestone from processing facilities to storage or shipping locations. The versatility of these systems makes them suitable for various applications, providing an efficient and reliable method for handling limestone in different industrial settings.
Limestone pneumatic conveying equipment plays a vital role in modern industrial operations by providing an efficient and reliable method for transporting bulk limestone. The design principles and components of these systems are carefully engineered to handle the specific characteristics of limestone, ensuring optimal performance and minimal operational issues. By understanding the key factors involved in the design and operation of such systems, industries can select and implement the most suitable solution for their material handling needs. As a result, limestone pneumatic conveying systems contribute significantly to the efficiency and productivity of various industrial processes, supporting the production of essential products like cement and other limestone-based materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top