Sulfur powder pneumatic conveying equipment is a specialized system designed to transport sulfur powder through the use of air or gas as the conveying medium. This technology is widely utilized in industrial settings where the efficient and safe handling of sulfur powder is critical. The equipment operates by creating a flow of air that carries the sulfur powder particles through a network of pipes and components, ensuring reliable material transfer from the source to the destination. Understanding the design principles behind such equipment is essential for optimizing performance, minimizing operational costs, and ensuring compliance with safety standards.
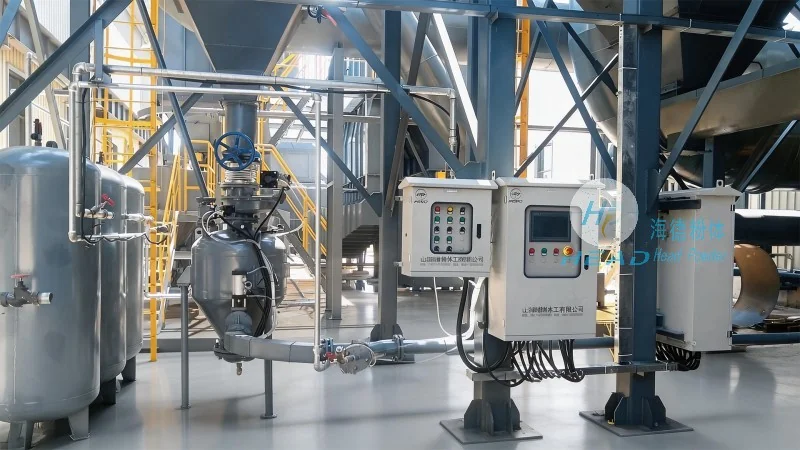
Sulfur powder, due to its fine particle size and potentially hazardous nature, requires specialized handling equipment to prevent dust explosions and ensure consistent material flow. The pneumatic conveying system addresses these challenges by utilizing compressed air or other gases to transport the powder. This method is preferred over traditional mechanical conveying systems in many applications because it eliminates the need for moving parts in the conveying line, reducing maintenance requirements and enhancing safety. The equipment typically consists of several key components, including a feeding device, a blower or compressor, a conveying pipeline, a separation unit, and a collection system. Each component plays a crucial role in the overall operation of the system, working in tandem to achieve efficient material transfer.
The design of sulfur powder pneumatic conveying equipment is based on several fundamental principles to ensure optimal performance and safety. The primary principle is the creation of a stable air flow that can effectively lift and transport the powder particles. This is achieved by controlling the air velocity and pressure within the system. The air velocity must be sufficient to overcome the gravitational forces acting on the powder particles and to maintain the powder in a suspended state. Typically, the air velocity in the conveying line is maintained at a level that is higher than the terminal velocity of the powder particles, ensuring that they remain suspended and are carried along with the air stream.
Another critical design principle is the selection of appropriate equipment materials to prevent corrosion and chemical reactions with the sulfur powder. Sulfur powder can be corrosive, especially when it contains moisture or other impurities. Therefore, the equipment components, such as the feeding hopper, pipelines, and separation units, are often constructed from materials like stainless steel, polyethylene, or other corrosion-resistant alloys. This choice of materials ensures the longevity of the equipment and maintains the purity of the sulfur powder during transport.
The system design also considers the pressure and flow characteristics of the conveying medium. There are two main types of pneumatic conveying systems: pressure and vacuum. In pressure systems, the air is compressed and introduced at the discharge end of the pipeline, pushing the powder forward. In vacuum systems, the air is drawn from the receiving end, creating a negative pressure that pulls the powder into the pipeline. The choice between these systems depends on the distance to be covered, the volume of material to be transported, and the layout of the facility. For sulfur powder, pressure systems are often preferred due to their ability to handle longer distances and larger volumes with less energy consumption.
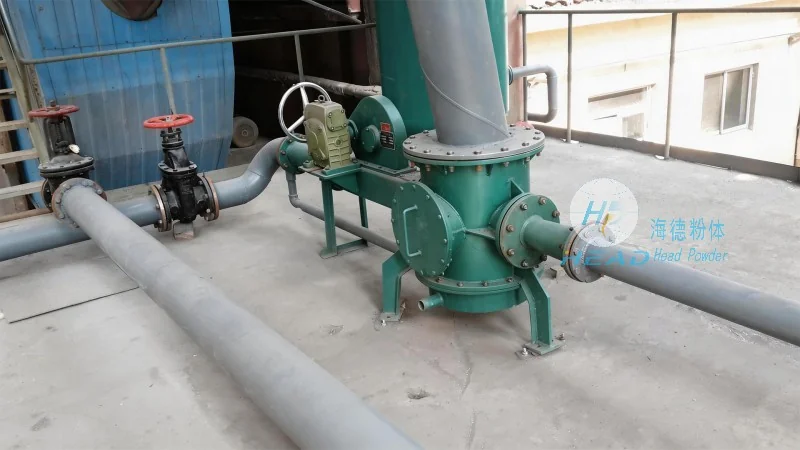
The sulfur powder pneumatic conveying equipment comprises several key components, each with a specific function to ensure the smooth operation of the system. The feeding device is responsible for introducing the sulfur powder into the conveying line. This component can be a rotary valve, a star feeder, or a pressure feeder, depending on the application. The feeding device must be designed to handle the specific characteristics of sulfur powder, such as its flowability and potential for bridging or caking. Proper feeding ensures a consistent flow of powder into the system, preventing blockages and maintaining system efficiency.
The blower or compressor is the heart of the pneumatic conveying system, providing the necessary air pressure and volume to transport the powder. The selection of the blower type (centrifugal, positive displacement, or rotary lobe) depends on the system requirements, including the required air flow rate, pressure, and power consumption. The blower must be capable of generating sufficient pressure to overcome the resistance in the pipeline and to lift the powder particles. It is also important to consider the noise level and maintenance requirements of the blower, as these factors impact the overall operational costs and user experience.
The conveying pipeline is a network of pipes that connects the feeding device to the separation unit and the collection system. The pipeline is typically made of materials like stainless steel, polyethylene, or PVC, depending on the system design and the properties of the sulfur powder. The diameter and length of the pipeline are critical design parameters, as they affect the air velocity and pressure drop within the system. Proper sizing of the pipeline ensures that the air velocity remains within the optimal range, preventing excessive energy consumption or insufficient powder transport.
The separation unit, also known as a cyclone or a filter, is responsible for separating the sulfur powder from the air stream at the end of the conveying line. The separation process is based on the principle of centrifugal force, where the heavier powder particles are forced to the wall of the cyclone and fall to the collection hopper, while the air is discharged through the top of the unit. The design of the separation unit is crucial for achieving high separation efficiency, minimizing dust emissions, and preventing powder loss. The separation efficiency is typically measured by the percentage of powder recovered from the air stream, and it is an important parameter in evaluating the performance of the system.
The collection system is the final component of the pneumatic conveying equipment, responsible for storing the separated sulfur powder. The collection hopper is usually designed with a discharge valve or a rotary valve to allow the powder to be discharged into a storage silo or a processing unit. The collection system must be designed to prevent dust leakage and to maintain the purity of the sulfur powder. The hopper is often equipped with a dust collection system, such as a bag filter or an electrostatic precipitator, to capture any residual dust particles before the air is released to the atmosphere.
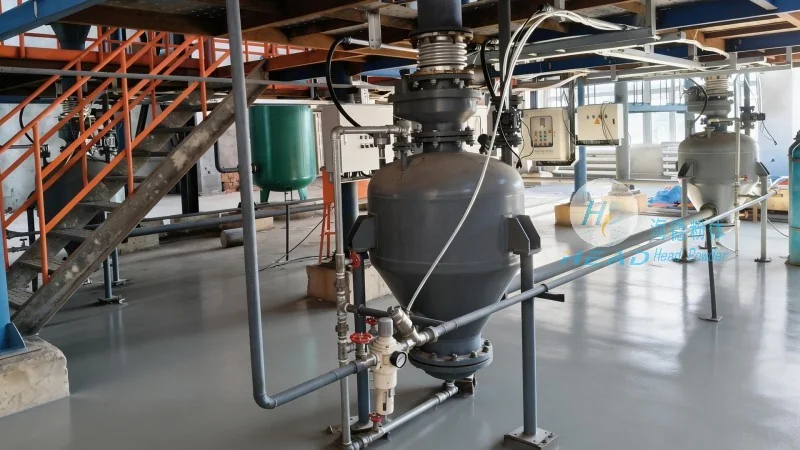
Proper operation and maintenance of sulfur powder pneumatic conveying equipment are essential to ensure its long-term performance and reliability. Regular maintenance is required to keep the system in optimal condition, including cleaning the feeding device, checking the blower performance, inspecting the pipeline for blockages or leaks, and maintaining the separation unit. The feeding device should be cleaned regularly to prevent caking or bridging of the sulfur powder, which can lead to system downtime. The blower should be checked for wear and tear, and the air filter should be replaced as needed to maintain the required air quality.
The pipeline should be inspected for any signs of corrosion or damage, and any leaks should be repaired immediately to prevent air loss and reduce energy consumption. The separation unit should be cleaned periodically to maintain its efficiency, as accumulated powder can reduce the separation efficiency and increase the risk of dust emissions. The collection system should be checked for any signs of leakage or blockage, and the discharge valve should be operated correctly to prevent powder spillage.
Operational considerations also include the control of air pressure and flow rate. The system should be operated at the optimal air pressure and flow rate to ensure efficient powder transport and minimize energy consumption. The air pressure should be adjusted based on the distance to be covered and the volume of material to be transported. The flow rate should be monitored to ensure that the system is not overloaded, which can lead to increased pressure drop and reduced separation efficiency.
Sulfur powder pneumatic conveying equipment is a critical component in industrial applications where the efficient and safe handling of sulfur powder is required. The design principles behind such equipment are based on the creation of a stable air flow, the selection of appropriate materials, and the optimization of system components to achieve reliable material transfer. The key components, including the feeding device, blower, conveying pipeline, separation unit, and collection system, each play a crucial role in the overall operation of the system. Proper operation and maintenance are essential to ensure the long-term performance and reliability of the equipment. By understanding the design principles and operational considerations, industrial facilities can optimize their sulfur powder handling processes, reduce operational costs, and enhance safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top