For industries dealing with bulk powder handling, efficient and reliable material transport is crucial. A powder silo pneumatic conveying equipment system offers a solution that combines storage and transport capabilities, ensuring smooth operations from raw material intake to processing. This article explores the fundamental aspects of such equipment, focusing on its design principles and the role it plays in modern industrial processes.
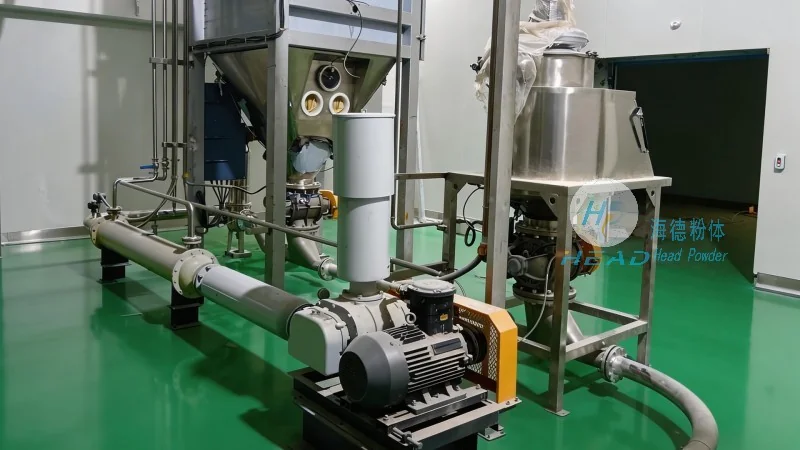
A powder silo pneumatic conveying system is a specialized device designed to store, transport, and distribute bulk powders through an air-driven mechanism. The system typically integrates a storage silo, a conveying pipeline, and a control unit, enabling the seamless movement of materials without the need for mechanical components like belts or buckets. This approach not only reduces maintenance costs but also minimizes the risk of material contamination, making it ideal for applications in pharmaceuticals, food processing, and chemical manufacturing.
The effectiveness of a powder silo pneumatic conveying system relies on its well-designed components, each playing a critical role in the overall operation. The primary components include the powder silo, which serves as the storage vessel, the air compressor or blower that generates the necessary airflow, the conveying pipeline that transports the material, and the control system that regulates the process. Additionally, features like dust collectors and material separators may be incorporated to enhance efficiency and safety.
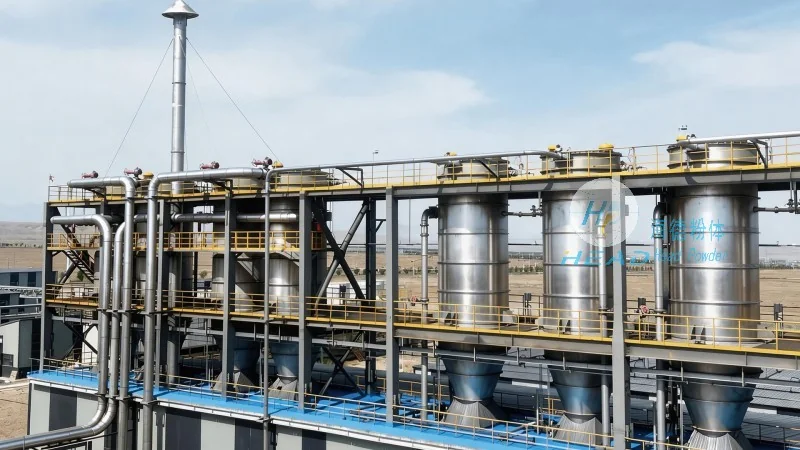
The design of a powder silo pneumatic conveying system is guided by several key principles aimed at optimizing performance, energy efficiency, and material handling. One of the core principles is the use of appropriate air velocity and pressure to ensure the material is entrained and transported effectively without causing excessive wear on the equipment. The system must also consider the properties of the powder being handled, such as particle size, density, and flowability, as these factors directly impact the conveying efficiency. Furthermore, the design incorporates safety measures, including pressure relief valves and explosion-proof components, to protect against potential hazards associated with powder handling.
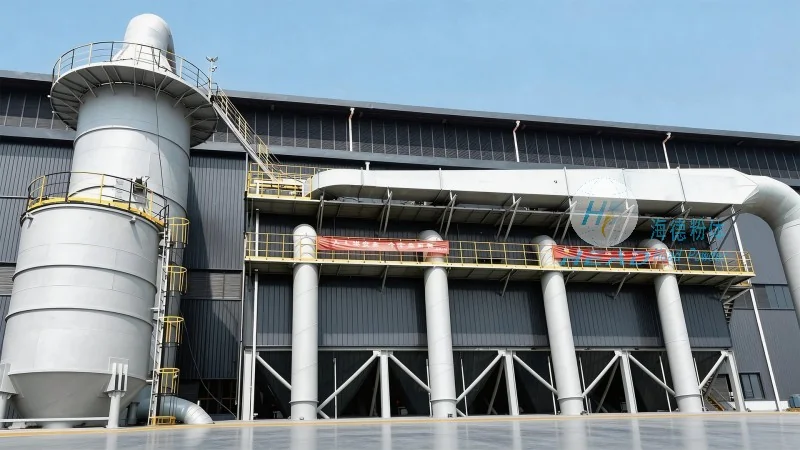
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling equipment, specializes in developing customized solutions tailored to the unique needs of various industries. With a focus on innovation and quality, the company designs and manufactures powder silo pneumatic conveying systems that meet stringent industry standards. The company's expertise lies in understanding the specific requirements of each application, from material characteristics to operational constraints, ensuring that the final product is both efficient and reliable. HeadPowder's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the field of bulk powder handling.
In conclusion, a powder silo pneumatic conveying equipment system is a vital asset for industries that rely on bulk powder transport. Its design, which integrates storage and air-driven transport, offers numerous advantages over traditional methods. By adhering to sound design principles and leveraging the expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd., businesses can achieve enhanced operational efficiency, reduced downtime, and improved product quality. As the demand for efficient powder handling solutions continues to grow, the importance of well-designed pneumatic conveying systems cannot be overstated.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top