Bulk bag pneumatic conveying systems are advanced industrial solutions designed to efficiently transfer bulk materials from one location to another. These systems are particularly popular in industries such as food processing, pharmaceuticals, and chemical manufacturing due to their ability to handle large volumes of powders and granules while maintaining high levels of cleanliness and safety. The core of these systems lies in the seamless integration of bulk bags with pneumatic conveying technology, offering a cost-effective and flexible approach to material handling. In today's competitive manufacturing landscape, the need for efficient and reliable material transfer has never been greater, making bulk bag pneumatic conveying systems an essential tool for many businesses.
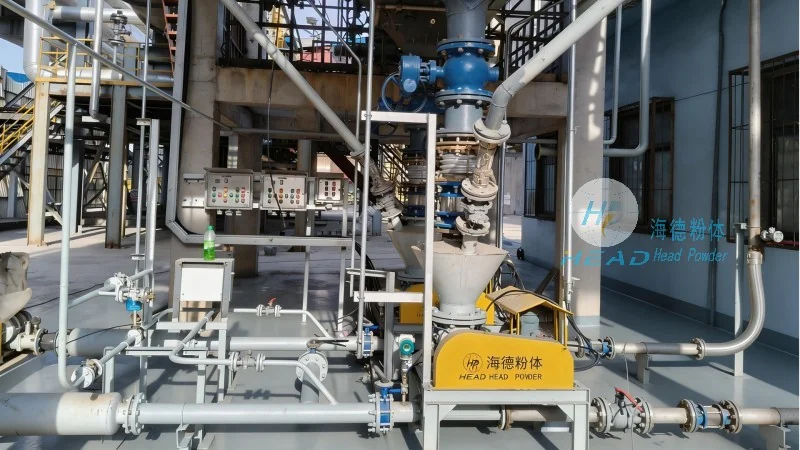
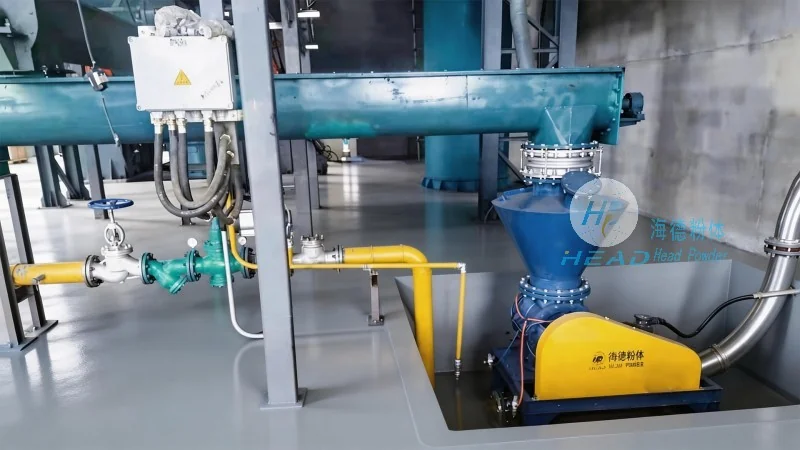
At the heart of any bulk bag pneumatic conveying system are several critical components that work in tandem to ensure smooth operation. The primary elements include the bulk bag itself, which serves as the container for the material; a hopper or feeder that regulates the flow of material from the bag; a conveying line that transports the material through the system; and a receiver or discharge unit where the material is deposited. Additionally, a vacuum or pressure source, such as a blower or compressor, provides the necessary force to move the material through the system. The design of each component is crucial for optimizing performance and minimizing downtime. For example, the bulk bag is typically made of durable, food-grade or industrial-grade materials to withstand the weight and handling of the material. The hopper is designed with a sloped bottom to facilitate the flow of material, preventing clogging and ensuring consistent discharge. The conveying line is usually made of stainless steel or other corrosion-resistant materials to handle various material types and prevent contamination. The receiver is equipped with a discharge valve or other mechanism to control the release of material, ensuring precise and controlled delivery.
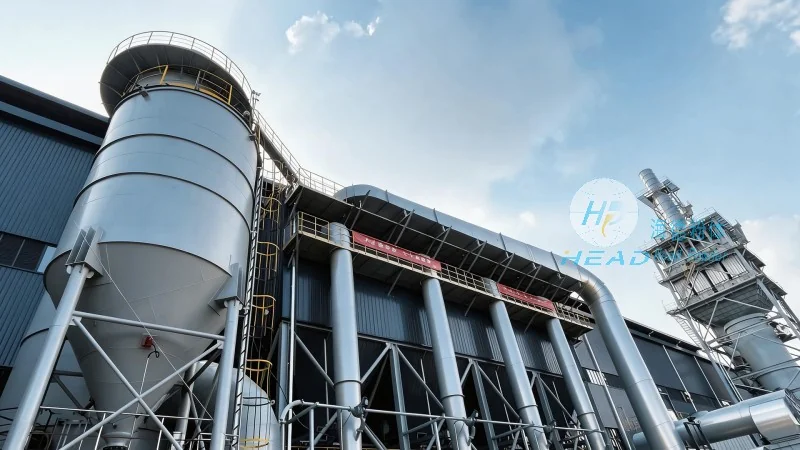
The design principles of bulk bag pneumatic conveying systems are centered on efficiency, reliability, and adaptability. Engineers focus on several key factors to ensure optimal performance. First, the system must be capable of handling a wide range of material properties, including different particle sizes, densities, and flow characteristics. This requires careful selection of the conveying line material and the type of air flow (e.g., vacuum or pressure) to prevent material degradation or blockages. For instance, materials with high moisture content may require a pressure system to prevent clumping, while lighter, finer powders may benefit from a vacuum system to avoid dust dispersion. Second, the system should minimize material loss and contamination, which is critical in industries like pharmaceuticals and food processing. This is achieved through the use of sealed bulk bags and enclosed conveying lines that prevent dust and particles from escaping into the environment. The use of filters and dust collection systems further enhances the system's ability to maintain a clean environment. Third, the design must consider energy efficiency and operational costs. Modern systems often incorporate variable speed drives and energy recovery mechanisms to reduce power consumption while maintaining performance. This not only lowers the system's carbon footprint but also reduces long-term operational expenses. Finally, the system must be easy to maintain and clean, with accessible components that can be quickly serviced without disrupting production. The modular design of many systems allows for easy replacement of parts and cleaning of the conveying line, minimizing downtime and ensuring consistent performance.
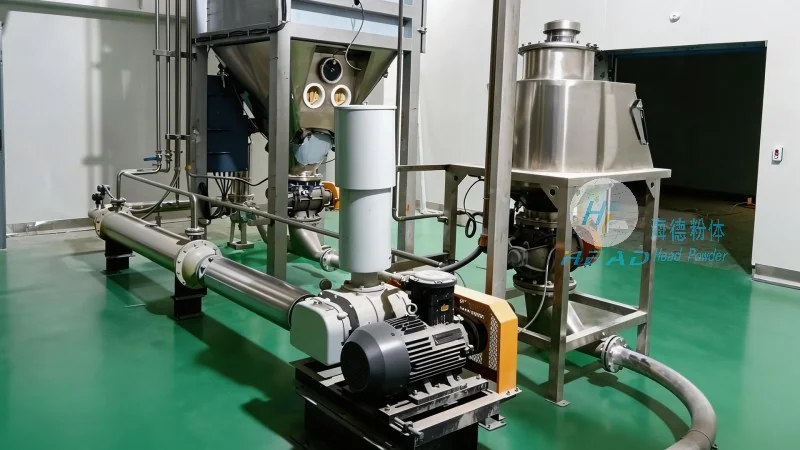
Understanding the operational mechanics of a bulk bag pneumatic conveying system is essential for appreciating its functionality. The process typically begins with the bulk bag being filled with the desired material. Once filled, the bag is placed in the hopper or feeder, which is connected to the conveying line. The system then uses a vacuum or pressure source to create airflow through the line. As the air flows, it lifts the material from the bag and transports it through the conveying line to the receiver. The material is then discharged into the receiver, where it can be further processed or stored. The entire process is automated, with sensors and controls ensuring that the system operates within safe and efficient parameters. For example, pressure sensors monitor the air pressure in the conveying line, while flow meters track the rate of material transfer. These sensors provide real-time data to the control system, allowing for adjustments to be made if the system deviates from optimal performance. This automated approach not only improves productivity but also reduces the risk of human error and exposure to hazardous materials. The system's ability to operate continuously without manual intervention makes it ideal for 24/7 production environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top