Diatomite, a natural sedimentary rock composed of fossilized diatoms, is widely utilized across various industrial sectors due to its distinctive properties such as high porosity, superior filtration capabilities, and lightweight characteristics. The efficient handling and transportation of diatomite are critical for industrial processes, and pneumatic conveying systems have emerged as a reliable solution for this purpose. This article provides an overview of diatomite pneumatic conveying equipment, focusing on its structural design and operational principles.
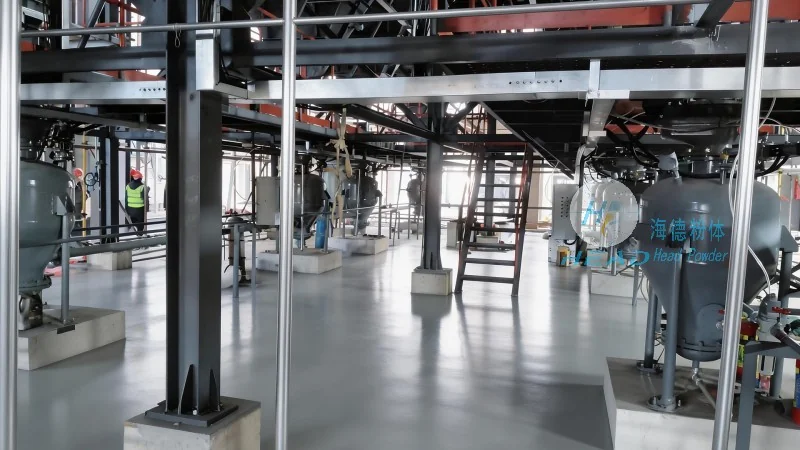
HeadPowder, a leading manufacturer in the field, specializes in the design and production of advanced pneumatic conveying systems tailored for diatomite handling. The company's expertise lies in developing equipment that ensures minimal product degradation, high efficiency, and low maintenance costs. The diatomite pneumatic conveying system typically comprises several key components, including a hopper, feeder, air compressor, conveying line, and receiver. Each component plays a vital role in the overall operation, ensuring smooth and continuous material transport.
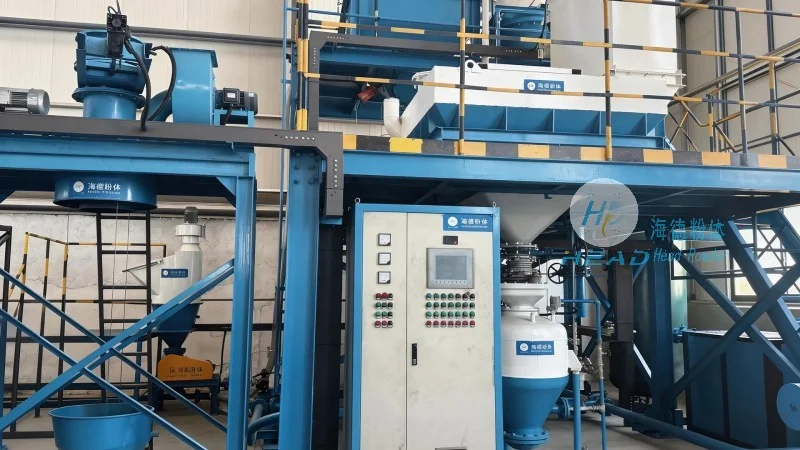
The structural design of a diatomite pneumatic conveying system is engineered to accommodate the specific characteristics of diatomite, such as its fine particle size and low bulk density. The hopper is designed with a wide opening to accommodate bulk diatomite and prevent clogging. The feeder, often a rotary valve or screw feeder, regulates the flow of diatomite into the conveying line, ensuring a consistent feed rate. The air compressor provides the necessary pressure to transport the material through the pipeline. The conveying line is typically constructed from stainless steel or other corrosion-resistant materials to prevent diatomite from adhering to the walls and causing blockages. The receiver collects the diatomite at the destination, allowing for easy discharge.
HeadPowder's diatomite pneumatic conveying equipment offers several advantages over traditional methods like belt conveyors or bucket elevators. The primary benefits include reduced product contamination, as the material is transported in an enclosed system, preventing exposure to dust and other contaminants. Additionally, the system minimizes labor costs and energy consumption by automating the conveying process. The compact design of the equipment makes it suitable for installation in limited spaces, and the low maintenance requirements ensure long-term operational reliability. The system also provides flexibility in terms of conveying distance and layout, allowing for easy integration into existing industrial setups.
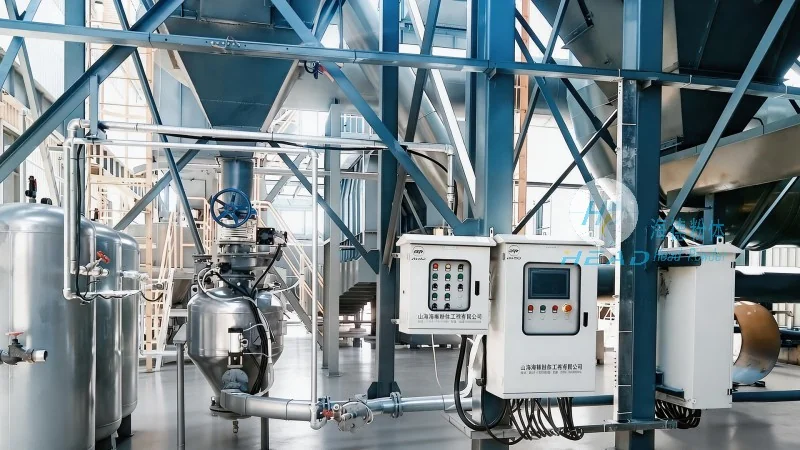
The diatomite pneumatic conveying system is widely used in industries such as water treatment, food processing, and pharmaceuticals. In water treatment plants, diatomite is used as a filter media to remove impurities from water. The conveying system efficiently transports the diatomite from storage to the filtration tanks, ensuring consistent filtration performance. In food processing, diatomite is used as a clarifying agent in beverages and as a filter aid in juice production. The system ensures that the diatomite is delivered to the processing lines without any loss or contamination. In the pharmaceutical industry, diatomite is used as a filtration aid in the production of sterile liquids. The enclosed conveying system maintains the sterility of the material, preventing any contamination during transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top