Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions, focuses on optimizing the transport of food additives through advanced pneumatic conveying technologies. Based in Shandong, China, the company leverages decades of industry experience to deliver efficient, safe, and reliable systems tailored to the unique demands of the food processing sector. This article explores the application and optimization strategies for pneumatic conveying in food additive transport, highlighting key benefits and practical implementation considerations.
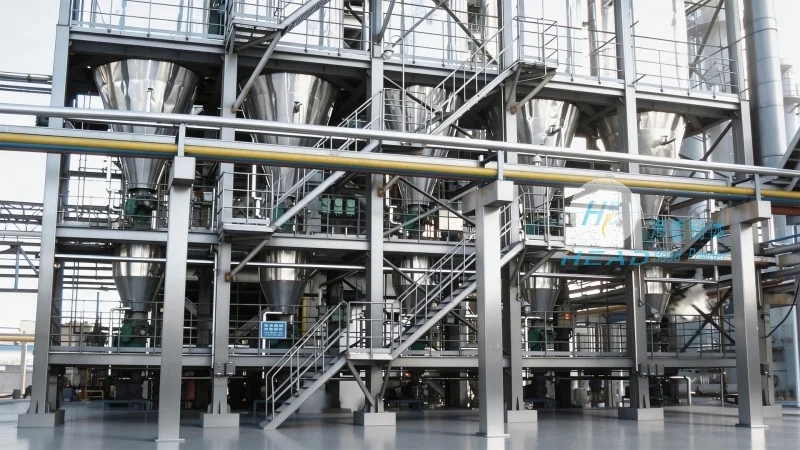
Pneumatic conveying is a method of transporting bulk materials, including food additives, using a stream of pressurized air or vacuum. Unlike traditional mechanical systems like screw conveyors or belt conveyors, pneumatic systems offer advantages such as reduced contamination risk, improved hygiene compliance, and the ability to handle a wide range of particle sizes and moisture contents. For food additives, which often require strict control over purity and contamination, pneumatic conveying provides a hygienic and efficient solution. The technology works by creating a pressure differential that propels the material through a pipeline, ensuring minimal contact with external surfaces and maintaining product integrity throughout the transport process.
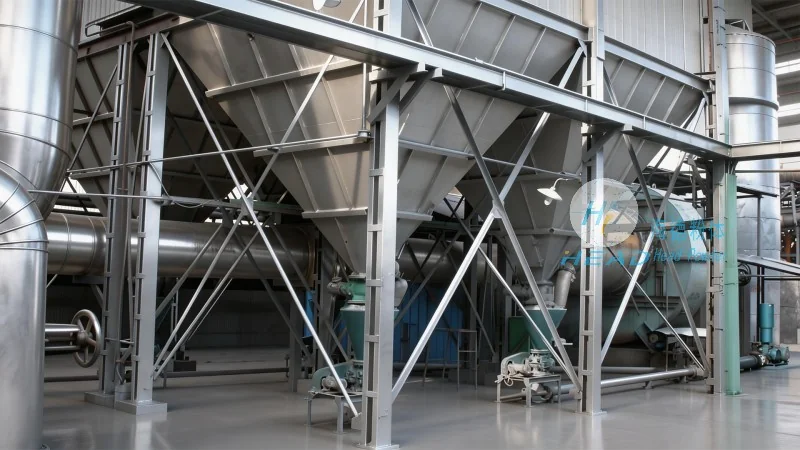
Implementing pneumatic conveying for food additives offers several critical advantages that enhance operational efficiency and product quality. First, the hygienic design of pneumatic systems minimizes the risk of cross-contamination, which is paramount in food processing environments. The enclosed pipelines and sealed components prevent exposure to external contaminants, ensuring that additives remain pure and meet regulatory standards. Second, pneumatic conveying is highly flexible, allowing for vertical, horizontal, or mixed-direction transport of materials. This flexibility enables manufacturers to design layouts that optimize space utilization and streamline production workflows. Third, the technology reduces labor costs by automating material handling processes, eliminating the need for manual loading and unloading of bulk additives. Additionally, pneumatic systems can handle materials with varying flow properties, including powders, granules, and even fine particles, making them suitable for a broad spectrum of food additives such as colorants, flavor enhancers, and preservatives.
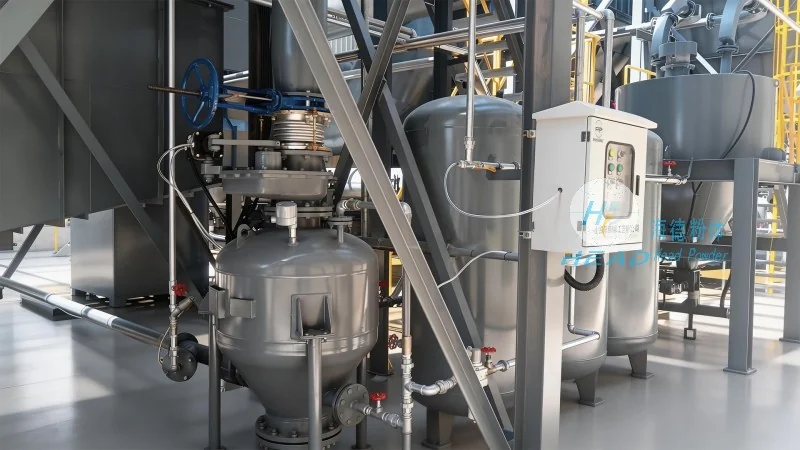
To maximize the effectiveness of pneumatic conveying in food additive transport, several optimization strategies are essential. First, proper system design is critical. This includes selecting the appropriate air velocity, pipeline diameter, and pressure levels to ensure efficient material transport while minimizing energy consumption. For example, higher air velocities may be required for fine powders to prevent clogging, whereas lower velocities are suitable for larger granules to reduce wear on components. Second, the integration of advanced control systems enhances operational efficiency. Automated controls allow for real-time monitoring of flow rates, pressure, and temperature, enabling immediate adjustments to maintain optimal performance. This not only improves productivity but also extends the lifespan of system components. Third, regular maintenance and cleaning protocols are vital to maintain hygiene standards. Pneumatic systems should be designed with easy-to-clean components, such as CIP (Clean-In-Place) compatible parts, to facilitate routine sanitation. This ensures that the system remains compliant with food safety regulations and prevents the buildup of residues that could affect product quality.
A practical example of pneumatic conveying optimization is demonstrated by a client in the food processing industry. The client, a manufacturer of dairy products, required a solution to transport powdered flavor enhancers from storage silos to production lines without compromising product purity. By implementing a customized pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd., the client achieved significant improvements. The system was designed with stainless steel pipelines and hygienic fittings, ensuring compliance with food safety standards. The air velocity was optimized to prevent clogging while maintaining a low energy consumption rate. As a result, the client experienced a 30% reduction in transport time and a 20% decrease in labor costs associated with manual handling. Additionally, the system’s flexibility allowed for easy integration with existing production lines, minimizing downtime during installation. This case study illustrates how tailored pneumatic conveying solutions can deliver measurable benefits in terms of efficiency, cost savings, and product quality.
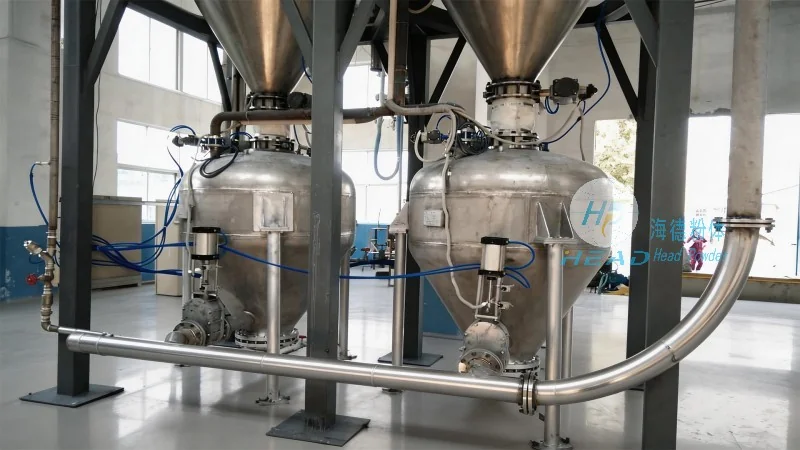
As the food industry continues to prioritize efficiency, safety, and compliance, pneumatic conveying technology remains a cornerstone of food additive transport systems. Shandong HeadPowder Engineering Co., Ltd. plays a pivotal role in advancing this technology by providing customized solutions that address the unique challenges of the food processing sector. By focusing on optimization strategies such as system design, advanced controls, and regular maintenance, manufacturers can leverage pneumatic conveying to enhance operational performance and maintain product integrity. The benefits of reduced contamination risk, flexibility, and cost savings make pneumatic conveying an indispensable tool for modern food additive transport. For businesses seeking to improve their material handling processes, pneumatic conveying offers a reliable and efficient solution that aligns with industry standards and regulatory requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top