When it comes to the efficient handling and transportation of wheat bran, selecting the right conveying method is crucial for optimizing production processes and ensuring operational efficiency. This article provides a detailed comparison of common wheat bran conveying methods, highlighting their advantages and disadvantages to help industrial operators make informed decisions.
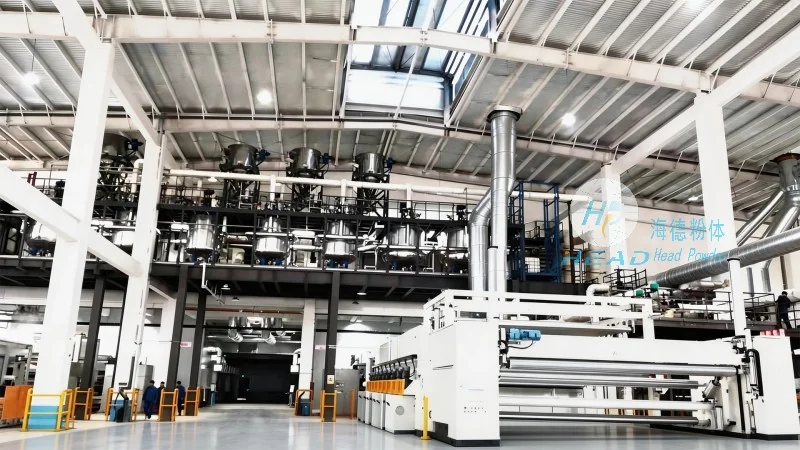
Wheat bran, a byproduct of wheat milling, is widely used in animal feed, food processing, and other industrial applications. The effective conveyance of this material requires systems that can handle its unique characteristics, such as bulk density, flowability, and potential for dust generation. Several methods are commonly employed in industrial settings, each with its own set of benefits and limitations.
Screw conveyors, also known as auger conveyors, are one of the most widely used equipment for transporting wheat bran. These systems consist of a rotating helical screw inside a tube or trough, which moves material from one point to another through gravitational force and the rotation of the screw. The advantages of screw conveyors include their simplicity, low maintenance requirements, and ability to handle a wide range of materials, including wheat bran with varying moisture content. They are particularly effective for horizontal or slightly inclined applications, making them suitable for short to medium distance conveying. However, screw conveyors have limitations when dealing with high-volume or abrasive materials, as the screw and trough can experience wear over time. Additionally, they may not be ideal for long vertical lifts due to the risk of material clogging or excessive power consumption.
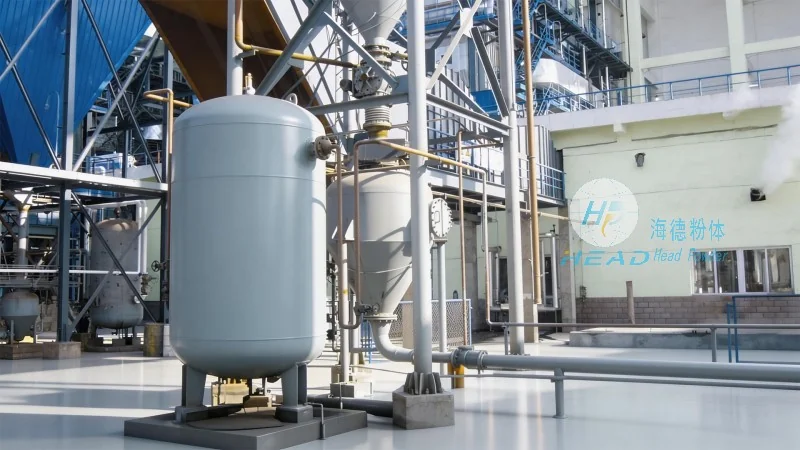
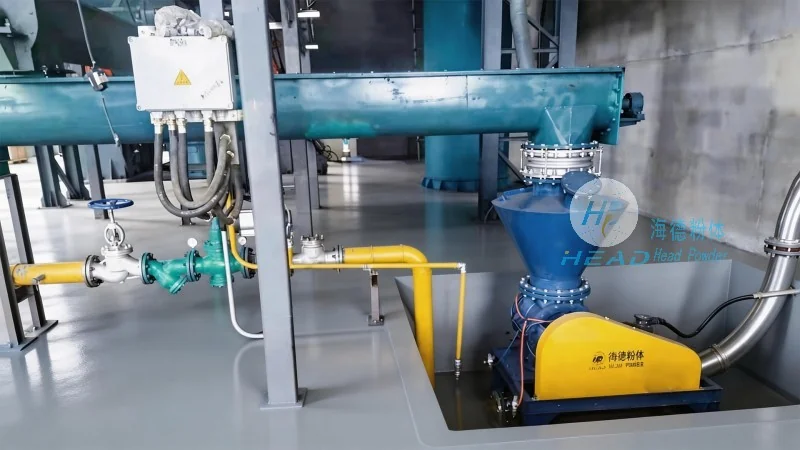
Pneumatic conveying systems use air or gas to transport wheat bran through a pipeline network. These systems can be categorized into pressure and vacuum types, each offering different capabilities. Pressure systems push material using compressed air, while vacuum systems pull material using a vacuum pump. The primary advantage of pneumatic conveying is its ability to transport wheat bran over long distances and through complex layouts, including vertical lifts. This method is also suitable for handling fine or dusty materials, as the enclosed pipeline prevents dust dispersion. However, pneumatic conveying requires significant energy input, as the air velocity must be maintained to prevent material settling. Moreover, the system can be prone to blockages if the bran is too moist or contains large particles, leading to increased maintenance and operational costs.
Belt conveyors utilize a continuous belt to transport wheat bran, making them suitable for both horizontal and inclined applications. These systems are commonly used in bulk material handling and can handle high volumes of wheat bran efficiently. The advantages of belt conveyors include their high capacity, low maintenance, and ability to transport materials over long distances. They are particularly effective for applications requiring continuous material flow, such as in feed mills or flour processing plants. However, belt conveyors have limitations when dealing with abrasive or sticky wheat bran, as the belt and pulleys can experience wear and tear. Additionally, they may not be suitable for vertical lifts due to the risk of material slipping or the need for complex pulley systems.
Bucket elevators are vertical conveying systems that use a series of buckets attached to a belt or chain to lift wheat bran from a lower to a higher level. These systems are highly efficient for vertical transport and can handle large volumes of material with minimal space requirements. The advantages of bucket elevators include their high lifting capacity, low energy consumption for vertical lifts, and ability to transport materials over long vertical distances. They are particularly suitable for applications where vertical space is limited or where the material needs to be elevated to a significant height. However, bucket elevators have limitations when dealing with fine or dusty wheat bran, as the buckets can accumulate material and cause blockages. Additionally, they require regular maintenance to ensure the buckets and drive system operate smoothly.
Hydraulic conveying systems use water or other fluids to transport wheat bran through a pipeline. The material is suspended in the fluid and moved along the pipeline by the flow of the liquid. The advantages of hydraulic conveyors include their ability to handle high volumes of material and transport it over long distances with minimal energy input. They are particularly effective for applications where the material is wet or contains a high moisture content. However, hydraulic conveying has significant limitations, as the system requires a large amount of water and energy to operate. The fluid must be continuously recycled, which adds to the maintenance and operational costs. Additionally, the system can be prone to clogging if the wheat bran contains large particles or is too dry, leading to reduced efficiency.
Choosing the right wheat bran conveying method depends on several factors, including the distance to be covered, the volume of material, the vertical or horizontal nature of the transport, and the material's characteristics. For short horizontal distances and moderate volumes, screw conveyors are often the most cost-effective option. For long distances or complex layouts, pneumatic conveying systems may be more suitable. Belt conveyors are ideal for high-capacity horizontal transport, while bucket elevators are preferred for vertical lifting. Hydraulic conveyors are best suited for wet or high-moisture applications but require careful consideration of operational costs.
Industrial operators should evaluate their specific needs and consider the advantages and disadvantages of each method before making a decision. By selecting the appropriate conveying system, they can improve operational efficiency, reduce maintenance costs, and ensure the safe and effective handling of wheat bran. For more information on wheat bran conveying solutions, contact Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top