HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for the cereal industry. This article provides a comprehensive overview of the classification of these systems and their practical applications, highlighting the technical solutions that enhance efficiency and reliability in grain handling operations.
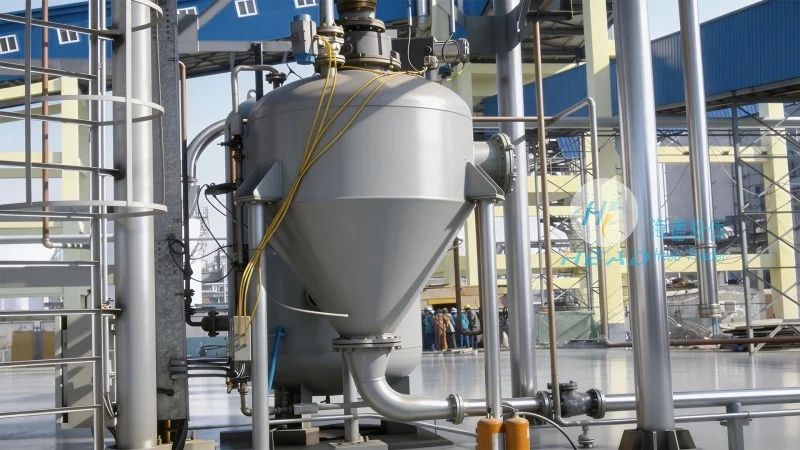
The classification of cereal pneumatic conveying systems is primarily based on the method of air flow and the type of material transport. Two main categories are commonly recognized: dilute-phase and dense-phase systems. Dilute-phase systems utilize low air-to-material ratios, where the material is suspended in the air stream, allowing for high-speed transport over long distances. This method is ideal for transporting fine or free-flowing cereals such as wheat, corn, and oats. Dense-phase systems, on the other hand, employ higher air-to-material ratios, creating a slurry-like mixture where the material moves in a more controlled manner. This approach is particularly suitable for handling sticky or abrasive cereals that require gentler handling to prevent product degradation or equipment wear.
Both dilute-phase and dense-phase systems consist of several critical components that work in tandem to ensure effective material transport. The primary components include a material feeder, a conveying line (often equipped with bends and expansion joints), a dust separator or cyclone, and a receiver or storage tank. The material feeder, typically a rotary valve or a screw feeder, ensures a consistent and controlled flow of cereal into the system. The conveying line, which may be made of metal or flexible tubing, transports the material and air mixture. The dust separator, such as a cyclone or bag filter, separates the air from the material, allowing the air to be recirculated or discharged while the cereal is collected in the receiver. The receiver then stores the transported cereal until it is ready for further processing or packaging.
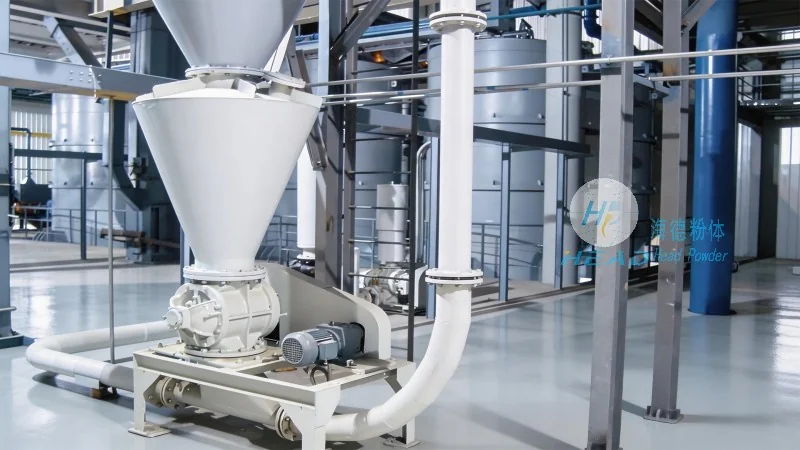
Cereal pneumatic conveying systems are widely used across various stages of the cereal production and processing chain. In the raw material handling stage, these systems efficiently transport bulk cereals from storage silos or trucks to processing facilities, minimizing manual handling and reducing the risk of contamination. During the processing stage, they are employed to move cereals through cleaning, sorting, and milling operations, ensuring that each step is performed with precision and minimal loss. In the packaging stage, the systems transfer finished products to packaging lines, enabling seamless integration with automated packaging equipment. Additionally, these systems are utilized in the distribution phase, where cereals are transported from processing plants to distribution centers or retail outlets, maintaining product integrity and freshness throughout the supply chain.
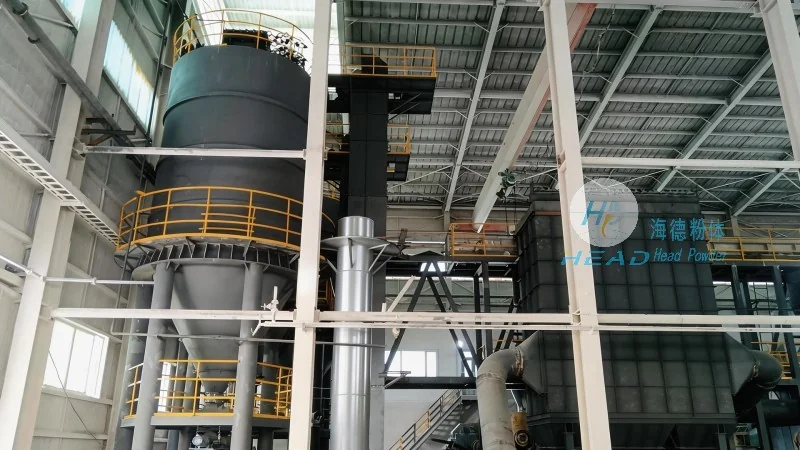
Compared to traditional mechanical conveying methods, cereal pneumatic conveying systems offer several advantages that make them a preferred choice in the industry. One of the most significant benefits is the ability to handle a wide range of cereal types, from fine powders to bulk grains, without the need for additional equipment or modifications. The systems are also highly flexible, allowing for easy reconfiguration to accommodate changes in production volumes or product lines. Furthermore, pneumatic conveying systems are more hygienic and cleaner than mechanical systems, as they minimize product contact with metal surfaces and reduce the risk of cross-contamination. This is particularly important in the food industry, where product safety and quality are paramount. Additionally, these systems are energy-efficient, as they can be optimized to use minimal air pressure and power, reducing operational costs and environmental impact.
HeadPowder Engineering Co., Ltd. provides comprehensive customization and integration services to meet the specific needs of cereal processing facilities. The company’s engineers work closely with clients to design systems that are tailored to their unique production requirements, including the type of cereal being handled, the distance of transport, and the desired level of automation. HeadPowder offers a range of standard and custom-designed components, such as specialized feeders, high-efficiency dust separators, and flexible conveying lines, to ensure optimal performance. The company also provides installation, commissioning, and maintenance services to ensure that the systems operate at peak efficiency throughout their lifecycle. By leveraging advanced engineering and manufacturing capabilities, HeadPowder delivers reliable and durable pneumatic conveying solutions that enhance productivity and reduce downtime for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top