Micro-powder pneumatic conveying systems are integral to modern industrial operations, enabling the efficient transport of fine powders with particle sizes typically ranging from 1 to 500 micrometers. These systems are designed to handle materials that often present unique challenges, such as dust generation, particle cohesion, and the need for minimal product degradation. The classification of micropowder pneumatic conveying systems is essential for understanding their operational principles and selecting the most suitable technology for specific industrial applications.
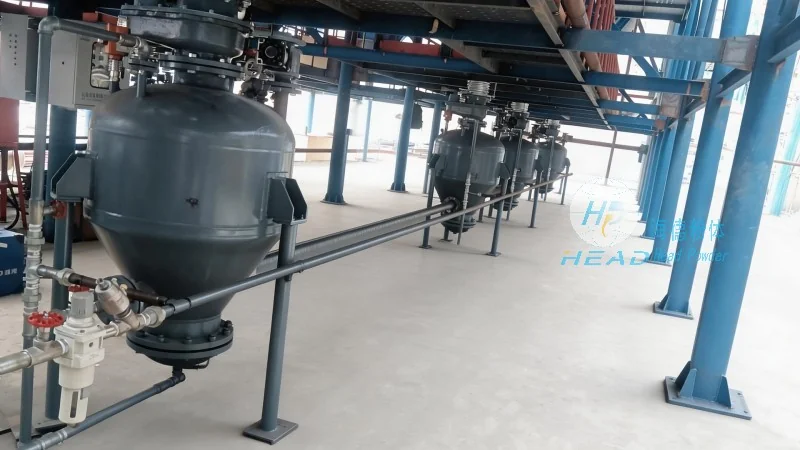
Micro-powder pneumatic conveying systems can be broadly categorized based on the pressure differential between the conveying line and the ambient environment, the phase of the conveying medium (air or gas), and the method of material transport. The primary classifications include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems operate by blowing air or gas into the conveying line, propelling the powder forward. Negative pressure systems, conversely, draw air and powder into the system using suction, creating a vacuum. Hybrid systems combine elements of both approaches, often using a combination of pressure and suction to optimize performance for specific material properties.
Within these broad categories, further sub-classifications exist based on the phase of the conveying medium. For instance, systems can be categorized as dilute-phase or dense-phase. Dilute-phase systems rely on high-velocity air to suspend the powder particles, typically operating at velocities above 20 m/s. Dense-phase systems, on the other hand, use lower velocities and higher gas-to-solid ratios to create a more compact flow, often employing pulse or rotary valves to control the material discharge. The choice between dilute and dense-phase systems depends on factors such as the material's dustiness, particle size distribution, and the required conveying distance.
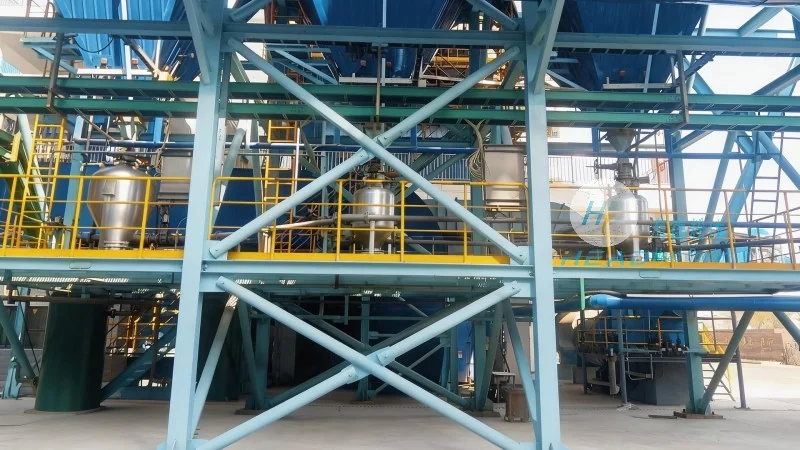
The application of micropowder pneumatic conveying systems spans multiple industries, each with distinct requirements for material handling. In the chemical industry, these systems are widely used for transporting fine powders such as pigments, catalysts, and specialty chemicals. The ability to maintain product purity and prevent contamination is paramount, making systems with advanced filtration and sealing capabilities essential. For example, in the production of pharmaceuticals, where product safety and consistency are critical, micropowder conveying systems are employed to transfer active pharmaceutical ingredients (APIs) and excipients with minimal risk of cross-contamination.
In the food and beverage sector, micropowder conveying systems are utilized for handling ingredients like cocoa powder, sugar, and flavorings. The systems must comply with stringent hygiene standards and be designed to prevent product degradation due to moisture or temperature variations. Many food processing facilities opt for positive pressure systems with stainless steel construction and integrated cleaning mechanisms to ensure compliance with regulatory requirements. The efficiency of these systems in maintaining product quality is a key factor in their adoption across the industry.
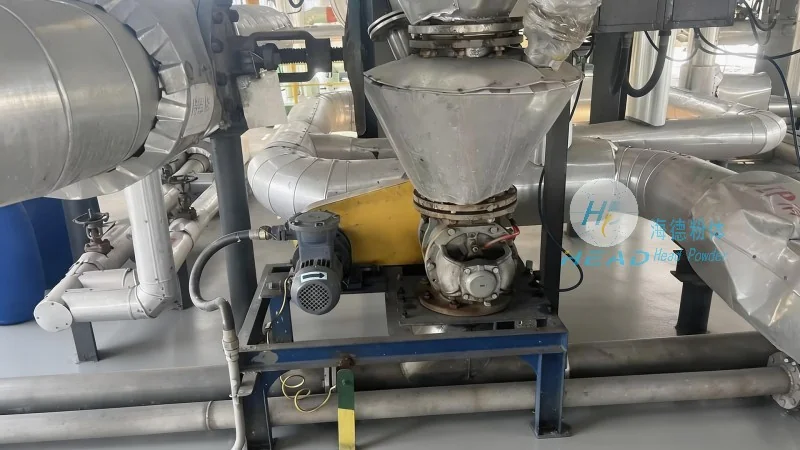
The manufacturing of ceramics and glass also relies on micropowder pneumatic conveying for transporting raw materials such as clay, silica, and feldspar. These materials often have high abrasiveness and require systems with robust components, including wear-resistant pipelines and specialized valves. The ability to handle abrasive powders without excessive wear and tear is a critical consideration in system design. Additionally, the need to maintain a consistent particle size distribution during transport is essential for achieving uniform product quality in the final ceramic or glass products.
When designing and implementing micropowder pneumatic conveying systems, several factors must be carefully evaluated to ensure optimal performance and longevity. Material selection is a primary consideration, as the conveying system must be compatible with the specific powder being handled. For example, systems handling corrosive chemicals may require materials such as stainless steel or PTFE-coated components to prevent degradation. Similarly, abrasive powders may necessitate the use of wear-resistant alloys or lined pipelines to extend the system's operational life.
System configuration and layout also play a crucial role in efficiency. The design of the conveying line, including the placement of bends, expansions, and contractions, directly impacts the pressure drop and energy consumption of the system. Properly sized and positioned pulse or rotary valves are essential for controlling the flow of powder and preventing blockages. Additionally, the integration of dust collection and filtration systems is critical for maintaining air quality and complying with environmental regulations. The effectiveness of these systems in capturing fine particles and preventing emissions is a key performance indicator.
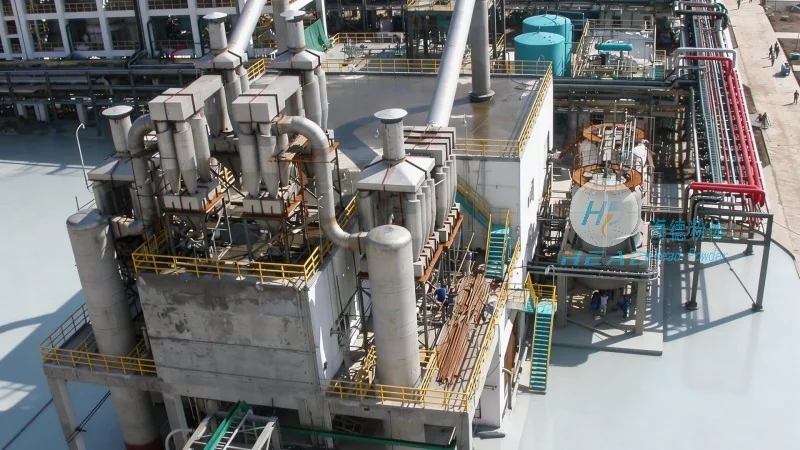
Operational parameters, such as air velocity and pressure, must be optimized based on the material's physical properties. For example, fine powders with high dustiness may require higher air velocities to maintain suspension, while cohesive powders may need additional energy input or specialized feeding mechanisms to ensure smooth transport. The use of in-line sensors and monitoring systems can help optimize these parameters in real-time, improving system efficiency and reducing energy consumption.
Micropowder pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of fine powders across various industrial applications. The classification of these systems, based on pressure differential, phase, and flow characteristics, provides a framework for selecting the most appropriate technology for specific material and operational requirements. The application analysis highlights the diverse industries that benefit from these systems, including chemicals, pharmaceuticals, food, and ceramics, where product quality, safety, and efficiency are paramount. By carefully considering material compatibility, system design, and operational parameters, industries can leverage micropowder conveying systems to enhance productivity and maintain competitive advantages. As technology advances, continued innovation in system design and material handling will further optimize the performance of these critical industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top