HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed for efficient transport of limestone powder and similar fine particulate materials. Based in Shandong, China, the company has established itself as a trusted partner in the field of bulk material handling, delivering reliable equipment that meets the demanding requirements of various industrial applications.
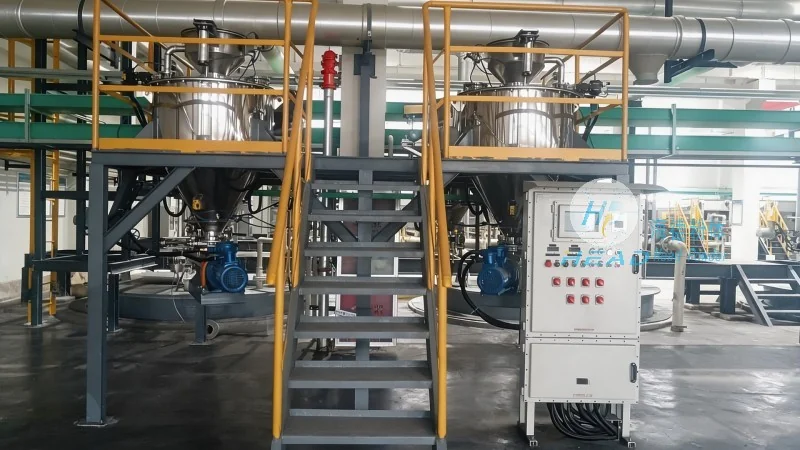
Limestone powder, a widely used raw material in industries such as cement production, chemical manufacturing, and environmental remediation, often requires safe and efficient transportation from storage silos to processing units. Pneumatic conveying equipment offers a solution that eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and enhancing operational safety. The system utilizes compressed air or vacuum to move the powder through a network of pipes, ensuring minimal product degradation and contamination.
The pneumatic conveying system for limestone powder typically consists of several critical components that work in tandem to ensure smooth operation. These include the material hopper or silo for storage, a feeder mechanism to control the flow rate, a compressor or vacuum pump to generate the necessary air pressure, a conveying line (often made of stainless steel or other corrosion-resistant materials to handle the abrasive nature of limestone powder), and a separation or collection unit at the destination point. Each component plays a vital role in maintaining the integrity of the limestone powder and the efficiency of the conveying process.
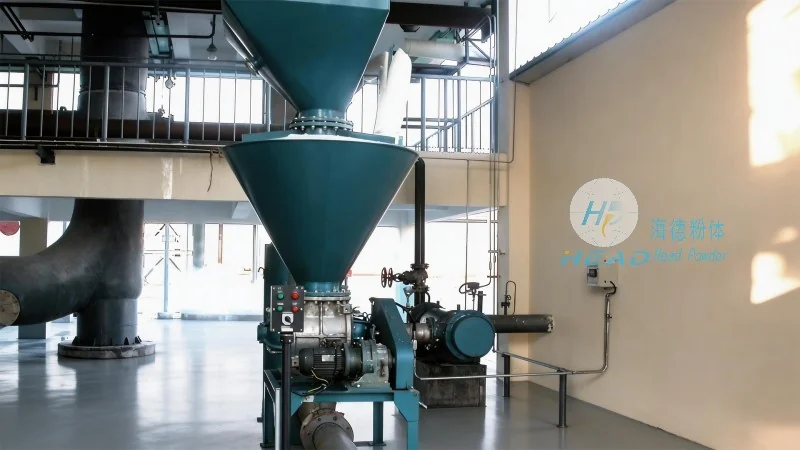
The operation of the limestone powder pneumatic conveying equipment begins with the loading of the material into the storage hopper. The feeder, which can be a rotary valve or a screw feeder, regulates the flow of limestone powder into the conveying line. Simultaneously, the compressor starts and generates compressed air, which is then introduced into the conveying line at a controlled pressure. The compressed air creates a flow that entrains the limestone powder particles, forming a dense gas-solid mixture. This mixture travels through the pipeline to the receiving hopper or processing unit. At the destination, a separator (such as a cyclone or a bag filter) separates the powder from the air, allowing the limestone powder to be collected while the air is either vented or recirculated back to the system. The entire process is automated, with sensors and control systems monitoring pressure, flow rate, and material level to ensure optimal performance and prevent system failures.
The working principle of the limestone powder pneumatic conveying system is based on the physics of fluid dynamics and particle transport. In a positive pressure system, compressed air is forced through the conveying line, creating a pressure differential that propels the limestone powder forward. The air velocity must be sufficient to overcome the gravitational forces and the friction between the particles and the pipe walls, ensuring that the powder remains suspended and transported efficiently. In a negative pressure (or vacuum) system, a vacuum pump creates a low-pressure environment that draws the limestone powder and air mixture into the system. Both systems rely on the concept of "fluidization," where the air flow creates a fluid-like environment for the powder particles, allowing them to move freely through the pipeline. The choice between positive and negative pressure depends on factors such as the distance to be covered, the material's properties, and the system's design constraints. The system's efficiency is determined by the air-to-material ratio, which must be optimized to minimize energy consumption while maintaining the required conveying capacity.
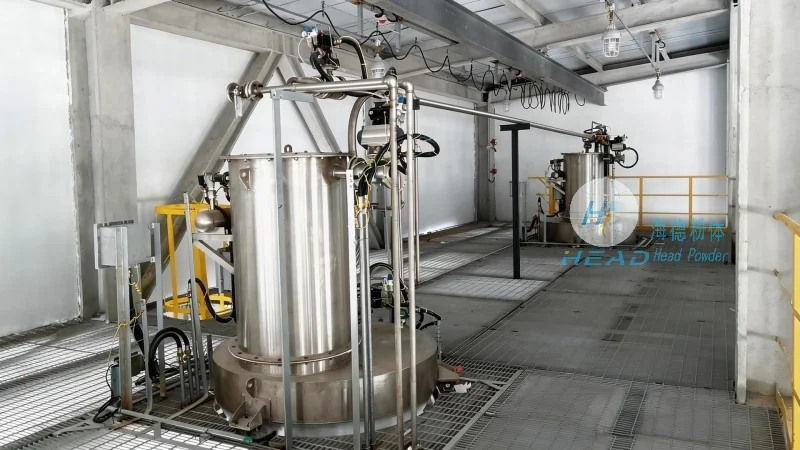
Implementing pneumatic conveying equipment for limestone powder offers several advantages over traditional mechanical conveying methods. Firstly, it eliminates the risk of product contamination, as the material is never in direct contact with mechanical components. This is particularly important for limestone powder used in food or pharmaceutical applications, where purity is critical. Secondly, the system reduces maintenance costs by eliminating moving parts like belts, chains, or buckets that are prone to wear and tear. Thirdly, pneumatic conveying systems are highly flexible, allowing for changes in the conveying route or capacity without major modifications. Additionally, the system can handle a wide range of particle sizes and moisture contents, making it suitable for various limestone powder applications. Finally, the equipment is designed for easy integration into existing industrial processes, ensuring a smooth transition and minimal disruption to production.
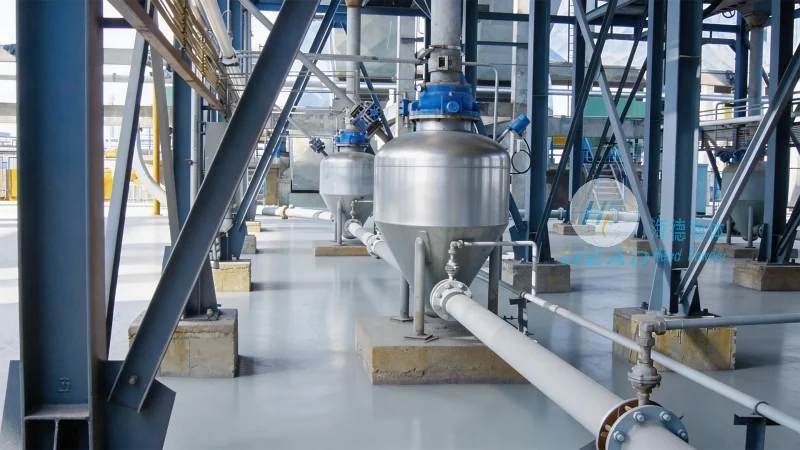
Limestone powder pneumatic conveying equipment is widely used in industries that rely on bulk material handling. In the cement industry, for example, limestone is a primary raw material, and pneumatic conveying systems are used to transport it from storage silos to the cement kilns. The efficiency of these systems directly impacts the production capacity and cost-effectiveness of cement manufacturing. In the chemical industry, limestone powder is used as a filler or reactant in various processes, and pneumatic conveying ensures that the material is delivered to reactors without any loss or contamination. Environmental remediation projects also benefit from these systems, as they allow for the safe and efficient transport of limestone powder used in soil stabilization or water treatment applications. The consistent and reliable performance of HeadPowder's pneumatic conveying equipment has contributed to improved operational efficiency and reduced downtime in these industries.
HeadPowder's limestone powder pneumatic conveying equipment represents a cutting-edge solution for the efficient and safe handling of fine particulate materials. By combining advanced engineering with robust design, the company has developed systems that meet the highest standards of performance and reliability. As industries continue to demand more efficient material handling solutions, the importance of pneumatic conveying systems will only grow. Future developments may include the integration of smart sensors and IoT technology to enhance real-time monitoring and predictive maintenance, further improving the system's efficiency and longevity. However, the core principles of operation and working principle will remain consistent, ensuring that HeadPowder's equipment continues to deliver exceptional performance for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top