HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for stone aggregate applications. These systems are engineered to efficiently transport bulk materials like crushed stone, gravel, and other construction aggregates over long distances with minimal maintenance and operational costs. The following sections detail the operation process and working principles of such systems, providing a comprehensive understanding of their functionality and benefits.
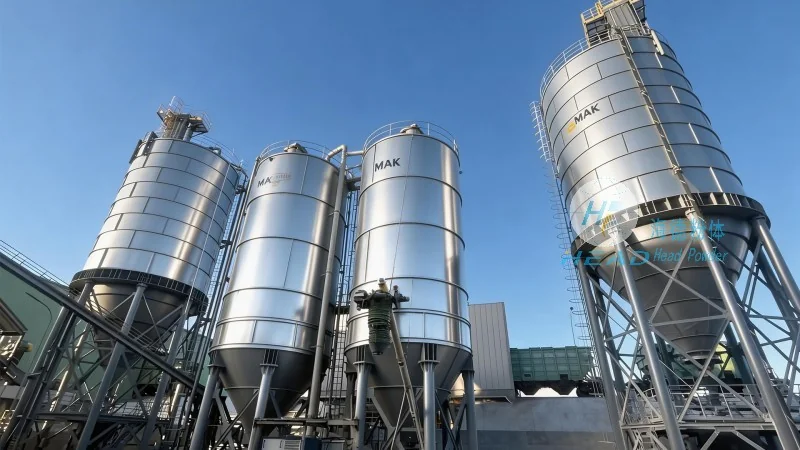
The pneumatic conveying line for stone aggregate typically consists of several critical components that work in unison to ensure smooth material transport. These components include the material hopper, feed mechanism, conveying pipe, air compressor or vacuum system, and a separation or discharge unit. Each component plays a vital role in the overall system performance. The material hopper is designed to store the stone aggregate and provide a controlled feed to the system. The feed mechanism, often a rotary valve or screw feeder, regulates the flow of material into the conveying pipe. The conveying pipe, usually made of stainless steel or other corrosion-resistant materials, is the main channel through which the material and air travel. The air compressor or vacuum system generates the necessary pressure or suction to move the material through the pipe. Finally, the separation or discharge unit collects the material at the end of the line and prepares it for further processing or use.
The operation process of a stone aggregate pneumatic conveying line begins with the loading of the material into the hopper. Once the hopper is filled, the feed mechanism starts to introduce the stone aggregate into the conveying pipe. Simultaneously, the air compressor or vacuum system activates, generating the required airflow. In a positive pressure system, the compressor pushes air into the pipe, creating a pressure differential that propels the material forward. The material is then carried along the pipe by the air stream, with the air velocity maintained at a level sufficient to keep the particles suspended and prevent blockages. As the material travels through the pipe, it reaches the end of the line where the separation unit is located. The separation unit, which may include a cyclone separator or a rotary valve, separates the material from the air. The separated material is then discharged into a collection bin or storage area, while the air is either filtered and recirculated or released to the atmosphere. The entire process is automated and can be controlled remotely, ensuring consistent and reliable material transport.
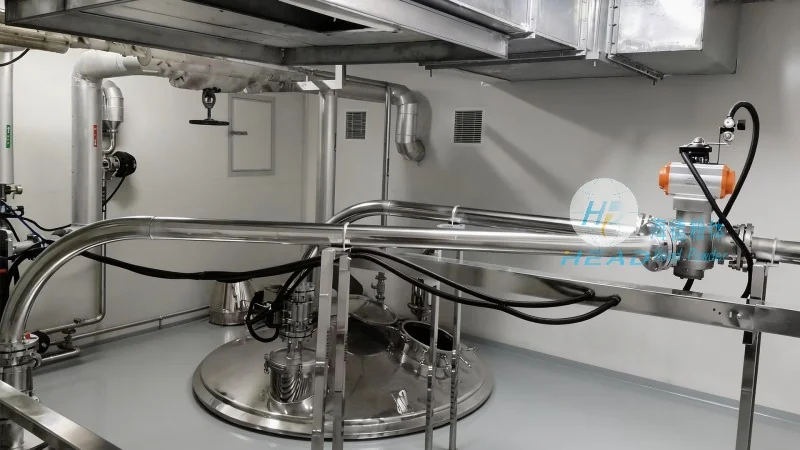
The working principle of a stone aggregate pneumatic conveying line is based on the fundamental physics of fluid dynamics and particle transport. The system operates by creating a flow of air through the conveying pipe, which interacts with the stone aggregate particles to move them from the inlet to the outlet. In a positive pressure system, the air compressor supplies high-pressure air that enters the pipe at the feed point. The air velocity is maintained above the minimum fluidization velocity of the stone particles, ensuring that the particles remain suspended in the air stream. The pressure drop along the pipe is managed by the system design, with appropriate pipe diameters and bends to minimize energy loss. In a negative pressure system, a vacuum pump creates a low-pressure environment at the discharge end, drawing the material and air through the pipe towards the inlet. The separation unit at the discharge end uses centrifugal force or other mechanisms to separate the material from the air, allowing the material to be collected while the air is filtered and recirculated. The choice between positive and negative pressure systems depends on factors such as the distance to be covered, the material characteristics, and the system layout. Both systems are effective for stone aggregate transport, with positive pressure systems often preferred for longer distances due to their higher efficiency and lower energy consumption.
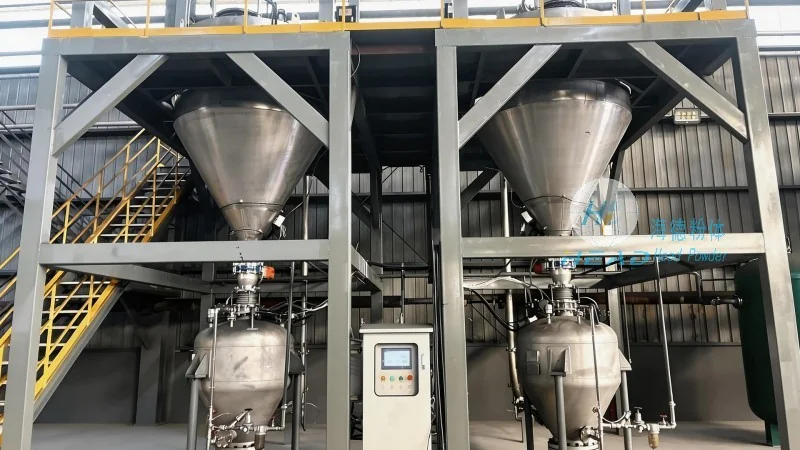
Implementing a pneumatic conveying line for stone aggregate offers several advantages over traditional methods like belt conveyors or bucket elevators. Firstly, the system is highly efficient in terms of energy consumption, as it minimizes material handling and reduces the need for multiple transfer points. This leads to lower operational costs and increased productivity. Secondly, pneumatic conveying systems are more flexible in terms of layout, allowing for vertical and horizontal transport in a single line, which simplifies the overall system design and reduces installation costs. Thirdly, the system is less prone to material degradation or contamination, as the material is enclosed within the pipe, protecting it from environmental factors and preventing dust emissions. Additionally, the system is compact and can be installed in confined spaces, making it suitable for various industrial applications. Finally, the automated operation of the system reduces labor requirements and enhances safety by minimizing human interaction with the material handling process.
To ensure the reliable and long-term operation of a stone aggregate pneumatic conveying line, proper maintenance and operational considerations are essential. Regular inspection of the system components, such as the hopper, feed mechanism, and conveying pipe, is necessary to detect any signs of wear or damage. The air compressor or vacuum system should be checked for proper performance, including pressure and airflow rates, to maintain optimal operation. The separation unit should be cleaned regularly to prevent clogging and ensure efficient material separation. Additionally, the system should be equipped with monitoring devices to track key parameters like pressure, temperature, and flow rate, allowing for early detection of any issues. Proper training of operators on the system's operation and maintenance procedures is also crucial to prevent accidents and ensure the system's longevity. By following these guidelines, users can maximize the performance and lifespan of their pneumatic conveying line, ensuring consistent and reliable material transport for their stone aggregate applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top