Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for handling rare earth materials. These systems are engineered to efficiently transport bulk materials like rare earth oxides, concentrates, and other powders over long distances with minimal loss and high reliability. The following sections detail the operational process and working principles of such systems, highlighting key components and their functions.
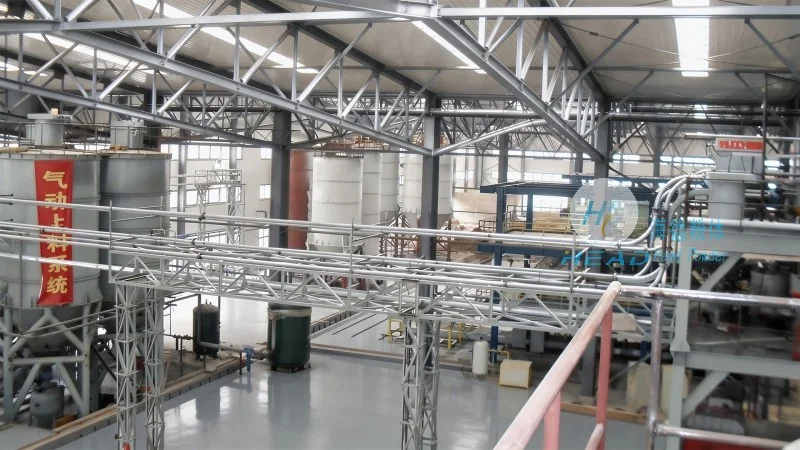
The core components of a rare earth material pneumatic conveying line typically include a material hopper, feeder, air compressor, conveying pipe, and a receiver or discharge unit. Each component plays a critical role in ensuring smooth material flow and system efficiency. The material hopper stores the rare earth powder, while the feeder controls the discharge rate to maintain consistent flow. The air compressor generates the necessary air pressure to move the material through the pipeline. The conveying pipe, often made of corrosion-resistant materials such as stainless steel or special alloys, transports the material and air mixture. Finally, the receiver collects the conveyed material and may include a dust collection system to ensure environmental compliance.
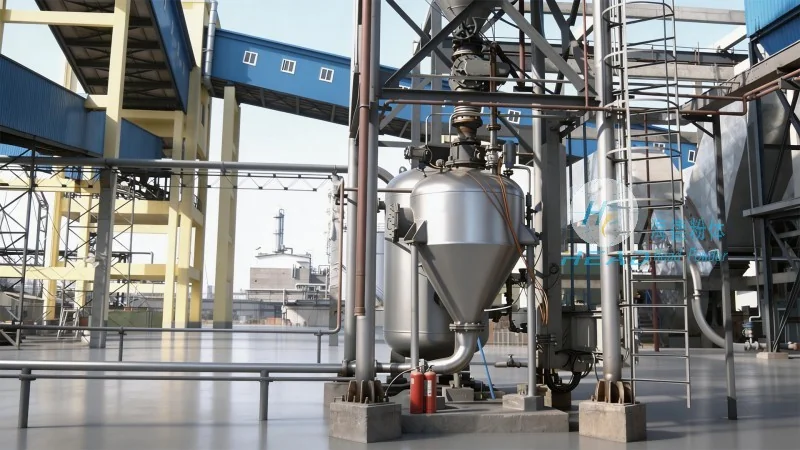
The working principle of a pneumatic conveying system involves creating a pressure differential between the material hopper and the receiver. By injecting compressed air into the hopper, the material is lifted and carried through the pipeline as a suspension. The air flow velocity is carefully controlled to prevent material deposition or blockage in the pipe. The system operates in either positive pressure (pressure conveying) or negative pressure (vacuum conveying) modes, depending on the application requirements. Positive pressure systems are commonly used for long-distance or high-capacity transport, while negative pressure systems are suitable for short distances or where dust control is a priority.
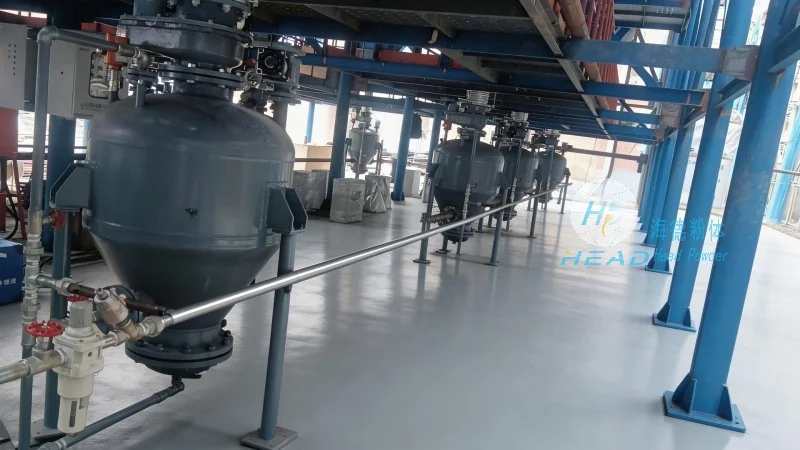
The operation process of a rare earth material pneumatic conveying line begins with material loading into the hopper. The feeder then regulates the flow rate, ensuring a steady supply of material to the conveying line. Simultaneously, the air compressor starts, generating compressed air that is introduced into the hopper. As the air pressure increases, the material is lifted and mixed with the air, forming a slurry that travels through the pipeline. The conveying pipe may include bends, valves, and expansion joints to accommodate changes in direction and elevation. At the receiving end, the material is deposited into the receiver, and the air is either vented or recirculated back to the system. The entire process is monitored by sensors and control systems to maintain optimal pressure, flow rate, and material level, ensuring consistent performance and minimizing downtime.
Using pneumatic conveying for rare earth materials offers several advantages over traditional methods like belt conveyors or bucket elevators. These systems provide a closed environment, reducing dust emissions and improving workplace safety. They also allow for flexible routing, enabling material transport around obstacles or over uneven terrain. Additionally, pneumatic conveying systems can handle fine powders and prevent material degradation due to minimal contact with equipment surfaces. The ability to control flow rates and pressure ensures precise material delivery, which is crucial for processing rare earth elements with high purity requirements. Furthermore, the system's compact design and low maintenance requirements make it suitable for various industrial applications, from small-scale processing to large-scale production facilities.
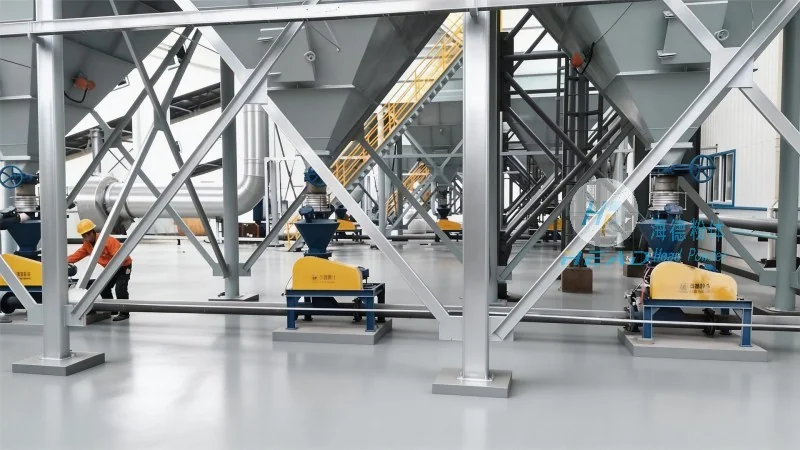
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented rare earth material pneumatic conveying lines in multiple industrial settings. For instance, in a rare earth oxide production plant, the system efficiently transports raw concentrates from storage silos to the processing reactors. The closed-loop design prevents contamination and ensures that the material remains in a controlled environment throughout the transport process. Another application involves the conveyance of rare earth metal powders from a sintering furnace to a packaging unit, where the system's high-temperature resistance and corrosion resistance are critical. These examples demonstrate the versatility and reliability of pneumatic conveying systems in the rare earth industry, supporting efficient production and compliance with environmental regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top