HeadPowder, a leading provider of industrial conveying solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for handling crystalline materials. This article delves into the operational process and underlying working principles of such equipment, offering insights into how these systems efficiently transport bulk materials while maintaining product integrity.
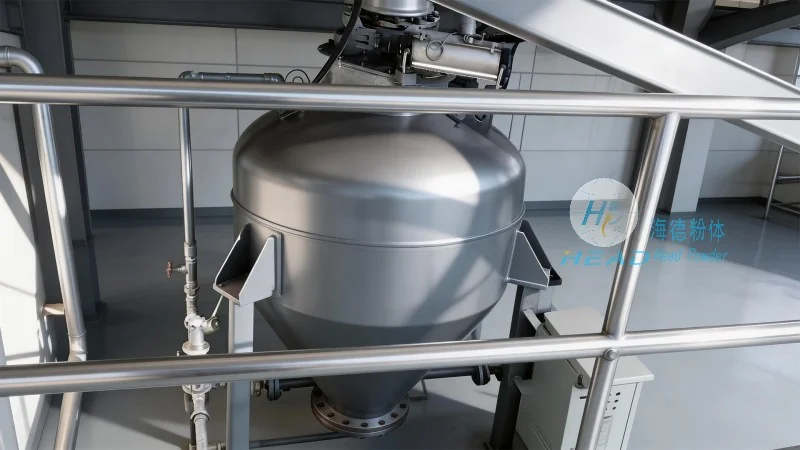
At the core of HeadPowder's offerings is a range of pneumatic conveying equipment engineered to handle crystalline materials, which often present unique challenges due to their size, shape, and tendency to agglomerate. These systems utilize air or gas as the primary transport medium, enabling the movement of materials from a source to a destination without the need for mechanical components like belts or buckets. The design of these systems is critical to ensure efficient, reliable, and safe operation, particularly when dealing with materials that are sensitive to moisture, temperature, or mechanical stress.
The pneumatic conveying equipment for crystalline materials typically consists of several key components, each playing a vital role in the overall operation. These include the material feed hopper, which holds the crystalline material and regulates its flow into the system; the air supply unit, which generates the necessary pressure or vacuum to move the material; the conveying line, which transports the material through the system; and the discharge unit, which delivers the material to its final destination. Additionally, components such as filters, cyclones, and pressure vessels are integrated to manage air quality, separate material from air, and store excess air or material, respectively.
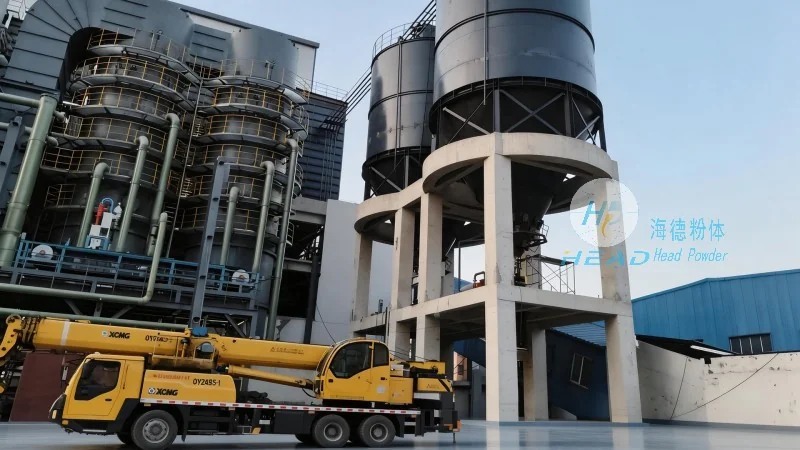
The operation of the pneumatic conveying system for crystalline materials follows a systematic sequence, ensuring smooth and continuous material transport. The process begins with the material being fed into the hopper from a storage silo or bulk container. A feeder mechanism, such as a rotary valve or a screw conveyor, controls the flow rate of the material into the hopper, preventing overfilling and maintaining a consistent feed. Simultaneously, the air supply unit activates, generating either positive pressure (to push the material forward) or negative pressure (to pull the material into the system). The material is then introduced into the conveying line, where it is suspended in the air stream and carried to the discharge point. The conveying line may include bends, elbows, or expansion joints to accommodate changes in direction or elevation, ensuring the material travels efficiently without blockages. Upon reaching the discharge unit, the material is separated from the air, often through a cyclone separator or a filter, and collected in a receiving bin or container. The air, now free of material particles, is either vented to the atmosphere or recirculated back into the system, depending on the design and environmental requirements.
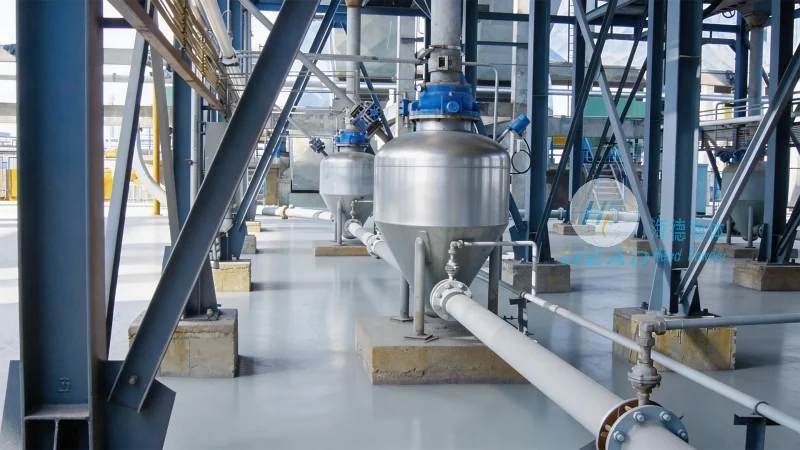
The working principle of the pneumatic conveying system relies on the fundamental physics of fluid dynamics and particle motion. In positive pressure systems, compressed air is introduced into the conveying line, creating a high-pressure environment that propels the crystalline material forward. The material particles are entrained in the air stream, and their movement is governed by the balance of forces, including the drag force exerted by the air on the particles and the gravitational force pulling them downward. The velocity of the air stream must be sufficient to overcome the gravitational force and keep the particles suspended, typically requiring air velocities ranging from 20 to 40 meters per second for fine crystalline materials. In negative pressure systems, a vacuum is created at the discharge end, drawing the material into the system and pulling it through the conveying line. The air flow in this case is directed from the material source towards the vacuum source, ensuring the material is pulled along the line without the need for external air compression.
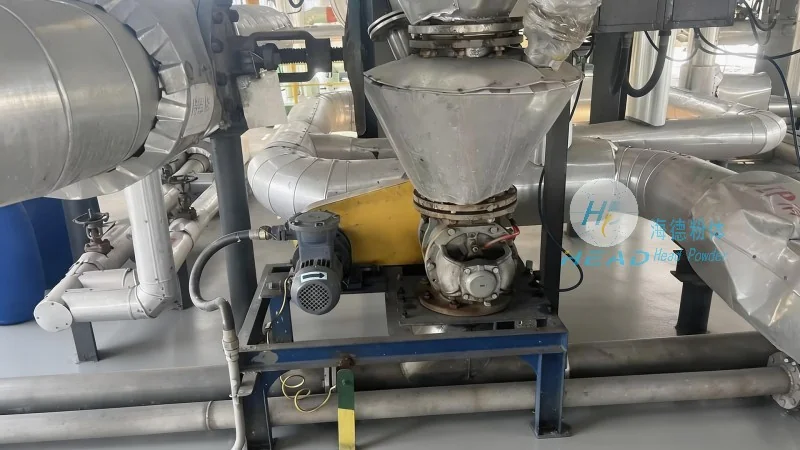
HeadPowder's pneumatic conveying equipment is designed with efficiency and product integrity as top priorities. The system's ability to maintain low temperatures and controlled humidity is crucial for preserving the quality of crystalline materials, which may degrade if exposed to high temperatures or moisture. The use of stainless steel or other corrosion-resistant materials in the construction of the hopper, conveying line, and discharge unit helps prevent contamination and ensures durability. Additionally, the integration of sensors and control systems allows for real-time monitoring of material flow rates, air pressure, and system performance, enabling operators to adjust parameters as needed to optimize efficiency and prevent system failures.
The pneumatic conveying systems developed by HeadPowder find applications in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. These systems offer several advantages over traditional mechanical conveying methods, such as reduced risk of material contamination, lower maintenance costs, and the ability to transport materials over long distances without the need for multiple transfer points. The flexibility of the system allows it to be adapted to different material types and processing requirements, making it a versatile solution for industrial material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top