HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying equipment tailored for catalyst material handling. This article provides a detailed overview of the operation process and working principles of such systems, highlighting their efficiency, reliability, and suitability for industrial applications.
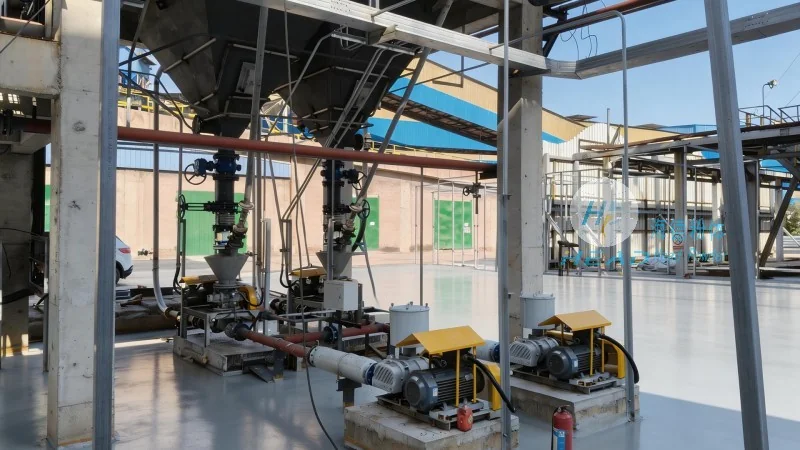
Pneumatic conveying systems utilize air or other gases to transport bulk materials like catalysts through a pipeline network. Unlike traditional mechanical conveyors, these systems offer advantages such as minimal product degradation, reduced maintenance, and the ability to handle a wide range of particle sizes and densities. The core components of a typical pneumatic conveying system include a material feed hopper, a conveyor line, a control valve, and a dust collection system. Each component plays a critical role in ensuring smooth and efficient material transport.
The operation process of a catalyst material pneumatic conveying system involves several key steps. First, the catalyst material is stored in a hopper, which is equipped with a feeding mechanism to control the flow rate. The material is then fed into the conveyor line under controlled conditions. Next, a fan or blower generates the necessary airflow, which is directed through the pipeline to create a pressure differential. This differential propels the catalyst particles along the conveyor line. The system typically includes a series of bends, elbows, and straight sections to guide the material to the destination point, such as a reactor or storage silo. At the end of the conveyor line, a control valve regulates the airflow and material discharge, ensuring precise delivery. Finally, a dust collection system captures any airborne particles, maintaining environmental compliance and product quality.
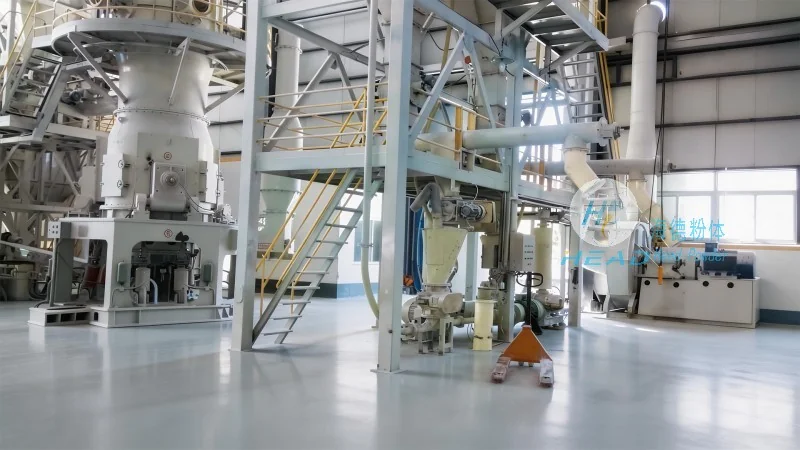
The working principle of pneumatic conveying equipment is based on the fundamental concept of fluidization and transport. When air is introduced into the conveyor line at a sufficient velocity, it creates a fluidized state where the catalyst particles are suspended and transported as a slurry. The velocity of the air must be maintained above the minimum conveying velocity, which is determined by the material's properties, such as particle size, density, and moisture content. The system operates under either positive or negative pressure, depending on the application. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use suction to pull the material. Both methods are effective, but the choice depends on factors like material characteristics, system layout, and operational requirements.
HeadPowder's pneumatic conveying systems for catalyst materials offer several key features and benefits. These include high efficiency in material transport, with minimal downtime and maintenance requirements. The systems are designed to handle abrasive and sensitive catalyst materials without causing degradation or contamination. Additionally, the enclosed pipeline design ensures a clean and dust-free environment, which is crucial for maintaining product quality and meeting environmental regulations. The flexibility of the system allows for easy integration with existing industrial processes, and the modular design enables scalability to accommodate varying production needs. Furthermore, the use of advanced control systems provides precise monitoring and adjustment of flow rates, pressure, and temperature, ensuring optimal performance and safety.
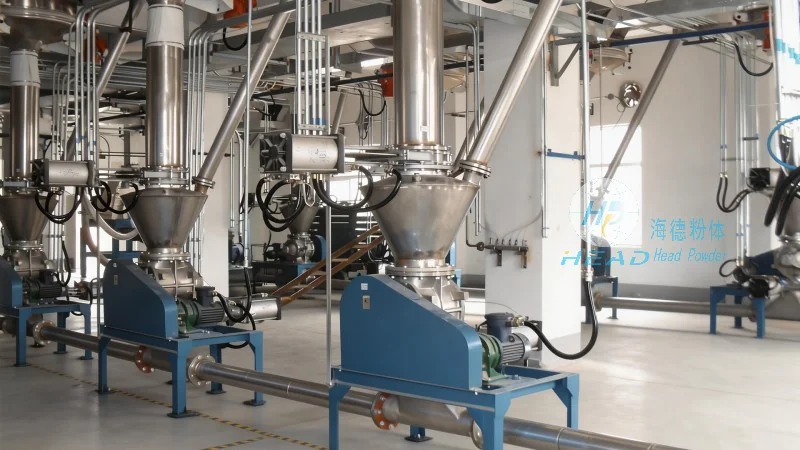
Pneumatic conveying equipment is widely used in various industrial applications involving catalyst materials. These include chemical manufacturing, petrochemical processing, pharmaceutical production, and environmental remediation. In chemical plants, the system efficiently transports catalysts to reactors, ensuring consistent and uniform mixing. In petrochemical facilities, it handles catalysts for refining processes, contributing to higher product yields and quality. Pharmaceutical manufacturers rely on these systems to transport catalysts in sterile environments, maintaining compliance with regulatory standards. Environmental remediation projects also utilize pneumatic conveying to transport catalysts used in treatment processes, enhancing the efficiency of waste management operations.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced pneumatic conveying equipment for catalyst material handling. Through meticulous design, robust construction, and rigorous testing, the company ensures that its systems meet the highest standards of performance, reliability, and safety. The operation process and working principles of these systems are optimized to deliver efficient, cost-effective, and environmentally friendly material transport solutions. By leveraging the expertise of HeadPowder, industrial facilities can enhance their production processes, improve product quality, and achieve greater operational efficiency in handling catalyst materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top