HeadPowder, a leading provider of industrial material handling solutions, specializes in air-driven equipment designed for the efficient and reliable transport of recycled sand materials. This equipment is engineered to meet the demands of modern construction and manufacturing industries, offering a sustainable alternative to traditional bulk material handling methods.
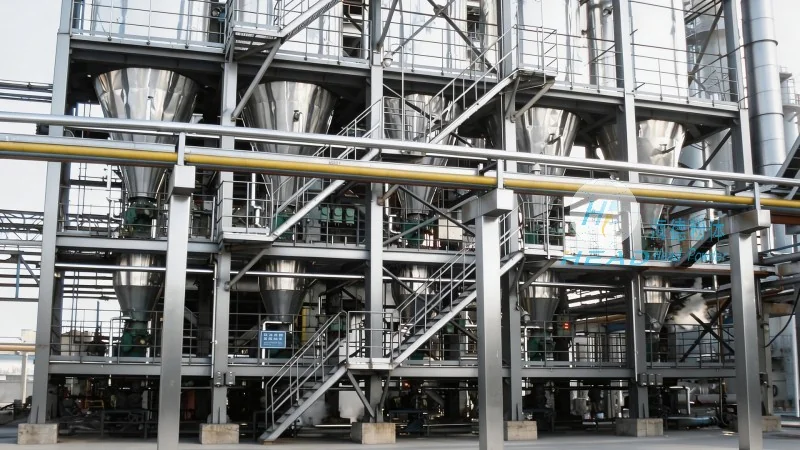
At the core of HeadPowder's air-driven equipment is a system that utilizes compressed air to move bulk materials through a network of pipes and ducts. This pneumatic conveying technology is particularly effective for transporting recycled sand, which often contains a mix of fine particles and aggregates. The system is designed to minimize material degradation, reduce dust emissions, and ensure consistent flow rates, making it ideal for applications in foundries, concrete production, and other industries that rely on recycled aggregates.
The air-driven equipment for recycled sand handling typically consists of several critical components, each playing a vital role in the overall operation. These include a material hopper for initial storage, a rotary valve or feeder to control the flow of sand into the conveying line, a series of pipeline sections with appropriate fittings and bends, and a receiver or discharge hopper at the destination point. Compressed air is supplied by an air compressor, which generates the necessary pressure to propel the sand through the system. The air and material are mixed in the pipeline, creating a slurry-like flow that allows for efficient transport over long distances.
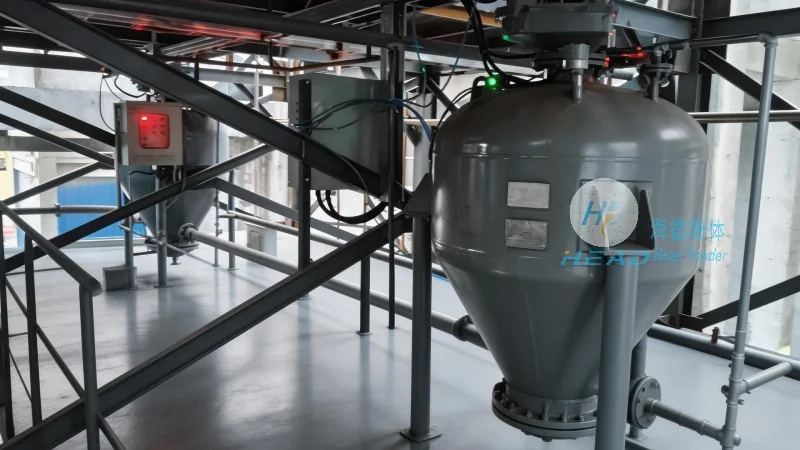
The operation of the air-driven equipment begins with the loading of recycled sand into the material hopper. The rotary valve or feeder then regulates the flow of sand, ensuring a steady and controlled feed into the conveying line. As the sand enters the pipeline, it is mixed with compressed air, which creates a pneumatic flow that propels the material forward. The pipeline system may include various components such as elbows, tees, and straight sections, each designed to maintain the flow without causing blockages or excessive pressure drops. At the receiving end, the air and sand are separated, typically using a cyclone separator or a filter, allowing the sand to be discharged into the target container or processing unit. The air is then filtered and returned to the compressor, completing the cycle.
The working principle of the air-driven equipment is based on the fundamental physics of fluid dynamics and particle transport. Compressed air provides the necessary kinetic energy to move the sand particles through the pipeline. The air velocity within the pipeline is maintained above the minimum conveying velocity required to keep the particles suspended and moving. This velocity is determined by factors such as the particle size, density, and the air pressure used. The system operates under a pressure or vacuum condition, depending on the specific application. In pressure systems, air is blown into the pipeline from the discharge end, pushing the material forward. In vacuum systems, air is drawn from the intake end, pulling the material through the line. Both methods are effective for recycled sand handling, with pressure systems often preferred for long-distance transport due to their higher efficiency and ability to handle larger particle sizes.
Implementing air-driven equipment for recycled sand handling offers several significant advantages over traditional methods. First, it provides a dust-free and clean operation, which is crucial for maintaining a safe and healthy working environment in industrial settings. The enclosed system prevents dust from being released into the air, reducing the risk of respiratory issues and improving overall workplace safety. Second, the equipment is highly efficient in terms of energy consumption and material transport. By using compressed air, the system can move large volumes of sand over long distances with minimal energy input compared to other methods like trucking or belt conveyors. Third, the system is flexible and can be easily integrated into existing production lines, allowing for seamless incorporation of recycled sand into the manufacturing process. Additionally, the equipment is low-maintenance, with fewer moving parts compared to mechanical conveyors, reducing downtime and operational costs.
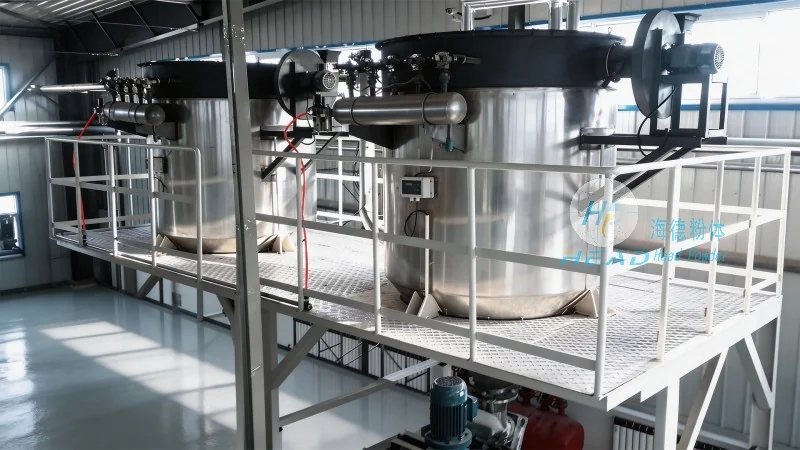
HeadPowder's air-driven equipment for recycled sand handling is widely used in various industrial applications. In foundries, the equipment is used to transport recycled sand from storage silos to molding machines, ensuring a consistent supply of material for the casting process. In concrete production plants, the system efficiently moves recycled aggregates from the stockpile to the mixing plant, contributing to the production of sustainable concrete. Other applications include the handling of recycled sand in asphalt plants, where the material is used as a filler or aggregate in road construction projects. The versatility of the equipment makes it suitable for a range of industries that require the efficient and reliable transport of bulk materials.
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to lead the way in developing advanced air-driven equipment for recycled sand material handling. By leveraging pneumatic conveying technology, the company provides solutions that enhance operational efficiency, improve workplace safety, and support sustainable practices in the construction and manufacturing sectors. The equipment's robust design, efficient operation, and low maintenance requirements make it an ideal choice for businesses looking to integrate recycled materials into their production processes while maintaining high standards of performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top