HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust-free bulk bag loading stations equipped with pneumatic conveying systems. These systems are designed to handle bulk materials efficiently and safely, ensuring minimal contamination and optimal operational performance.
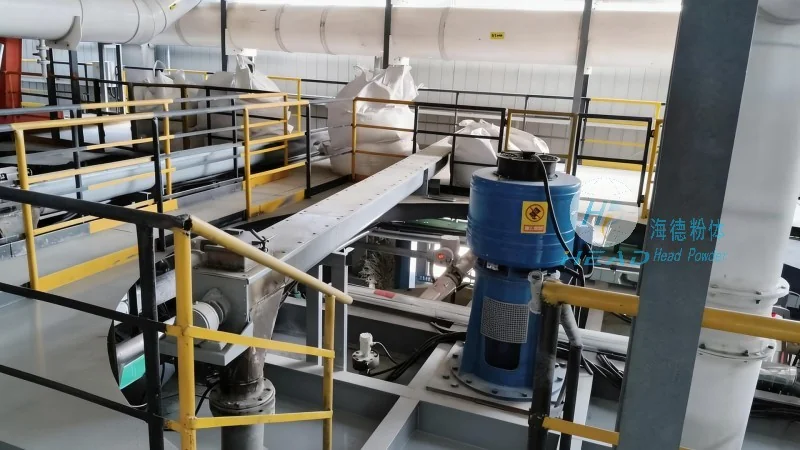
HeadPowder Engineering Co., Ltd. offers sophisticated dust-free bulk bag loading stations that integrate pneumatic conveying technology to streamline material handling processes. The primary goal of these systems is to transfer bulk materials from bulk bags (ton bags) into processing equipment or storage containers with minimal dust generation and maximum efficiency. By combining state-of-the-art engineering with robust construction, these stations are tailored to meet the demanding requirements of various industrial applications, including chemical, pharmaceutical, food, and mining sectors.
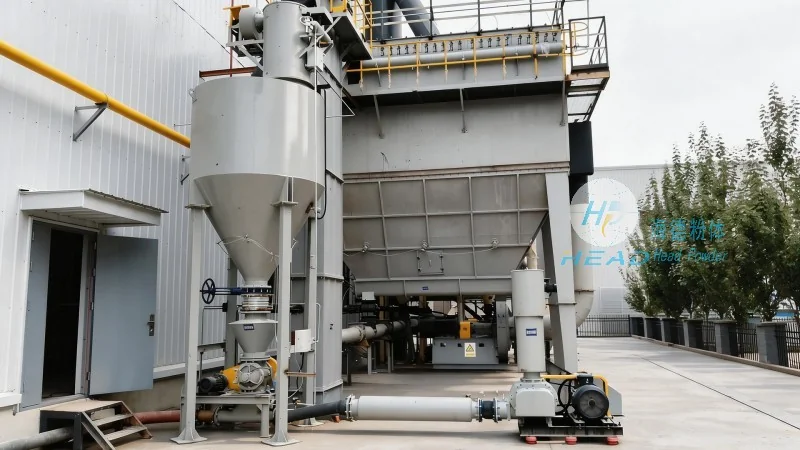
The dust-free bulk bag loading station typically consists of several critical components that work in harmony to achieve seamless material transfer. These include bulk bag hoppers, pneumatic conveying ducts, dust collection systems, and control panels. Each component is engineered to ensure durability, reliability, and compliance with industry standards. The system is designed to handle a wide range of bulk materials, from powders and granules to fine particles, with the ability to adjust conveying rates and pressures as needed. The dust collection system, often integrated with HEPA filters or other advanced filtration technologies, ensures that the working environment remains clean and safe, adhering to environmental regulations and occupational health standards.
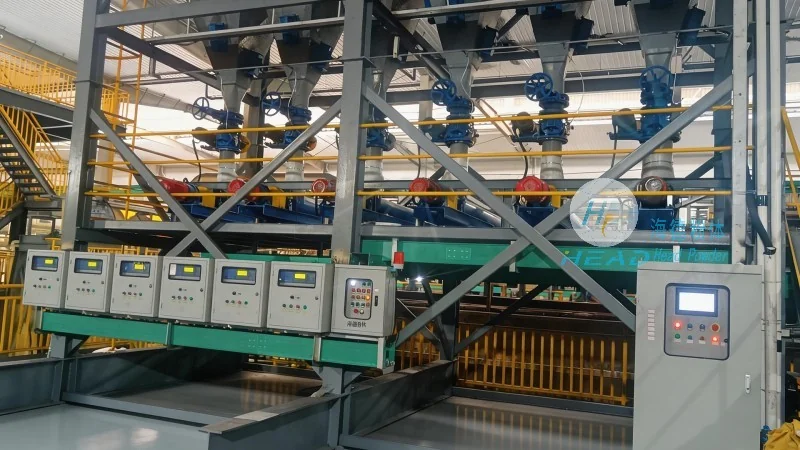
The operation of the dust-free bulk bag loading station begins with the placement of a bulk bag into the designated hopper. The bag is then sealed and positioned securely to facilitate material discharge. The pneumatic conveying system then initiates the process by creating a pressure differential between the hopper and the receiving vessel. Air is drawn through the material, lifting and transporting it through the conveying ducts to the target container. The system uses positive or negative pressure, depending on the application, to ensure efficient and controlled material flow. As the material is conveyed, the dust collection system captures any airborne particles, preventing contamination and maintaining a clean workspace. The process continues until the bulk bag is emptied, after which the system can be prepared for the next load. The entire operation is typically automated, with the control panel allowing operators to monitor and adjust parameters such as pressure, flow rate, and material level in real-time. This automation enhances efficiency and reduces the risk of human error, ensuring consistent and reliable performance.
The core of the dust-free bulk bag loading station is the pneumatic conveying technology, which relies on the movement of air to transport bulk materials. The system operates on the principle of creating a pressure difference between the source (the bulk bag hopper) and the destination (the receiving vessel). In positive pressure systems, compressed air is introduced into the hopper, forcing the material and air mixture through the conveying lines. In negative pressure systems, a vacuum is created at the receiving end, drawing the material and air mixture from the hopper. The choice between positive and negative pressure depends on factors such as material characteristics, distance, and system design. The conveying ducts are typically made of materials like stainless steel or plastic, which are resistant to corrosion and wear, ensuring long-term durability. The system may also include features like cyclone separators or rotary valves to separate the material from the air stream, allowing for clean material discharge and air recycling. The control system monitors the pressure, flow, and material level, adjusting the air flow as needed to maintain optimal conveying conditions. This closed-loop control ensures that the system operates efficiently, minimizing energy consumption and maximizing material throughput.
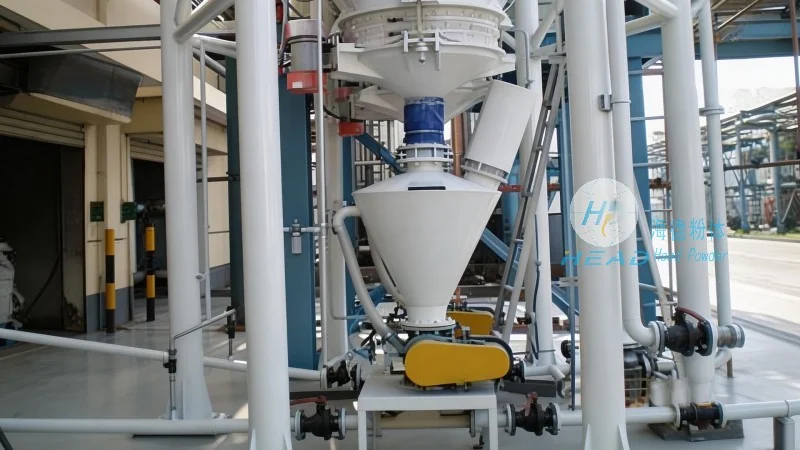
The dust-free bulk bag loading stations with pneumatic conveying systems offer numerous benefits to industrial operations. These include reduced dust exposure, improved workplace safety, and enhanced material handling efficiency. By minimizing dust generation, the systems help comply with environmental regulations and reduce the risk of respiratory issues among workers. The automated operation reduces labor costs and increases productivity, as the system can handle multiple bulk bags without constant human intervention. The flexibility of the system allows it to handle a wide variety of materials, making it suitable for diverse industrial applications. For example, in the chemical industry, these systems are used to transfer reactive powders safely and efficiently. In the food industry, they ensure that food-grade materials are handled without contamination. In mining operations, they facilitate the transport of ore and other bulk materials from storage to processing equipment. The robust design and advanced filtration systems also make these stations suitable for applications where material purity is critical, such as in pharmaceutical manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top