Limestone powder is a widely used material in various industrial applications, including construction, chemical production, and environmental remediation. The efficient and reliable transportation of limestone powder from storage to processing units is crucial for maintaining production efficiency and reducing operational costs. Pneumatic conveying systems have emerged as a preferred solution for handling fine powders like limestone due to their ability to minimize dust, improve safety, and enhance process control. This article outlines the design considerations and key components of a specialized pneumatic conveying system tailored for limestone powder particles, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
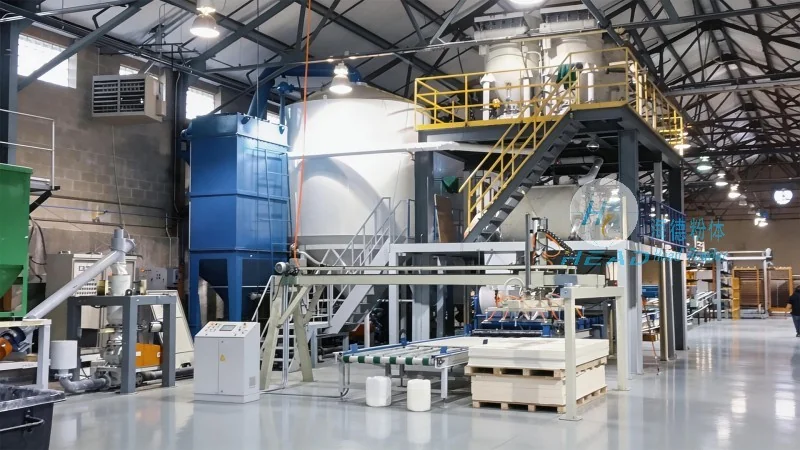
The design of a pneumatic conveying system for limestone powder particles involves several critical factors to ensure optimal performance and longevity. First, the particle size and density of limestone powder are fundamental parameters that influence the selection of conveying air velocity and system pressure. Limestone powder typically has a particle size range of 0.1 to 100 microns, with a bulk density of approximately 1.5 g/cm³. These characteristics affect the required air flow rate and the type of conveying line (e.g., dilute phase or dense phase). The system must be designed to handle the specific flow rates and pressure drops associated with limestone powder to prevent blockages and ensure consistent material transport.
Second, the system's layout and configuration are critical for minimizing energy consumption and maximizing efficiency. The design considers the distance between the storage silo and the processing unit, the number of transfer points, and the need for any intermediate storage or blending. A well-planned layout reduces the overall pressure drop across the system, leading to lower energy costs and longer equipment life. Additionally, the choice of materials for the conveying line and components is essential to prevent corrosion and wear from limestone powder, which can be abrasive and acidic in some cases. Stainless steel or corrosion-resistant alloys are commonly used for the conveying pipes and valves to ensure durability and maintain product purity.
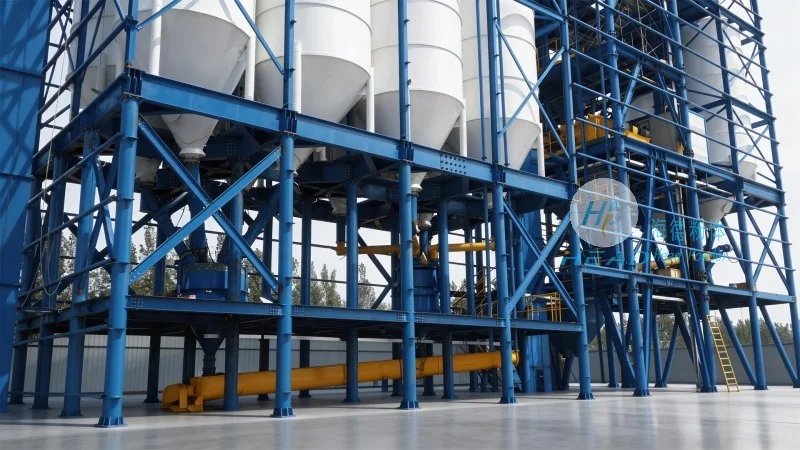
The pneumatic conveying system for limestone powder consists of several key components that work in tandem to achieve efficient material transport. The primary components include a storage silo, a rotary airlock feeder, a positive displacement blower or air compressor, a conveying line, and a receiving hopper. The storage silo is designed to hold the limestone powder and provide a consistent feed to the system. The rotary airlock feeder regulates the flow of powder from the silo to the blower, preventing backflow and maintaining a steady material feed rate. The positive displacement blower generates the necessary air pressure and flow rate to move the limestone powder particles through the conveying line. The conveying line, typically made of stainless steel, transports the powder-air mixture from the feeder to the receiving hopper. The receiving hopper collects the limestone powder and can be integrated with downstream processing equipment.
Optional components such as cyclone separators, filters, and dust collectors are included to improve system efficiency and safety. Cyclone separators use centrifugal force to separate the powder from the air, allowing the air to be recirculated or vented, while the powder is collected for further use. Filters and dust collectors are essential for maintaining air quality and complying with environmental regulations, especially in industrial settings where dust emissions must be minimized.
The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. offers several advantages over traditional mechanical conveying methods. First, it eliminates the need for moving parts in the conveying line, reducing maintenance costs and the risk of mechanical failure. Unlike screw conveyors or belt conveyors, which can experience blockages and wear from limestone powder, pneumatic systems are less prone to these issues. Second, the system provides better control over the material flow rate and pressure, allowing for precise dosing and process control. This is particularly important in applications where the limestone powder is used as a raw material in chemical reactions or as a filler in construction materials, where consistent quality is critical.
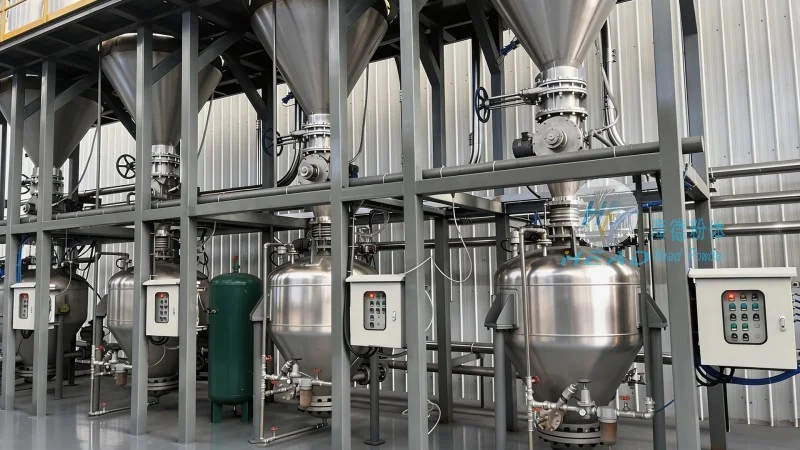
Third, the system is more hygienic and safer to operate compared to other methods. Pneumatic conveying reduces dust exposure, minimizing the risk of respiratory issues for workers and preventing dust accumulation that could lead to fires or explosions. The enclosed system design also protects the limestone powder from contamination and moisture, ensuring the material remains in optimal condition for its intended use. Additionally, the system can be easily integrated with existing production lines, reducing the need for major infrastructure changes and minimizing downtime during installation.
The pneumatic conveying system for limestone powder has been successfully implemented in various industrial applications, including cement production, lime manufacturing, and chemical processing. In cement plants, the system efficiently transports limestone powder from storage silos to grinding mills, where it is mixed with other raw materials to produce clinker. The system's ability to handle large volumes of limestone powder at high flow rates ensures that the cement production process remains uninterrupted. In lime manufacturing, the system transports limestone powder to kilns, where it is heated to produce quicklime or slaked lime. The consistent flow of limestone powder improves the quality and efficiency of the lime production process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top