HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. This article provides a detailed overview of the operation process and working principle of a stone aggregate pneumatic conveying system, highlighting the key components, operational steps, and technical aspects that ensure efficient material transport.
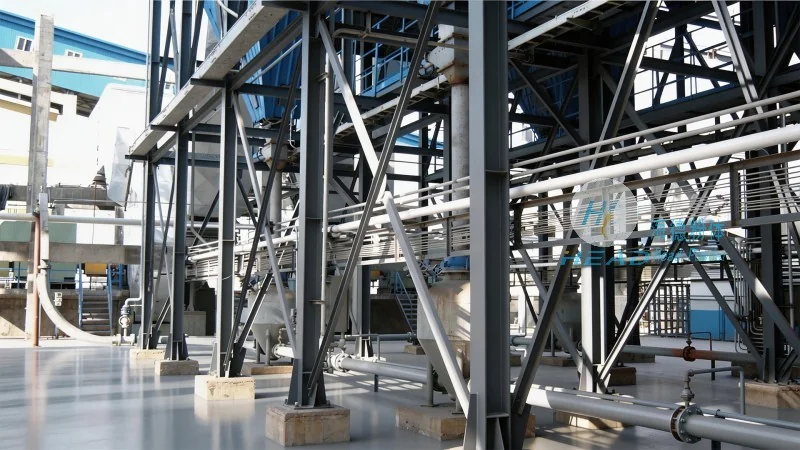
The stone aggregate pneumatic conveying system is engineered to transport bulk materials like crushed stone, gravel, or other granular aggregates from a storage silo or hopper to processing units, packaging stations, or storage facilities. The system typically consists of several critical components, including a material feeder, a conveying pipeline, a pressure vessel (or receiver), a fan or blower, and a control system. Each component plays a vital role in the seamless operation of the entire system, ensuring reliable and continuous material transport.
The operation of the stone aggregate pneumatic conveying system follows a systematic sequence of steps to achieve efficient material transfer. The process begins with the material feeder, which regulates the flow of stone aggregates from the storage silo into the conveying pipeline. The feeder may be a rotary valve, a screw feeder, or a vibratory feeder, depending on the system design and material characteristics. As the material enters the pipeline, a fan or blower generates a high-velocity air stream that propels the aggregates through the pipeline. The air stream is carefully controlled to maintain the optimal velocity and pressure required for the material to remain suspended and transported without segregation or degradation.
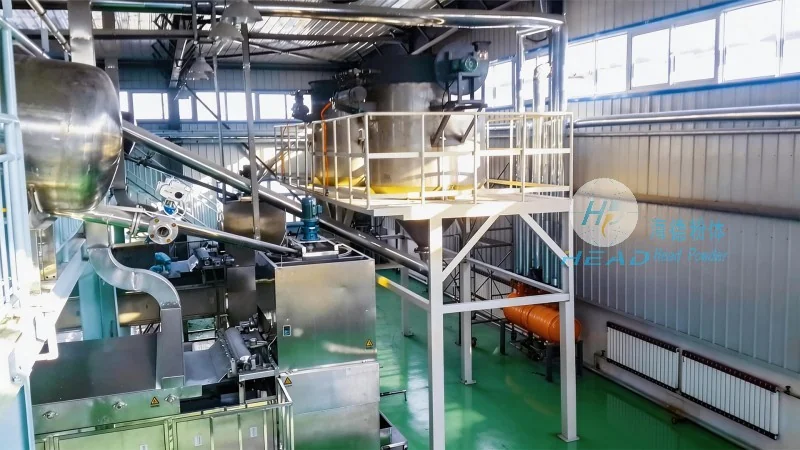
During the conveying process, the material travels through the pipeline, which may include bends, elbows, or vertical sections, all designed to minimize pressure loss and ensure smooth material flow. The pipeline is typically made of corrosion-resistant materials such as stainless steel or PVC, suitable for handling abrasive stone aggregates. At the receiving end of the system, a pressure vessel or receiver is used to separate the conveyed material from the air stream. The vessel may be equipped with a cyclone separator or a bag filter to capture the aggregates and return the air to the fan for recirculation, enhancing energy efficiency and reducing waste.
The working principle of the stone aggregate pneumatic conveying system is based on the fundamental concept of fluidization and suspension of solid particles in a gas stream. When the fan or blower creates a high-velocity air flow, the air exerts a drag force on the individual stone aggregates, lifting them off the pipeline walls and keeping them suspended in the air stream. This suspension allows the aggregates to be transported through the pipeline as a homogeneous mixture of solid and gas, eliminating the need for mechanical conveyors like belts or buckets that can cause material degradation or blockages.
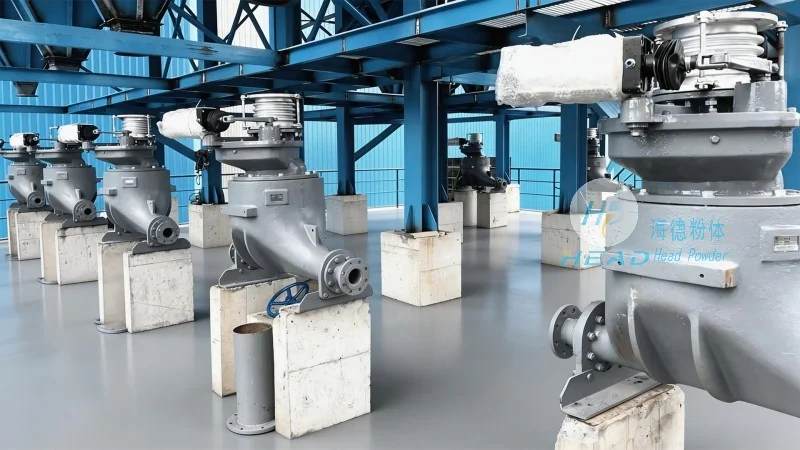
The system operates under either positive pressure or negative pressure (or a combination of both, known as a mixed system), depending on the application requirements. Positive pressure systems use the fan to force air and material through the pipeline, while negative pressure systems use a vacuum to draw material into the pipeline. The choice of pressure type depends on factors such as the distance to be covered, the height of the vertical lift, and the material characteristics. In positive pressure systems, the fan is located at the material source, and the air is blown into the pipeline, pushing the material forward. In negative pressure systems, the fan is located at the receiving end, and the vacuum pulls the material into the pipeline, drawing it from the source.
HeadPowder's stone aggregate pneumatic conveying system offers several advantages over traditional mechanical conveying methods. Firstly, it eliminates the need for moving parts in the conveying line, reducing maintenance costs and minimizing the risk of material blockages or wear. Secondly, the system provides a clean and dust-free operation, as the material is enclosed within the pipeline and separated from the environment by the air stream. This is particularly beneficial for applications where dust control is critical, such as in food processing or pharmaceutical industries. Thirdly, the system allows for flexible and scalable material transport, as the pipeline can be easily extended or modified to accommodate changes in production volume or layout. Additionally, the system operates with high efficiency, as the air stream is recirculated and reused, reducing energy consumption and operational costs.
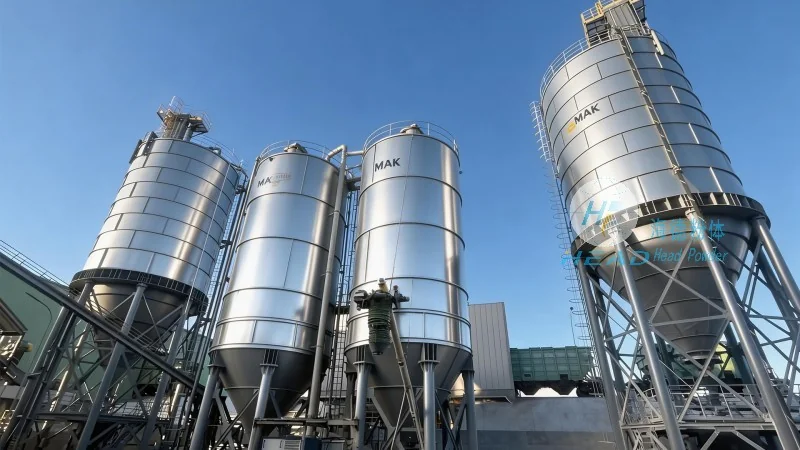
The stone aggregate pneumatic conveying system is widely used in various industries, including construction, mining, and manufacturing. In the construction industry, it is commonly used to transport crushed stone or gravel from quarries to construction sites or processing plants. In the mining industry, it is used to transport ore or rock from mining operations to processing facilities. In the manufacturing industry, it is used to transport raw materials like sand or gravel to production lines or packaging stations. The system is also used in the food and pharmaceutical industries for transporting granular materials that require strict hygiene and dust control measures.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced pneumatic conveying systems for stone aggregate applications. The company's expertise in system design, manufacturing, and installation ensures that clients receive reliable and efficient solutions tailored to their specific needs. By leveraging the operation process and working principle of the stone aggregate pneumatic conveying system, HeadPowder helps industries improve productivity, reduce costs, and enhance operational safety. For more information about HeadPowder's products and services, please visit our official website or contact our sales team.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top