Camellia seed powder conveying systems are critical components in the processing industry, particularly for facilities that handle bulk powders such as camellia seeds. These systems ensure efficient, safe, and reliable transport of the powder from one processing stage to another, minimizing material loss and optimizing production efficiency. Understanding the operation process and working principles of such equipment is essential for operators, engineers, and plant managers to maintain optimal performance and troubleshoot issues effectively.
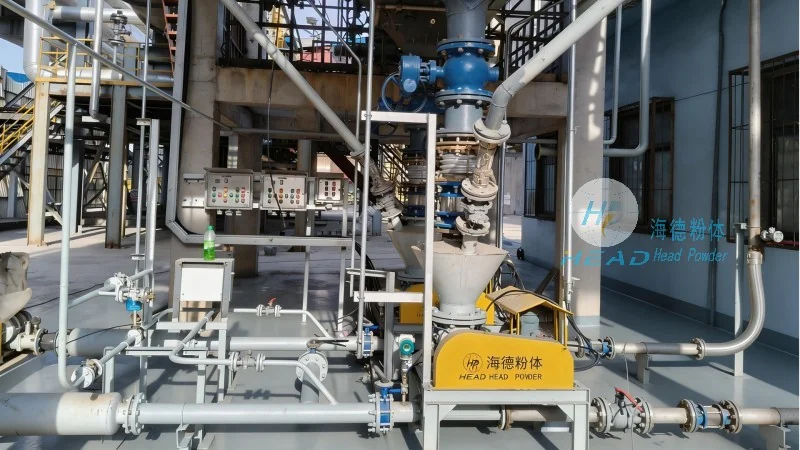
The camellia seed powder conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder), is designed to handle the unique challenges of transporting camellia seed powder. This system integrates various components, including hoppers, feeders, conveyors, and control systems, to create a seamless flow of material. The design takes into account the physical properties of camellia seed powder, such as its particle size, moisture content, and flowability, to ensure smooth operation and prevent issues like clogging or segregation.
Each component of the conveying system plays a vital role in the overall operation. The hopper serves as the storage and feeding unit, where raw camellia seeds are introduced and stored before processing. The feeder, typically a screw or vibratory type, regulates the flow of powder into the conveyor, ensuring a consistent feed rate. The conveyor itself, which may be a pneumatic or mechanical system, transports the powder through the system. Control systems monitor and adjust the operation based on real-time data, such as pressure, flow rate, and temperature, to maintain optimal conditions.
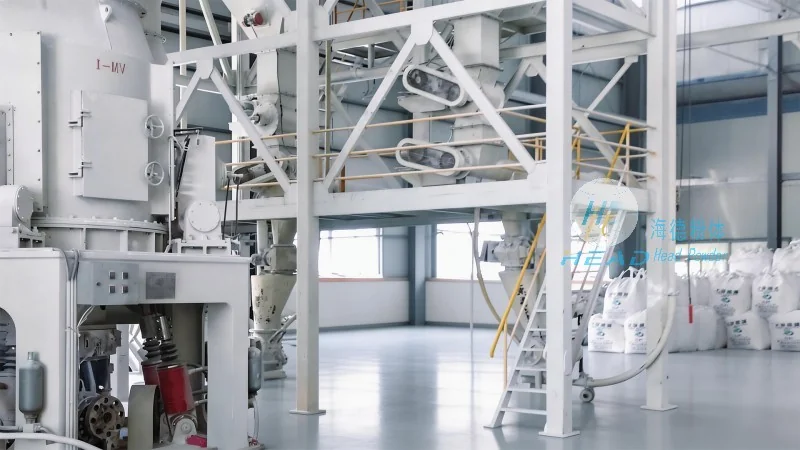
The operation of the camellia seed powder conveying system follows a systematic process. First, the raw camellia seeds are fed into the hopper. The feeder then controls the discharge rate, ensuring a steady flow into the conveyor. The conveyor transports the powder to the next processing stage, such as grinding or extraction. At each stage, sensors and controls monitor the system's performance, adjusting parameters as needed. The process continues until the powder reaches its final destination, such as a storage silo or processing unit. This step-by-step approach ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity.
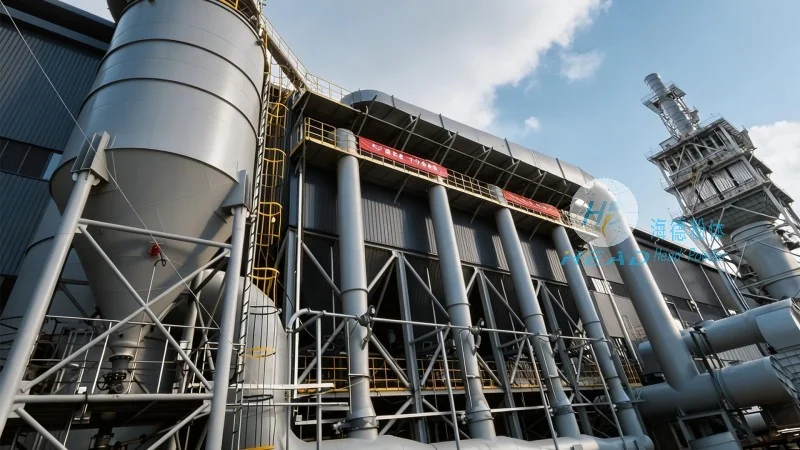
The working principle of the camellia seed powder conveying system is based on the principles of fluidization and pneumatic transport. In pneumatic conveying systems, the powder is suspended in a stream of air and transported through pipes. The air flow is controlled to maintain the powder in a fluidized state, preventing it from settling or clogging the system. Mechanical conveyors, on the other hand, use rotating components to move the powder along a path. The combination of these methods allows for efficient and reliable transport of camellia seed powder, even in challenging conditions. The system's design ensures that the powder is handled gently, preserving its quality and preventing degradation.
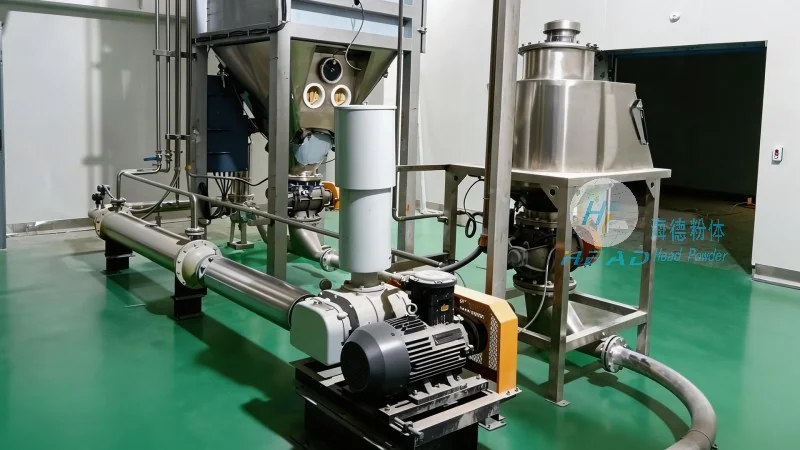
Investing in a professional camellia seed powder conveying system from headpowder offers numerous benefits. These systems are designed to handle the specific characteristics of camellia seed powder, ensuring consistent performance and minimal maintenance. The use of advanced control systems and materials reduces the risk of contamination and improves product quality. Additionally, the system's efficiency reduces energy consumption and operational costs, making it a cost-effective solution for processing facilities. The reliability of the system minimizes downtime, ensuring that production remains uninterrupted and meets customer demands.
To ensure the long-term performance of the camellia seed powder conveying system, regular maintenance is essential. This includes cleaning the hopper and feeder to prevent material buildup, checking the conveyor for wear and tear, and inspecting the control systems for proper operation. Troubleshooting common issues, such as clogging or uneven flow, involves checking the feed rate, air pressure, and material properties. By following a regular maintenance schedule and understanding the system's operation, operators can prevent major problems and extend the system's lifespan. The expertise of headpowder in designing and manufacturing these systems ensures that customers receive reliable equipment and support throughout its lifecycle.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top